FANUC Series 16i/18i/21i - MB, FANUC Series 18i - MB5 Additional Manual Page 2
Additional Manual
A-78746E
Edit
Apprv.Desig.
Sheet
Title
Draw
No.
Date
Design
Descri
p
tion
Date
FANUC Series 16i/18i/21i –MB, 18i –MB5
Tool length compensation without axis
movement Specifications
Apr.11.2002
2/3
Sheet
K.Yamamuro
02
04/02/19 All revision
H.Kouzai
1. Outline
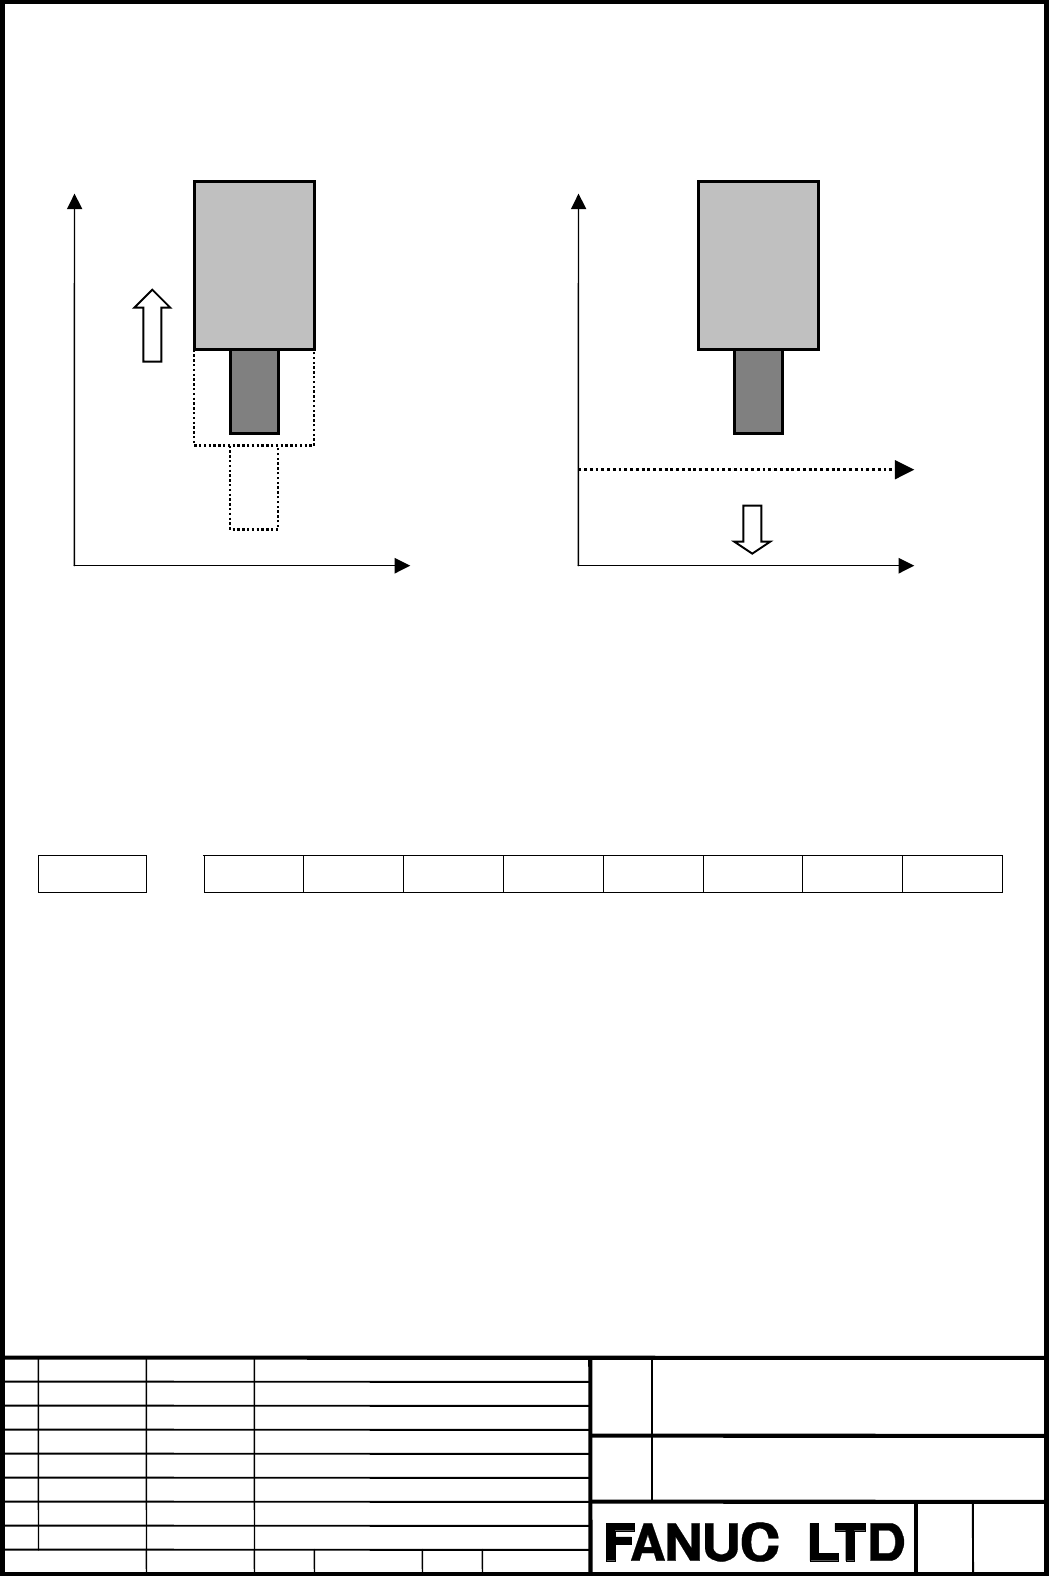
By setting parameter TOS (No.5006#6), it is possible to choose tool length compensation with axis
movement or one without axis movement.
2. Parameter
No. #7 #6 #5 #4 #3 #2 #1 #0
5006 TOS
Data type : Bit type
TOS Choose type of tool length compensation
0 : Tool length compensation with axis movement
1 : Tool length compensation without axis movement (by coordinate shift)
Tool length compensation with axis movement Tool length compensation without axis movement
(Compensation by coordinate shift)
X
X’
ZZ
X
Move
Z axis
Shift Z axis coordinate
Contents Summary of FANUC Series 16i/18i/21i - MB, FANUC Series 18i - MB5 Additional Manual
- Page 1FANUC Series 16i/18i/21i - MB FANUC Series 18i - MB5 Tool length compensation without axis movement Specifications - Contents - 1. OUTLINE ..................................................................................................................................................... 2 2. PARAME
- Page 21. Outline By setting parameter TOS (No.5006#6), it is possible to choose tool length compensation with axis movement or one without axis movement. Z Z Move Z axis X Shift Z axis coordinate X X’ Tool length compensation with axis movement Tool length compensation without axis movement (Compensation
- Page 3No. #7 #6 #5 #4 #3 #2 #1 #0 6006 MSV Data type : Bit type MSV When reading system variables with tool length compensation without axis movement, 0 : System variables #5041~#5048 (current position), #5061~#5068 (skip signal position) do not include the actual tool length compensation value. 1 : Syste