Series 0i/0i Mate - Model B Connection manual (Function) Page 616
Connection manual (Function)
B–63833EN–1/02
9. SPINDLE SPEED FUNCTION
598
This function stops the spindle at a specified position. The spindle can
be stopped in either of the following two ways.
· The spindle is stopped using mechanical stop.
· The spindle is stopped by applying a function of the spindle control
unit.
To mechanically stop the spindle by using, for example, a shot pin, rotate
the spindle at a constant low speed and drive the pin into the spindle. The
spindle can be rotated at a low constant speed by applying either of the
following methods.
· Spindle orientation signal (See 9.3, “Spindle Control.”)
· Spindle output control by the PMC (See 15.4.)
Some spindle control units can position the spindle motor by using
sensors and position coders. The CNC itself does not control positioning
by using these units.
In serial spindle orientation by a position coder, the stop position is
specified either by a parameter or by the PMC (spindle orientation
function with the stop position externally set).
[Classification] Input signal
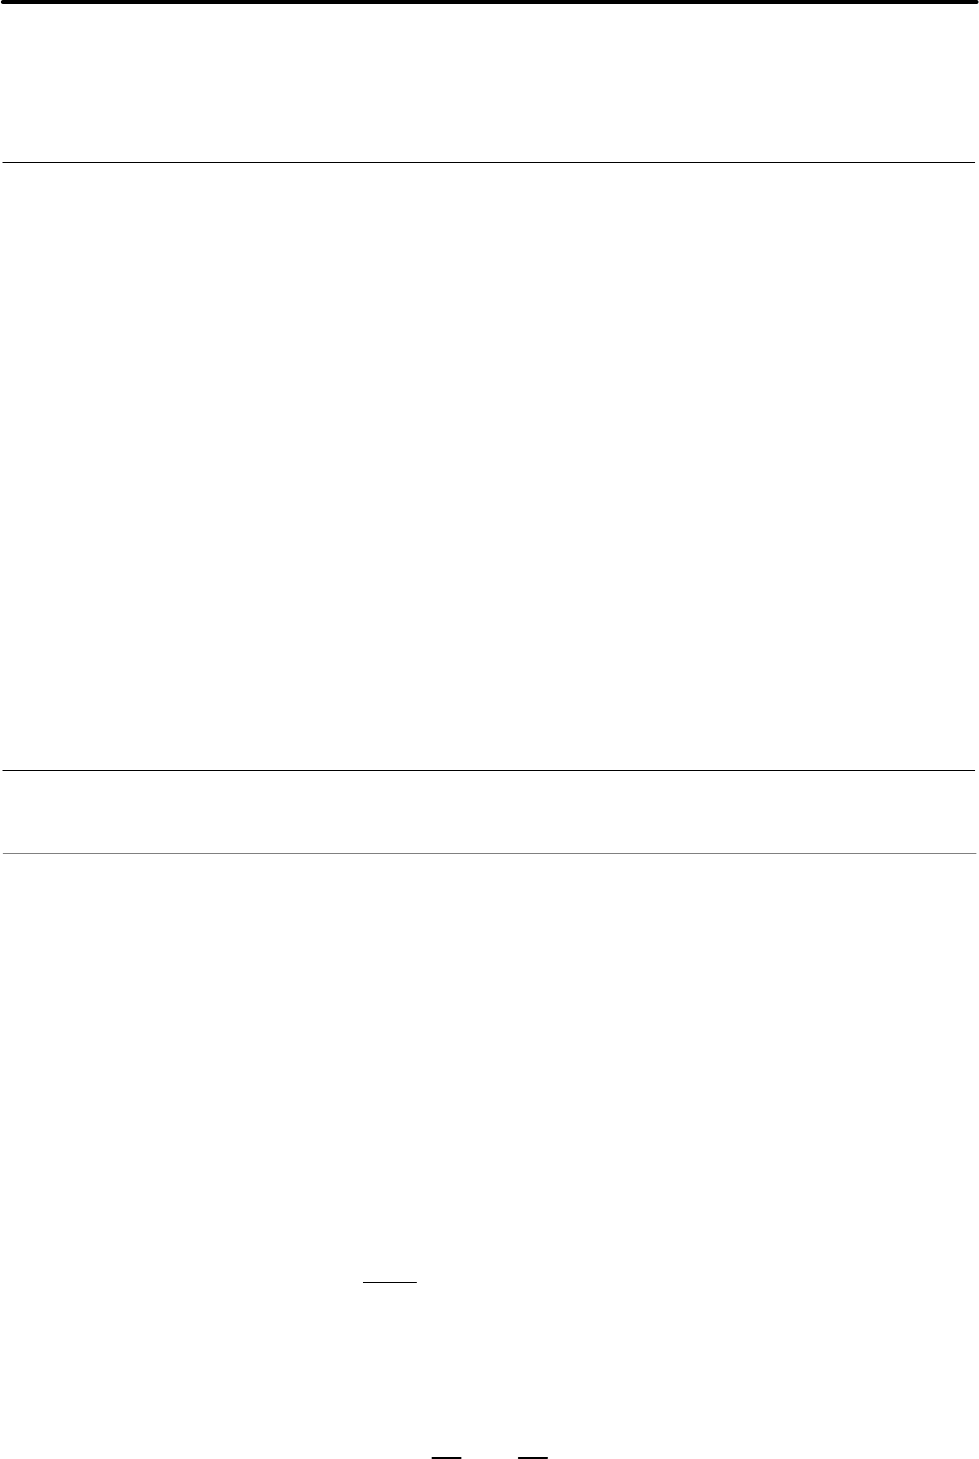
[Function] This command is used for specifying a stop position with an absolute
position within one rotation in the following equation:
=
4096
360
ȍ (2
i
Pi)
n
i=0
where
Pi = 0 when SHAi = 0
Pi = 1 when SHAi = 1
9.12
SPINDLE
ORIENTATION
General
Mechanical stop
Using the spindle
control unit
Serial spindle orientation
by a position coder
Signal
Spindle orientation
signals with the stop
position externally set
SHA00 to SHA11 for the
first spindle
<G078, G079>
SHB00 to SHB11 for the
second spindle
<G080, G081>
Contents Summary of Series 0i/0i Mate - Model B Connection manual (Function)
- Page 1FANUC Series 0 -MODEL B FANUC Series 0 Mate-MODEL B CONNECTION MANUAL (FUNCTION) (Volume 1 & 2) B-63833EN-1/02
- Page 2Ȧ No part of this manual may be reproduced in any form. Ȧ All specifications and designs are subject to change without notice. In this manual we have tried as much as possible to describe all the various matters. However, we cannot describe all the matters which must not be done, or which cannot be
- Page 3B–63833EN–1/02 DEFINITION OF WARNING, CAUTION, AND NOTE DEFINITION OF WARNING, CAUTION, AND NOTE This manual includes safety precautions for protecting the user and preventing damage to the machine. Precautions are classified into Warning and Caution according to their bearing on safety. Also, suppl
- Page 4
- Page 5B–63833EN–1/02 PREFACE PREFACE This manual describes all the NC functions required to enable machine tool builders to design their CNC machine tools. The following items are explained for each function. 1. General Describes feature of the function. Refer to Operator’s manual as requied. 2. Signals D
- Page 6PREFACE B–63833EN–1/02 Applicable models The models covered by this manual, and their abbreviations are : Model name Abbreviation FANUC Series 0i–TB 0i–TB Series 0i–B 0i FANUC Series 0i–MB 0i–MB FANUC Series 0i Mate–TB 0i Mate–TB Series 0i Mate–B 0i Mate FANUC Series 0i Mate–MB 0i Mate–MB NOTE Some
- Page 7B–63833EN–1/02 PREFACE Parameter description Parameters are classified by data type as follows : Dta type Valid data range Remarks Bit 0 or 1 Bit axis Byte –128 to 127 In some parameters, signs are ig- Byte axis 0 to 255 nored. Word –32768 to 32767 Word axis 0 to 65535 2–word –99999999 to 2–word axi
- Page 8PREFACE B–63833EN–1/02 D Notation of bit type and bit axis type parameters Data No. Data (#0 to #7 indicates bit position) #7 #6 #5 #4 #3 #2 #1 #0 0000 SEQ INI ISO TVC D Notation of parameters other than bit type and bit axis type Data No. Data 1023 Servo axis number of a specific axis NOTE In an it
- Page 9B–63833EN–1/02 PREFACE Related manuals of The following table lists the manuals related to Series 0i–B and 0i Series 0i–B/0i Mate–B Mate–B. This manual is indicated by an asterisk(*). Specification Manual name number DESCRIPTIONS B–63832EN CONNECTION MANUAL (HARDWARE) B–63833EN CONNECTION MANUAL (FU
- Page 10PREFACE B–63833EN–1/02 Related manuals of The following table lists the manuals related to Servo Motor ai series Servo Motor ai series Specification Manual name number FANUC AC SERVO MOTOR ai series DESCRIPTIONS B–65262EN FANUC AC SERVO MOTOR ai series B–65270EN PARAMETER MANUAL FANUC AC SPINDLE MOT
- Page 11B–63833EN–1/02 Table of Contents Volume 1 DEFINITION OF WARNING, CAUTION, AND NOTE . . . . . . . . . . . . . . . . . . . . . . . . . . . . . s–1 PREFACE . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . p–1 1. AXIS C
- Page 12TABLE OF CONTENTS B–63833EN–1/02 2.10 SERVO/SPINDLE MOTOR SPEED DETECTION . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 154 3. MANUAL OPERATION . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 159 3.1 JOG FEED/INCRE
- Page 13B–63833EN–1/02 TABLE OF CONTENTS 7. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL . . . . . 304 7.1 FEEDRATE CONTROL . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 305 7.1.1 Rapid Traverse Rate . . . . . . . . . . . . . .
- Page 14TABLE OF CONTENTS B–63833EN–1/02 9.10.1 General . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 525 9.10.2 Connection Among Spindle, Spindle Motor, and Position Coder . . . . . . . . . . . . . . . . . . . . . . 527
- Page 15B–63833EN–1/02 TABLE OF CONTENTS 11.5.1 Custom Macro . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 649 11.5.2 Interruption Type Custom Macro . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .
- Page 16TABLE OF CONTENTS B–63833EN–1/02 13.3 EXTERNAL I/O DEVICE CONTROL . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 790 13.4 EXTERNAL PROGRAM INPUT . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 797 13
- Page 17B–63833EN–1/02 TABLE OF CONTENTS 17.6 ERROR MESSAGES . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 979 17.6.1 EMB_ETH MASTER CTRL LOG Screen . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 979
- Page 18
- Page 19B–63833EN–1/02 1. AXIS CONTROL 1 AXIS CONTROL 1
- Page 201. AXIS CONTROL B–63833EN–1/02 1.1 CONTROLLED AXES General Series 0i–B Item M series T series Controlled path 1 path 1 path Controlled axes 4 axes 2 axes Simultaneously Max. 4 axes Max. 4 axes controlled axes Axis control by PMC Max. simultaneous 4 Max. simultaneous 4 axes (Not available on axes (No
- Page 21B–63833EN–1/02 1. AXIS CONTROL Alarm and message Number Message Description 015 TOO MANY AXES COM- The number of the commanded axes MANDED exceeded that of simultaneously con- (M series) trolled axes. Correct the program. TOO MANY AXES An attempt was made to move the ma- COMMANDED chine along the ax
- Page 221. AXIS CONTROL B–63833EN–1/02 1.2 SETTING EACH AXIS 1.2.1 Name of Axes General Each axis that is controlled by the CNC (including those controlled by the PMC) must be named. Select and set names from among X, Y, Z, A, B, C, U, V, and W (with parameter 1020). The names of the basic axes, however, ar
- Page 23B–63833EN–1/02 1. AXIS CONTROL NOTE 1 With the T series, when G code system A is used, neither U, V, nor W can be used as an axis name. Only when G code system B or C is used, U, V, and W can be used as axis names. 2 The same axis name cannot be assigned to more then one axis. 3 When the secondary a
- Page 241. AXIS CONTROL B–63833EN–1/02 1.2.2 Increment System General The increment system consists of the least input increment (for input ) and least command increment (for output). The least input increment is the least increment for programming the travel distance. The least command increment is the lea
- Page 25B–63833EN–1/02 1. AXIS CONTROL NOTE Diameter programming is used only for T series. Diameter programming or radius programming is determined by parameter DIAx (No. 1006#3) for each axis. Also, parameter IPR (No. 1004#7) can make the least input increment of IS–B and IS–C ten times the least command
- Page 261. AXIS CONTROL B–63833EN–1/02 NOTE IS–A is not available. IPR Whether the least input increment for each axis is set to a value 10 times as large as the least command increment is specified, in increment systems of IS–B and IS–C, mm input. 0 : The least input increment is not set to a value 10 time
- Page 27B–63833EN–1/02 1. AXIS CONTROL 1.2.3 Specifying the Rotation Axis General Bit 0 (ROTx) of parameter 1006 can be used to set each axis to a linear axis or rotation axis. Bit 1 (ROSx) of parameter 1006 can be used to select the rotation axis type, A or B, for each axis. See the explanation of the para
- Page 281. AXIS CONTROL B–63833EN–1/02 ROSx ROTx Meaning 1 0 Setting is invalid (unused) 1 1 Rotation axis (B type) (1) Inch/metric conversion is not done. (2) Machine coordinate values, absolute coordinate values and relative coordinate values are linear axis type. (Is not rounded in 0 to 360_) (3) Stored
- Page 29B–63833EN–1/02 1. AXIS CONTROL 1260 Amount of a shift per one rotation of a rotation axis NOTE 1 After setting the parameter, turn off the power once and turn it on again to operate the machine. 2 This parameter is valid only when ROAx = 1. [Data type] Two–word axis [Unit of data] Increment system U
- Page 301. AXIS CONTROL B–63833EN–1/02 1.2.4 Outputting the Movement State of an Axis General The movement state of each axis can be output to the PMC. Signal Axis moving signals MV1 – MV4
[Classification] Output signal [Function] These signals indicate that a control axis is moving. The signals are - Page 31B–63833EN–1/02 1. AXIS CONTROL Axis moving direction signals MVD1 – MVD4
[Classification] Output signal [Function] These signals indicate the movement direction of control axis. They are provided for each control axis, and the number in the signal name corresponds to the control axis number. - Page 321. AXIS CONTROL B–63833EN–1/02 Caution CAUTION Axis moving signals and axis moving direction signals are output in both automatic and manual operations. 1.2.5 Mirror Image General Mirror image can be applied to each axis, either by signals or by parameters (setting input is acceptable). All movement
- Page 33B–63833EN–1/02 1. AXIS CONTROL MI 1 1 ..... Applies mirror image to the 1st axis. 2 ..... Applies mirror image to the 2nd axis. 3 ..... Applies mirror image to the 3rd axis. : : : : The mirror image signal can be turned to “1” in the following cases: a) During offset cancel; b) When the CNC is in th
- Page 341. AXIS CONTROL B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 0012 MIRx The following parameter can be set at “Setting screen.” [Data type] Bit axis MIRx Mirror image for each axis 0 : Mirror image is off. 1 : Mirror image is on. Warning WARNING 1 When programmable mirror image (M series) and ord
- Page 35B–63833EN–1/02 1. AXIS CONTROL 1.2.6 Follow–up General When position control is disabled for the controlled axes (when the servo is off, during emergency stop, or during a servo alarm), if the machine is moved, a positional error occurs. Follow–up is a function for changing the current position of t
- Page 361. AXIS CONTROL B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 1819 FUPx [Data type] Bit axis FUPx To perform follow–up when the servo is off for each axis. 0 : The follow–up signal, *FLWU, determines whether follow–up is performed or not. When *FLWU is 0, follow–up is performed. When *FLWU is 1,
- Page 37B–63833EN–1/02 1. AXIS CONTROL 1.2.7 Servo Off (Mechanical Handle) General Place the controlled axes in the servo off state, stop the current to the servo motor, which disables position control. However, the position detection feature functions continuously, so the current position is not lost. Thes
- Page 381. AXIS CONTROL B–63833EN–1/02 Caution CAUTION 1 In general, interlock is applied to an axis while the servo off signal for that axis is 1. 2 When one of these signals turns to “1”, the servo motor is turned off. The mechanical clamp is done by using the auxiliary function. Set the timing for the au
- Page 39B–63833EN–1/02 1. AXIS CONTROL 1.2.8 Position Switch General Position switch signals can be output to the PMC while the machine coordinates along a controlled axes are within a specified ranges. Signal Position switch signal PSW01 – PSW16
- Page 401. AXIS CONTROL B–63833EN–1/02 Parameter D Increasing the number of position switch signals #7 #6 #5 #4 #3 #2 #1 #0 6901 PSF PCM EPS IGP [Data type] Bit IGP During follow–up for the absolute position detector, position switch signals are: 0 : Output 1 : Not output EPS The number of position switches
- Page 41B–63833EN–1/02 1. AXIS CONTROL D Setting the correspondence between the position switch signals and the controlled axes 6910 Axis corresponding to the first position switch 6911 Axis corresponding to the second position switch 6912 Axis corresponding to the third position switch 6913 Axis correspond
- Page 421. AXIS CONTROL B–63833EN–1/02 D Setting the machine coordinate ranges for which the position switch signals are output D Maximum operation range 6930 Maximum operation range of the first position switch 6931 Maximum operation range of the second position switch 6932 Maximum operation range of the t
- Page 43B–63833EN–1/02 1. AXIS CONTROL D Minimum operation range 6950 Minimum operation range of the first position switch 6951 Minimum operation range of the second position switch 6952 Minimum operation range of the third position switch 6953 Minimum operation range of the fourth position switch 6954 Mini
- Page 441. AXIS CONTROL B–63833EN–1/02 1.3 ERROR COMPENSATION 1.3.1 Stored Pitch Error Compensation General If pitch error compensation data is specified, pitch errors of each axis can be compensated in detection units per axis. Pitch error compensation data is set for each compensation position at the inte
- Page 45B–63833EN–1/02 1. AXIS CONTROL · Interval of the pitch error compensation positions (for each axis): Parameter 3624 Procedure for displaying 1 Set the following parameters: and setting the pitch ⋅ Pitch error compensation position at the reference position (for error compensation data each axis): Pa
- Page 461. AXIS CONTROL B–63833EN–1/02 Explanations D Specifying the To assign the compensation positions for each axis, specify the positive compensation position direction or the negative direction relative to the compensation position No. of the reference position. If the machine stroke exceeds the speci
- Page 47B–63833EN–1/02 1. AXIS CONTROL The correspondence between the machine coordinate and the compensation position No. is as follows: –400 –350 –100 –50 0 50 100 750 800 Machine coordinate (mm) Compensation position number. 33 39 40 41 42 56 Compensation values are output at the positions indicated by .
- Page 481. AXIS CONTROL B–63833EN–1/02 D For rotary axis ⋅Amount of movement per rotation: 360° ⋅ Interval between pitch error compensation positions: 45° ⋅ No. of the compensation position of the reference position: 60 If the above is specified, the No. of the farthest compensation position in the negative
- Page 49B–63833EN–1/02 1. AXIS CONTROL The following is an example of compensation amounts. No 60 61 62 63 64 65 66 67 68 Compensation value +1 –2 +1 +3 –1 –1 –3 +2 +1 Pitch error compensation value (absolute value) +4 +3 Reference position 68 +2 (60) +1 68 61 62 63 64 65 66 67 61 62 63 64 65 66 67 (60) 61
- Page 501. AXIS CONTROL B–63833EN–1/02 3622 Number of the pitch error compensation position at extreme positive position for each axis NOTE After setting this parameter, turn the power off then on again so that the setting will take effect. [Data type] Word axis [Unit of data] Number [Valid data range] 0 to
- Page 51B–63833EN–1/02 1. AXIS CONTROL [Valid data range] 0 to 99999999 The pitch error compensation positions are equally spaced to parameter No. 3624. Set the space between two adjacent positions for each axis. The minimum interval between pitch error compensation positions is limited and obtained from th
- Page 521. AXIS CONTROL B–63833EN–1/02 Warning WARNING 1 Compensation value range Compensation values can be set within the range from –7 x compensation magnification (detection unit) to +7 x compensation magnification (detection unit). The compensation magnification can be set for each axis within the rang
- Page 53B–63833EN–1/02 1. AXIS CONTROL Reference item Inputting pitch error compensa- III.8.6.3 tion data OPERATOR’S MANUAL Outputting pitch error com- III.8.6.4 (M series) (B–63844EN) pensation data Displaying and setting pitch error III.11.5.2 compensation data Series 0i–B Inputting pitch error compensa-
- Page 541. AXIS CONTROL B–63833EN–1/02 1.3.2 Backlash Compensation General D Backlash compensation Function for compensating for lost motion on the machine. Set a compensation value in parameter No. 1851, in detection units from 0 to "9999 pulses for each axis. D Backlash compensation More precise machining
- Page 55B–63833EN–1/02 1. AXIS CONTROL Parameter #7 #6 #5 #4 #3 #2 #1 #0 1800 RBK [Data type] Bit RBK Backlash compensation applied separately for cutting feed and rapid traverse 0 : Not performed 1 : Performed 1851 Backlash compensating value for each axis [Data type] Word axis [Unit of data] Detection uni
- Page 561. AXIS CONTROL B–63833EN–1/02 1.4 The servo interface of the Series 16 features the following: SETTINGS RELATED S Digitally controlled AC servo motor TO SERVO– S Motor feedback with serial pulse coders CONTROLLED AXES (1) Absolute pulse coder with a resolution of 1,000,000 pulses/rev (2) Absolute p
- Page 57B–63833EN–1/02 1. AXIS CONTROL Parameter #7 #6 #5 #4 #3 #2 #1 #0 1800 CVR [Data type] Bit CVR When velocity control ready signal VRDY is set ON before position control ready signal PRDY comes ON 0 : A servo alarm is generated. 1 : A servo alarm is not generated. #7 #6 #5 #4 #3 #2 #1 #0 1815 APCx APZ
- Page 581. AXIS CONTROL B–63833EN–1/02 [Data type] Bit axis DM1x to DM3x Setting of detection multiplier Set value Detection multiplier DM3x DM2x DM1x 0 0 0 1/2 0 0 1 1 0 1 0 3/2 0 1 1 2 1 0 0 5/2 1 0 1 3 1 1 0 7/2 1 1 1 4 NOTE When the flexible feed gear is used, do not use these parameters. Set the numera
- Page 59B–63833EN–1/02 1. AXIS CONTROL (2) When command multiplier is 1 to 48 Set value = 2 command multiplier Valid data range: 2 to 96 NOTE When command multiplier is 1 to 48, the set value must be determined so that an integer can be set for command multiplier. 1821 Reference counter size for each axis [
- Page 601. AXIS CONTROL B–63833EN–1/02 Set the positioning deviation limit in movement for each axis. If the positioning deviation exceeds the positioning deviation limit during movement, a servo alarm is generated, and operation is stopped immediately (as in emergency stop). Generally, set the positioning
- Page 61B–63833EN–1/02 1. AXIS CONTROL 1.4.2 Absolute Position Detection General Even when the power to the CNC is turned off, a battery–powered pulse coder stores the current position. No reference position return is required when the power to the CNC is restored. Signal Absolute position detector battery
- Page 621. AXIS CONTROL B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 F172 PBATL PBATZ Parameter #7 #6 #5 #4 #3 #2 #1 #0 1815 APCx NOTE When this parameter has been set, the power must be turned off before operation is continued. [Data type] Bit axis APCx Position detector 0: Other than absolute pos
- Page 63B–63833EN–1/02 1. AXIS CONTROL 1.4.3 FSSB Setting Overview Connecting the CNC control section to servo amplifiers via a high–speed serial bus (FANUC Serial Servo Bus, or FSSB), which uses only one fiber optics cable, can significantly reduce the amount of cabling in machine tool electrical sections.
- Page 641. AXIS CONTROL B–63833EN–1/02 Slave In an FSSB–based system, a fiber optics cable is used to connect the CNC to servo amplifiers and separate detector interface units. These amplifiers and separate detector interface units are called slaves. The two–axis amplifier consists of two slaves, and the th
- Page 65B–63833EN–1/02 1. AXIS CONTROL D The following servo functions cannot be used: - High–speed current loop - High–speed interface axis Automatic setting Automatic setting can be used on the FSSB setting screen, if the following parameter is set as follows: Bit 0 of parameter No. 1902 = 0 On the FSSB s
- Page 661. AXIS CONTROL B–63833EN–1/02 Manual setting 2 If the following parameter is set, manual setting 2 can be used for each parameter axis setting. Bit 0 of parameter No. 1902 = 1 To perform manual setting 2, set parameter Nos. 1023, 1905, 1910 to 1919, 1936, and 1937. Refer to the Parameter Manual for
- Page 67B–63833EN–1/02 1. AXIS CONTROL FSSB display and setting procedure D Display The FSSB setting screen displays FSSB–based amplifier and axis information. This information can also be specified by the operator. 1. Press the SYSTEM function key. 2. To display [FSSB], press the next menu page key several
- Page 681. AXIS CONTROL B–63833EN–1/02 D AMP . . . . amplifier type The amplifier type display consists of the letter A, which stands for “amplifier”, a number that indicates the placing of the amplifier, as counted from that nearest to the CNC, and a letter such as L (first axis) or M (second axis) indicat
- Page 69B–63833EN–1/02 1. AXIS CONTROL (2) Axis setting screen The axis setting screen displays the information shown below: AXIS SETTING O1000 N00001 AXIS NAME AMP M1 M2 1–DSP CS TNDM 1 X A1–L 0 0 0 0 1 2 Y A2–L 1 0 1 0 0 3 Z A2–M 0 0 0 1 0 4 A A3–L 0 0 0 0 2 >_ MDI **** *** *** 13:11:56 [ AMP ][ AXIS ][ M
- Page 701. AXIS CONTROL B–63833EN–1/02 (3) Amplifier maintenance screen The amplifier maintenance screen displays maintenance information for servo amplifiers. This screen consists of the following two pages, PAGE either of which can be selected by pressing the PAGE or key. AMPLIFIER MAINTENANCE O1000 N0000
- Page 71B–63833EN–1/02 1. AXIS CONTROL D TEST . . . . . . . . . date of test performed on an amplifier connected to each axis Example) 010123 = January 23, 2001 D MEINTE–No. . . engineering change number for an amplifier connected to each axis D Setting On an FSSB setting screen (other than the amplifier ma
- Page 721. AXIS CONTROL B–63833EN–1/02 The amplifier setting screen displays the following items: D AXIS . . . controlled axis number For this item, enter a value of between 1 and the maximum number of controlled axes. If a number that falls outside this range is entered, the warning message FORMAT ERROR ap
- Page 73B–63833EN–1/02 1. AXIS CONTROL D TNDM This item is not used in Series 0i and Series 0i Mate. When the [SETING] soft key is pressed on the axis setting screen after data entry, the message DATA IS OUT OF RANGE is displayed if any of the following conditions is satisfied. D Both M1 and M2 are nonzero
- Page 741. AXIS CONTROL B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 1905 PM2 PM1 FSL [Data type] Bit axis FSL Specifies whether to use a fast or slow interface between a servo amplifier and the servo software. 0 : Fast type 1 : Slow type There are two types of servo data transfer interfaces: fast and slow types.
- Page 75B–63833EN–1/02 1. AXIS CONTROL 1910 Address conversion table value for slave 1 (ATR) 1911 Address conversion table value for slave 2 (ATR) 1912 Address conversion table value for slave 3 (ATR) 1913 Address conversion table value for slave 4 (ATR) 1914 Address conversion table value for slave 5 (ATR)
- Page 761. AXIS CONTROL B–63833EN–1/02 f Example of axis configuration and parameter setting CNC Slave ATR Controlled Program Servo axis number No.1910 Axis axis axis name number to 1919 number (No. 1020) (No. 1023) Single–axis 1 0 1 X 1 amplifier X 2 Y 3 2 1 A Two–axis amplifier 3 Z 4 3 2 Y 4 A 2 M1 4 16 (
- Page 77B–63833EN–1/02 1. AXIS CONTROL 1920 Controlled axis number for slave 1 (FSSB setting screen only) 1921 Controlled axis number for slave 2 (FSSB setting screen only) 1922 Controlled axis number for slave 3 (FSSB setting screen only) 1923 Controlled axis number for slave 4 (FSSB setting screen only) 1
- Page 781. AXIS CONTROL B–63833EN–1/02 1936 Connector number for first separate detector interface unit 1937 Connector number for second separate detector interface unit [Data type] Byte axis [Valid data range] 0 to 7 To use a separate detector interface unit, this parameter must be set to “connection numbe
- Page 79B–63833EN–1/02 1. AXIS CONTROL Alarm and message D Servo alarms Number Message Description 456 ILLEGAL CURRENT The current control cycle settings (pa- LOOP rameter No. 2004, bit 0 of parameter No. 2003, and bit 0 of parameter No. 2013) are incorrect. Possible problems are as follows. – For the two a
- Page 801. AXIS CONTROL B–63833EN–1/02 Number Message Description 466 n AXIS : MOTOR/AMP The maximum current rating for the am- COMBINATION plifier does not match that for the motor. 467 n AXIS : ILLEGAL SET- The servo function for the following has TING OF AXIS not been enabled when an axis occu- pying a s
- Page 81B–63833EN–1/02 1. AXIS CONTROL Number Message Description 5198 FSSB : ID DATA NOT The initial ID information for the amplifi- READ er cannot be read because of a failure in the temporary assignment. 5311 FSSB: ILLEGAL CON- A connection related to FSSB is illegal. NECTION This alarm is issued when ei
- Page 821. AXIS CONTROL B–63833EN–1/02 1.5 SETTINGS RELATED WITH COORDINATE SYSTEMS 1.5.1 Machine Coordinate System General Machine coordinate system is a coordinate system set with a zero point proper to the machine system. A coordinate system in which the reference position becomes the parameter-preset (N
- Page 83B–63833EN–1/02 1. AXIS CONTROL [Valid data range] –99999999 to 99999999 Set the coordinate values of the reference positions in the machine coordinate system. 1722 Rapid traverse deceleration rate at inter–rapid traverse block overlap [Data type] Byte axis [Unit of data] % [Valid data range] 0 to 10
- Page 841. AXIS CONTROL B–63833EN–1/02 1.5.2 Workpiece Coordinate System/Addition of Workpiece Coordinate System Pair General A coordinate system used for machining a workpiece is referred to as a workpiece coordinate system. A workpiece coordinate system is to be set with the CNC beforehand (setting a work
- Page 85B–63833EN–1/02 1. AXIS CONTROL Changing workpiece The six workpiece coordinate systems specified with G54 to G59 can be coordinate system changed by changing an external workpiece zero point offset value or workpiece zero point offset value. Three methods are available to change an external workpiec
- Page 861. AXIS CONTROL B–63833EN–1/02 Addition of workpiece Besides the six workpiece coordinate systems (standard workpiece coordinate system pair coordinate systems) selectable with G54 to G59, 48 additional workpiece (M series) coordinate systems (additional workpiece coordinate systems) can be used. Pa
- Page 87B–63833EN–1/02 1. AXIS CONTROL G50 When the CNC has commands G54 to G59 specifying workpiece coordinate systems (optional function), if the G50 command for setting a coordinate system (or the G92 command in G command system B or C) is specified, 0 : The G50 (or G92) command is executed without an al
- Page 881. AXIS CONTROL B–63833EN–1/02 Workpiece coordinate system 1 (G54) Workpiece coordinate system 2 (G55) Workpiece zero point offset Origin of machine coordinate system #7 #6 #5 #4 #3 #2 #1 #0 3108 WCI [Data type] Bit WCI On the workpiece coordinate system screen, a counter input is: 0 : Disabled. 1 :
- Page 89B–63833EN–1/02 1. AXIS CONTROL 1.5.3 Rotary Axis Roll Over General The roll–over function prevents coordinates for the rotation axis from overflowing. The roll–over function is enabled by setting bit 0 (ROAx) of parameter 1008 to 1. For an incremental command, the tool moves the angle specified in t
- Page 901. AXIS CONTROL B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 1008 RRLx RABx ROAx NOTE After setting this parameter, turn the power off then on again so that the setting will take effect. [Data type] Bit axis ROAx The roll–over function of a rotation axis is 0 : Invalid 1 : Valid NOTE ROAx specifies the fu
- Page 91B–63833EN–1/02 1. AXIS CONTROL Note NOTE This function cannot be used together with the indexing function of the index table (M series). Reference item OPERATOR’S MANUAL II.20.2 ROTARY AXIS ROLL–OVER (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.18.2 ROTARY AXIS ROLL–OVER (T series) (B–638
- Page 921. AXIS CONTROL B–63833EN–1/02 1.6 SIMPLE SYNCHRONOUS CONTROL General A movement along an axis can be executed simply by executing a move command specified for that axis or by synchronizing the movement with another axis. Either of these two types can be selected by means of a signal sent from the m
- Page 93B–63833EN–1/02 1. AXIS CONTROL WARNING 1 Before using the synchronization error check function, set identical values for the reference positions of the master and slave axes. 2 To clear the alarm, first increase the maximum synchronization error set in parameter 8314, then press the reset key. Next,
- Page 941. AXIS CONTROL B–63833EN–1/02 NOTE 1 To use the synchronization compensation function, set the SOF bit, bit 7 of parameter 8301 (if only one master/slave axis pair is in sync) or SOFx bit, bit 7 of parameter 8303 (if two master/slave axis pair is in sync), to 1. 2 The synchronization compensation f
- Page 95B–63833EN–1/02 1. AXIS CONTROL D Torque difference alarm If the master and slave axes operate independently while simple detection (M series) synchronous control is applied, the machine may be damaged. To prevent this, the torque command difference between the axes is monitored. If the difference is
- Page 961. AXIS CONTROL B–63833EN–1/02 5 Connect a check board to observe torque differences. If an analog check board is used, set the rotary switch of the check board to 1, and observe signals on CH7. If the oscilloscope is a combined analog/digital model, set the DATA digit for CH1 to 5, and observe sign
- Page 97B–63833EN–1/02 1. AXIS CONTROL
Signals for selecting the manual feed axis for simple synchronous control SYNCJ1 to SYNCJ4 [Classification] Input signal [Function] synchronous control is performed in jog, handle, or incremental feed mode. The signal is provided for each controlled a - Page 981. AXIS CONTROL B–63833EN–1/02 Parameter T series 1010 Number of CNC–controlled axes NOTE When this parameter is set, the power must be turned off before operation is continued. [Data type] Byte [Valid data range] 1, 2, 3, ..., the number of controlled axes Set the maximum number of axes that can be
- Page 99B–63833EN–1/02 1. AXIS CONTROL Units digit in the parameter for the first axis → Set the axis number for the master axis when the first axis is used as a slave axis. Tens digit in the parameter for the first axis → Set the axis number for the master axis when the second axis is used as a slave axis.
- Page 1001. AXIS CONTROL B–63833EN–1/02 M series 1010 Number of CNC–controlled axes NOTE When this parameter is set, the power must be turned off before operation is continued. [Data type] Byte [Valid data range] 1, 2, 3, ..., the number of controlled axes Set the maximum number of axes that can be controlle
- Page 101B–63833EN–1/02 1. AXIS CONTROL #7 #6 #5 #4 #3 #2 #1 #0 8302 ATS ATE NOTE The system power must be turned off then back on in order for this parameter setting to become effective. [Data type] Bit ATE Specify whether to enable the automatic setting of grid positioning under simple synchronous control
- Page 1021. AXIS CONTROL B–63833EN–1/02 8311 Axis number of master axis in synchronous control [Data type] Byte axis [Valid data range] 0 to 3 Select a master axis and slave axis for simple synchronous control. Set a master axis number for the slave axis side. A maximum of two pairs can be synchronized. Exam
- Page 103B–63833EN–1/02 1. AXIS CONTROL 8314 Allowable error in synchronization error check [Data type] Word axis [Unit of data] Increment system IS–A IS–B IS–C Unit Metric machine 0.01 0.001 0.0001 mm Inch machine 0.001 0.0001 0.00001 inch Rotation axis 0.01 0.001 0.0001 deg [Valid data range] 0 to 32767 Th
- Page 1041. AXIS CONTROL B–63833EN–1/02 8317 Torque difference alarm detection timer (one master/slave axis pair under synchro- nous control) [Data type] Word [Unit of data] ms [Valid data range] 0 to 4000 (if 0 is specified, the system assumes 512 ms.) This parameter specifies the time between the servo pre
- Page 105B–63833EN–1/02 1. AXIS CONTROL 8327 Torque difference alarm detection timer (two pair under synchronous control) [Data type] Word axis [Unit of data] ms [Valid data range] 0 to 4000 This parameter specifies the time between the servo preparation completed signal SA
- Page 1061. AXIS CONTROL B–63833EN–1/02 Servo alarm Number Message Description 407 SERVO ALARM: The following error has occurred during EXCESS ERROR an operation under simplified synchro- nization control: The difference in machine coordinate value between axes in synchronization has exceeded a value specifi
- Page 107B–63833EN–1/02 1. AXIS CONTROL Caution CAUTION 1 Set the same detection unit for both the master and slave axes. 2 When a manual reference position return is executed, identical movements are performed along the master and slave axes until deceleration commences. Subsequently, grids are detected sep
- Page 1081. AXIS CONTROL B–63833EN–1/02 1.7 ANGULAR AXIS CONTROL General When the angular axis makes an angle other than 90° with the perpendicular axis, the angular axis control function controls the distance traveled along each axis according to the inclination angle. For the angular axis control function,
- Page 109B–63833EN–1/02 1. AXIS CONTROL D Absolute and relative An absolute and a relative position are indicated in the programmed position display Cartesian coordinate system. D Machine position display A machine position indication is provided in the machine coordinate system where an actual movement is t
- Page 1101. AXIS CONTROL B–63833EN–1/02 Warning WARNING 1 After angular axis control parameter setting, be sure to perform manual reference point return operation. 2 If bit 2 (AZK) of parameter No. 8200 has been set to 0, such that manual reference position return along the angular axis also causes movement
- Page 111B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2 PREPARATIONS FOR OPERATION 93
- Page 1122. PREPARATIONS FOR OPERATION B–63833EN–1/02 2.1 EMERGENCY STOP General If you press Emergency Stop button on the machine operator’s panel, the machine movement stops in a moment. Red EMERGENCY STOP Fig. 2.1 (a) EMERGENCY STOP This button is locked when it is pressed. Although it varies with the mac
- Page 113B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Emergency stop limit switch Emergency stop +X =X +Y =Y +Z =Z +4 =4 Relay power Emergency stop temporary release supply EMG SK Spark killer Fig. 2.1 (b) Connection of emergency stop limit switch The distance from the position where the dynamic brake is app
- Page 1142. PREPARATIONS FOR OPERATION B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 X008 *ESP #7 #6 #5 #4 #3 #2 #1 #0 G008 *ESP Reference item FANUC AC SERVO MOTOR αi series B–65262EN DESCRIPTIONS 96
- Page 115B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.2 CNC READY SIGNAL General When the CNC is turned on and becomes ready for operation, the CNC ready signal is set to 1. Signal CNC Ready Signal MA
- Page 1162. PREPARATIONS FOR OPERATION B–63833EN–1/02 Servo Ready Signal SA
- Page 117B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.3 OVERTRAVEL CHECK 2.3.1 Overtravel Signal General When the tool tries to move beyond the stroke end set by the machine tool limit switch, the tool decelerates and stops as a result of tripping the limit switch, and an OVER TRAVEL is displayed. Signal O
- Page 1182. PREPARATIONS FOR OPERATION B–63833EN–1/02 The following shows the deceleration distance at overtravel. (i) Rapid traverse Command pulse deceleration V ÄÄÄÄ ÄÄÄ Servo system delay ÄÄÄÄ ÄÄÄ ÄÄÄÄ ÄÄÄ VR t ÄÄÄÄ ÄÄÄ *+La limit switch t1 t2 TR TR 1 L1=VR(t1+t2+ +TS) · [mm or inch] 2 60000 L1:Decelerati
- Page 119B–63833EN–1/02 2. PREPARATIONS FOR OPERATION D Releasing overtravel First, move the tool into a safe zone under manual operation. Then press the reset button to reset the alarm. Signal address #7 #6 #5 #4 #3 #2 #1 #0 G114 *+L4 *+L3 *+L2 *+L1 G116 *–L4 *–L3 *–L2 *–L1 Parameter #7 #6 #5 #4 #3 #2 #1 #0
- Page 1202. PREPARATIONS FOR OPERATION B–63833EN–1/02 2.3.2 Stored Stroke Check 1 General When the tool tries to moved beyond a stored stroke check limit, an alarm is displayed and the tool is decelerated and stopped. When the tool enters a forbidden zone and an alarm is generated, the tool may only be moved
- Page 121B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Axis direction dependent stored stroke limit switch signal +EXL1 to +EXL4
–EXL1 to –EXL4 [Classification] Input signal [Function] Switches between stroke limit 1–I (parameter No. 1320 and No. 1321) and stroke limit 1–II (parameter No. 1326 and - Page 1222. PREPARATIONS FOR OPERATION B–63833EN–1/02 Stroke limit reached signals +OT1 to +OT4
–OT1 to –OT4 (M series) [Classification] Output signal [Function] Notify that the tool is about to enter the forbidden area of stored stroke check 1. Each direction of each controlled axis has one st - Page 123B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Parameter #7 #6 #5 #4 #3 #2 #1 #0 1300 BFA LZR LMS NAL [Data type] Bit NAL Specifies whether to issue an alarm related to stored stroke check 1, as follows: 0 : To issue an alarm. 1 : Not to issue an alarm; the stroke limit reached signal F124 or F126 is
- Page 1242. PREPARATIONS FOR OPERATION B–63833EN–1/02 CAUTION In the cases below, the automatic release function is disabled. To release an alarm, a reset operation is required. 1 When a setting is made to issue an alarm before a stored stroke limit is exceeded (bit 7 (BFA) of parameter No. 1300) 2 When an a
- Page 125B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 1326 Coordinate value II of stored stroke check 1 in the positive direction on each axis 1327 Coordinate value II of stored stroke check 1 in the negative direction each axis [Data type] Two–word axis [Unit of data] Increment system IS–A IS–B IS–C Unit Me
- Page 1262. PREPARATIONS FOR OPERATION B–63833EN–1/02 Note NOTE 1 Parameter LZR (bit 6 of No. 1300) selects whether each check becomes effective after the power is turned on and manual reference position return or automatic reference position return by G28 has been performed or immediately after the power is
- Page 127B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.3.3 Stored Stroke Check 2, 3 General Three areas which the tool cannot enter can be specified with stored stroke check 1, stored stroke check 2,and stored stroke check 3. ÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇ ÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇ ÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇ ÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇÇ ÇÇ
- Page 1282. PREPARATIONS FOR OPERATION B–63833EN–1/02 Stored stroke check 2 The stored stroke check 2 values are set either by parameters (Nos. 1322, 1323) or by command. The foribidden area may be defined as the area external to the limits, or internal to the limits. This is determinal by the value in param
- Page 129B–63833EN–1/02 2. PREPARATIONS FOR OPERATION ÇÇÇÇÇÇÇÇ A(X1, Y1, Z1) ÇÇÇÇÇÇÇÇ ÇÇÇÇÇÇÇÇ B(X2, Y2, Z2) ÇÇÇÇÇÇÇÇ X1>X2, Y1>Y2, Z1>Z2 X1–X2> ζ (In least command increment) Y1–Y2> ζ (In least command increment) Z1–Z2> ζ (n least command increment) ζ is the distance the tool travels in 8 ms. It is 2000 in
- Page 1302. PREPARATIONS FOR OPERATION B–63833EN–1/02 B The position of the tool after reference position return b ÇÇÇÇÇÇÇÇÇÇÇÇÇÇ A a ÇÇÇÇÇÇÇÇÇÇÇÇÇÇ Forbidden area boundary ÇÇÇÇÇÇÇÇÇÇÇÇÇÇ Fig. 2.3.3 (h) Setting the forbidden area (M series) D Forbidden area over– Forbidden areas can be set to overlap. ÇÇÇÇÇÇ
- Page 131B–63833EN–1/02 2. PREPARATIONS FOR OPERATION D Change from G23 to When G23 is switched to G22 while the tool is in a forbidden area, the G22 in a forbidden area following results. (1) When the forbidden area is internal to the limits, an alarm is generated in the next move. (2) When the forbidden ar
- Page 1322. PREPARATIONS FOR OPERATION B–63833EN–1/02 BFA When a command is issued where the resulting motion would exceed the value of a stored stroke check 1, 3 0: An alarm is generated after the stroke check 1, 3 is exceeded. 1: An alarm is generated before the stroke check 1, 3 is exceeded. #7 #6 #5 #4 #
- Page 133B–63833EN–1/02 2. PREPARATIONS FOR OPERATION WARNING For axes with diameter specification, a diameter value must be set. 1324 Coordinate value of stored stored check 3 in the positive direction on each axis 1325 Coordinate value of stored stroke check 3 in the negatice direction on each axis [Data t
- Page 1342. PREPARATIONS FOR OPERATION B–63833EN–1/02 Warning WARNING 1 Whenever the two check limits are set to the same value, the following results are seen. (1)In the case of stored stroke check 1, all areas are prohibited. (2)In the case of stored stroke check 2 or 3, no areas are prohibited. 2 Whenever
- Page 135B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.3.4 Chuck/Tailstock Barrier (T series) General The chuck/tailstock barrier function prevents damage to the machine by checking whether the tool tip interferes with either the chuck or tailstock. Specify an area into which the tool may not enter (entry–p
- Page 1362. PREPARATIONS FOR OPERATION B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G060 *TSB Parameter D Profile of a chuck 1330 Profile TY of a chuck [Data type] Byte [Valid data range] 0 or 1 0 : Chuck which holds a workpiece on the inner surface 1 : Chuck which holds a workpiece on the outer sur
- Page 137B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Chuck which holds a workpiece on Chuck which holds a workpiece on the outer surface (TY=1) the inner surface (TY=0) X X L A L A W1 L1 W W W1 CX CX L1 Z Z CZ CZ Zero point of Zero point of the workpiece the workpiece coordinate coordinate system system Fig
- Page 1382. PREPARATIONS FOR OPERATION B–63833EN–1/02 1341 Length of a tailstock (L) 1342 Diameter of a tailstock (D) 1343 Length of a tailstock (L1) 1344 Diameter of a tailstock (D1) 1345 Length of a tailstock (L2) 1346 Diameter of a tailstock (D2) 1347 Diameter of the hole of a tailstock (D3) [Data type] T
- Page 139B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Symbol Description TZ Z–axis coordinate of a tailstock L Length of a tailstock D Diameter of a tailstock (diameter input) L1 Length of a tailstock (1) D1 Diameter of a tailstock (1) (diameter input) L2 Length of a tailstock (2) D2 Diameter of a tailstock
- Page 1402. PREPARATIONS FOR OPERATION B–63833EN–1/02 Warning WARNING 1 Invalid settings will result in the absence of a prohibited area, as follows: 1) In the setting of the chuck shape, if the jaw length (parameter No. 1331) is less than the grasp length (parameter No. 1333) or if the jaw width (parameter
- Page 141B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.4 ALARM SIGNAL General When an alarm is triggered in the CNC, the alarm is displayed on the screen, and the alarm signal is set to 1. If the voltage level of the memory backup battery falls to below a specified level while the CNC is turned off, the bat
- Page 1422. PREPARATIONS FOR OPERATION B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 3111 NPA [Data type] Bit NPA Action taken when an alarm is generated or when an operator message is entered 0 : The display shifts to the alarm or message screen. 1 : The display does not shift to the alarm or message scr
- Page 143B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.5 START LOCK/ INTERLOCK General These signals disable machine movement along axes. When any of these signals is activated during movement, tool movement along the affected axis (or axes) is decelerated, then stopped. Signal Start lock signal STLK
- Page 1442. PREPARATIONS FOR OPERATION B–63833EN–1/02 All axes Interlock signal *IT
- Page 145B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Interlock signal for each axis *IT1 to *IT4
[Classification] Input signal [Function] These signals disable feed along axes on an axis–by–axis basis. A separate interlock signal is provided for each controlled axis. The number at the end of each sign - Page 1462. PREPARATIONS FOR OPERATION B–63833EN–1/02 NOTE In the T series, when bit 4 (DAU) of parameter No. 3003 is 0, a directional interlock for each axis is applied only during manual operation. To allow a directional interlock for each axis also during automatic operation, set bit 4 (DAU) of parameter
- Page 147B–63833EN–1/02 2. PREPARATIONS FOR OPERATION NOTE This signal is effective for any blocks including blocks for cycle operation internally created by a canned cycle and so on. Signal address #7 #6 #5 #4 #3 #2 #1 #0 G007 STLK #7 #6 #5 #4 #3 #2 #1 #0 G008 *BSL *CSL *IT #7 #6 #5 #4 #3 #2 #1 #0 G130 *IT4
- Page 1482. PREPARATIONS FOR OPERATION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3004 BCY BSL [Data type] Bit BSL The block start interlock signal *BSL and cutting block start interlock signal *CSL are: 0 : Disabled. 1 : Enabled. BCY When more than one operation is performed by one block command such as a canne
- Page 149B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.6 MODE SELECTION General The mode select signal is a code signal consisting of the three bits MD1, MD2, and MD4. The following seven modes can be selected. D Memory edit (EDIT) D Memory operation (MEM) D Manual data input (MDI) D Manual handle/increment
- Page 1502. PREPARATIONS FOR OPERATION B–63833EN–1/02 For this example mode switching, only MD2 should change from 0 to 1. However if a transient signal status change were to occur in a signal other than MD2 during mode switching, another mode (manual continuous feed mode, for example) would be set between a
- Page 151B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Operation mode check signal MMDI, MMEM , MRMT, MEDT, MH, MINC, MJ, MREF, MTCHIN
- Page 1522. PREPARATIONS FOR OPERATION B–63833EN–1/02 Note NOTE Precautions on modes and mode switching 1 In MDI mode, the STL signal turns to “0” and the CNC stops as soon as the commands entered via the MDI have been executed. But the SPL signal does not turn to “1”. Therefore, another command can be enter
- Page 153B–63833EN–1/02 2. PREPARATIONS FOR OPERATION NOTE 4 Manual operation in TEACH IN JOG mode a) When bit 1 (THD) of parameter No. 7100 is set to 0 Only jog feed is possible. b) When bit 1 (THD) of parameter No. 7100 is set to 1 Both jog feed and manual handle feed are possible, provided the manual hand
- Page 1542. PREPARATIONS FOR OPERATION B–63833EN–1/02 NOTE 6 When the HANDLE/INC or TEACH IN HANDLE mode is selected while the CNC is operating in the MEM or MDI mode, the automatic or MDI operation stops, the STL signal turns to “0”, the SPL signal simultaneously turns to “1”, and the CNC enters the HANDLE/
- Page 155B–63833EN–1/02 2. PREPARATIONS FOR OPERATION NOTE 7 When the JOG or TEACH IN JOG mode is selected during RMT, MEM or MDI mode operation, operation stops, the STL signal turns to “0”, the SPL signal simultaneously turns to “1”, and the CNC enters the JOG or TEACH IN JOG mode. Under these conditions,
- Page 1562. PREPARATIONS FOR OPERATION B–63833EN–1/02 NOTE 8 The mode switching operation is summarized in the time chart below (Fig. 2.6 (f)). M M M M D D D Disable because of Disable because of feed hold state of MDI operation possible here- feed hold state of automatic operation MDI operation after H / S
- Page 157B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.7 STATUS OUTPUT SIGNAL General The table below lists the status output signals. They indicate the state of the CNC. See the sections listed in the table for details of each signal. Signal name Symbol Reference section Alarm signal AL 2.4 Battery alarm s
- Page 1582. PREPARATIONS FOR OPERATION B–63833EN–1/02 NOTE 1 Rapid traverse in automatic operation includes all rapid traverses in canned cycle positioning, automatic reference point return, etc., as well as the move command G00. Rapid traverse in manual operation also includes rapid traverse in reference po
- Page 159B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.8 VRDY OFF ALARM IGNORE SIGNAL General The German VDE safety standard requires that the motor be deactivated when the safety guard is opened. By using the VRDY OFF Alarm Ignore signal, however, the CNC can be restarted without resetting, even if the saf
- Page 1602. PREPARATIONS FOR OPERATION B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G066 IGNVRY G192 IGVRY4 IGVRY3 IGVRY2 IGVRY1 Parameter #7 #6 #5 #4 #3 #2 #1 #0 1804 SAK [Data type] Bit SAK When the VRDY OFF Alarm Ignore signal IGNVRY is 1, or when any of the VRDY OFF Alarm Ignore signals IGVRY1 t
- Page 161B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 2.9 ABNORMAL LOAD DETECTION General Machine collision, defective, and damaged cutters cause a large load torque on the servo and spindle motors, compared with normal rapid traverse or cutting feed. This function detects the load torque on the motors and s
- Page 1622. PREPARATIONS FOR OPERATION B–63833EN–1/02 D Parameter setting The following flowcharts explain how to specify parameters for the abnormal load detection function. (1) Servo axis Abnormal load detection function is available. Abnormal load detection No. 2016#0 = 0 function to be used? No Yes No. 2
- Page 163B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Signal Servo axis abnormal load detected signal ABTQSV
- Page 1642. PREPARATIONS FOR OPERATION B–63833EN–1/02 Abnormal load detection ignore signal IUDD1 to IUDD4
[Classification] Input signal [Function] These signals disable the abnormal load detection function for corresponding axes. These signals correspond to the controlled axes. The suffixed number o - Page 165B–63833EN–1/02 2. PREPARATIONS FOR OPERATION #7 #6 #5 #4 #3 #2 #1 #0 2016 ABNTDT [Data type] Bit axis ABNTDT Output of the estimated load torque (for each axis) 0 : Disabled 1 : Enabled This parameter must be specified when using the estimated load torque output function or the abnormal load detecti
- Page 1662. PREPARATIONS FOR OPERATION B–63833EN–1/02 2104 Threshold for abnormal load detection alarm [Data type] Word axis [Unit of data] Torque command unit (Refer to the digital servo operator’s manual for details.) [Valid data range] 0 to 7282 (The maximum motor torque is 7282, regardless of the motor t
- Page 167B–63833EN–1/02 2. PREPARATIONS FOR OPERATION 4248 Spindle load torque monitor constant [Data type] Word axis [Valid data range] 0 to 32767 [Standard setting] Depends of the motor model. This constant is determined by the maximum output torque and inertia of the motor. It is used for observer process
- Page 1682. PREPARATIONS FOR OPERATION B–63833EN–1/02 PMC window function D Reading the load torque The load torque data can be read at the PMC using its window function. data (1) Servo axis [Input data structure] Top address +0 (Function code) 211 2 (Completion code) (Not to be set) 4 (Data length) (Not to
- Page 169B–63833EN–1/02 2. PREPARATIONS FOR OPERATION [Output data structure] Top address + 0 (Function code) 211 2 (Completion code) ? (Refer to the above description about the completion code.) 4 (Data length) L (L = 2*n, where n is the num- ber of specified axes) 6 (Data number) 0 8 (Data attribute) M (M:
- Page 1702. PREPARATIONS FOR OPERATION B–63833EN–1/02 (2) Spindle [Input data structure] Top address +0 (Function code) 211 2 (Completion code) (Not to be set) 4 (Data length) (Not to be set) 6 (Data number) 1 8 (M = 1 to n: Specifies separately (Data attribute) for each axis whether data for the axis is to
- Page 171B–63833EN–1/02 2. PREPARATIONS FOR OPERATION [Output data structure] Top address + 0 (Function code) 211 2 (Completion code) ? (Refer to the above description about the completion code.) 4 (Data length) L (L = 2*n, where n is the num- ber of specified axes) 6 (Data number) 1 8 (Data attribute) M (M:
- Page 1722. PREPARATIONS FOR OPERATION B–63833EN–1/02 2.10 SERVO/SPINDLE MOTOR SPEED DETECTION General The servo axis and spindle motor speeds are monitored. If the speed of an axis exceeds a preset maximum (specified by parameter setting), the corresponding signal is output to a Y address (specified by para
- Page 173B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Signal Motor speed detection function enable signal MSDFON
- Page 1742. PREPARATIONS FOR OPERATION B–63833EN–1/02 Spindle motor speed detection signals DSP1, DSP2
- Page 175B–63833EN–1/02 2. PREPARATIONS FOR OPERATION Signal address #7 #6 #5 #4 #3 #2 #1 #0 G016 MSDFON #7 #6 #5 #4 #3 #2 #1 #0 Y (n+0) Reserved DSV4 DSV3 DSV2 DSV1 Y (n+1) Reserved DSP2 DSP1 Parameter 1890 Servo motor speed for detection NOTE After this parameter has been set, the power must be turned off
- Page 1762. PREPARATIONS FOR OPERATION B–63833EN–1/02 WARNING Be sure to specify a Y address that is not used with a PMC sequence program (ladder). NOTE The motor speed detection signals are inactivate whenever the servo/spindle motor speed detection function is not used, whenever the value 0 or a value beyo
- Page 177B–63833EN–1/02 3. MANUAL OPERATION 3 MANUAL OPERATION 159
- Page 1783. MANUAL OPERATION B–63833EN–1/02 3.1 JOG FEED/ INCREMENTAL FEED General D Jog feed In jog mode, setting a feed axis and direction selection bit to “1” on the machine operator’s panel moves the tool along the selected axis in the selected direction. Manual operation is allowed one axis at a time. 3
- Page 179B–63833EN–1/02 3. MANUAL OPERATION Signal The following signals determine that way the jog feed or incremental feed is executed. Selection Jog feed Incremental feed Mode selection MD1, MD2, MD4, MJ MD1, MD2, MD4, MINC Selection of the axis to move +J1, –J1, +J2, –J2, +J3, –J3, ... Selection of the d
- Page 1803. MANUAL OPERATION B–63833EN–1/02 [Operation] When the jog bit is “1”, the control unit operates as described below. D When jog feed or incremental feed is allowed, the control unit moves the specified axis in the specified direction. D In jog feed, the control unit continues to feed the axis while
- Page 181B–63833EN–1/02 3. MANUAL OPERATION Incremental feed mode (TEACH IN HANDLE mode) Reset +J1 1st axis move +J1 is inef- fective dur- Axis is fed again Move is stopped by ing this resetting after signals have period. turned to “0” once. Manual Feedrate Override Signal *JV0 – *JV15
- Page 1823. MANUAL OPERATION B–63833EN–1/02 Manual rapid traverse selection signal RT
- Page 183B–63833EN–1/02 3. MANUAL OPERATION Parameter #7 #6 #5 #4 #3 #2 #1 #0 1002 JAX [Data type] Bit JAX Number of axes controlled simultaneously in jog feed, manual rapid traverse and manual reference position return 0 : 1 axis 1 : 3 axes #7 #6 #5 #4 #3 #2 #1 #0 1401 RPD [Data type] Bit RPD Manual rapid t
- Page 1843. MANUAL OPERATION B–63833EN–1/02 1424 Manual rapid traverse rate for each axis [Data type] Two–word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 30 – 240000 30 – 100000 Inch machine 0.1 inch/min 30 – 96000 30 – 48
- Page 185B–63833EN–1/02 3. MANUAL OPERATION Warning WARNING For incremental feeding along an axis under diameter programming, the tool moves in units of the diameter. Note NOTE 1 Time constant and method of automatic acceleration/ deceleration for manual rapid traverse are the same as G00 in programmed comma
- Page 1863. MANUAL OPERATION B–63833EN–1/02 3.2 MANUAL HANDLE FEED General In manual handle feed mode, the tool can be incrementally moved by rotating the manual pulse generator. Select the axis along which the tool is to be moved with the handle feed axis selection signal. The minimum distance the tool is m
- Page 187B–63833EN–1/02 3. MANUAL OPERATION Signal Manual Handle Feed Axis Selection Signals [Classification] Input signal D (M series) HS1A – HS1D [Function] Selects the axis of manual handle feed. A set of four code signals, A, B,
- Page 1883. MANUAL OPERATION B–63833EN–1/02 WARNING 1 Because the least input increment is used as the units for manual handle and incremental feed, the same value represents a different distance depending on whether the metric or inch input system is used. 2 For an axis under diameter programming, the tool
- Page 189B–63833EN–1/02 3. MANUAL OPERATION #7 #6 #5 #4 #3 #2 #1 #0 7102 HNGx [Data type] Bit axis HNGx Axis movement direction for rotation direction of manual pulse generator 0: Same in direction 1: Reverse in direction 7110 Number of manual pulse generators used [Data type] Byte [Valid data range] 1, 2, o
- Page 1903. MANUAL OPERATION B–63833EN–1/02 Warning WARNING Rotating the handle quickly with a large magnification such as x100 moves the tool too fast or the tool may not stop immediately after the handle is no longer rotated or the distance the tool moves may not match the graduations on the manual pulse g
- Page 191B–63833EN–1/02 3. MANUAL OPERATION 3.3 MANUAL HANDLE INTERRUPTION General Rotating the manual pulse generator during automatic operation can increase the distance traveled by the amount corresponding to the handle feed. The axis to which the handle interrupt is applied is selected using the manual h
- Page 1923. MANUAL OPERATION B–63833EN–1/02 Warning WARNING The distance travelled by handle interruption is determined according to the amount by which the manual pulse generator is turned and the handle feed magnification (x1, x10, xM, xN). Since the movement is not accelerated or decelerated, it is very d
- Page 193B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT 4 REFERENCE POSITION ESTABLISHMENT 175
- Page 1944. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 4.1 MANUAL REFERENCE POSITION RETURN General The tool is moved in the direction specified by parameter ZMI (bit 5 of No. 1006) setting the feed axis and direction select signal to “1” during manual reference position return mode. Movement will conti
- Page 195B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT (6) Upon confirmation that the current position is at the in–position area, the reference position return end signal (ZP1, ZP2, ZP3,…) and the reference position establishment signal (ZRF1, ZRF2, ZRF3,…) turn to “1”. These steps are repeated for eac
- Page 1964. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 D LDW: Deceleration dog width (mm or inch) TR V R( ) 30 ) T S) ) 4V L TS L DW u 2 60 1000 VR: Rapid traverse (mm/min or inch/min) TR: Rapid traverse time constant (ms) TS: Servo time constant (ms) VL: FL speed for reference position return (mm/min o
- Page 197B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Signal Manual reference position return selection signal ZRN
- Page 1984. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 Feed Axis and Direction For details about this signal, see 3.1, “Feed Axis and Direction Selection Selection Signal Signal”. Only notes on use of reference position return are given, here. NOTE The direction of reference position return is set for e
- Page 199B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Reference position return deceleration signals *DEC1 to *DEC4
[Classification] Input signal [Function] These signals decelerate the feedrate for manual reference position return to a low feedrate (FL). Deceleration signals are provided for ea - Page 2004. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 Reference position establishment signal ZRF1 to ZRF4
[Classification] Output signal [Function] Notify the system that the reference position has been established. A reference position establishment signal is provided for each axis. The number - Page 201B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT #7 #6 #5 #4 #3 #2 #1 #0 1005 ZRNx [Data type] Bit axis ZRNx When a command specifying the movement (except for G28) is issued in automatic operation (MEM, RMT, or MDI) before referencing is completed (after power on) 0 : An alarm is generated. (P/S
- Page 2024. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 [Valid data range] –99999999 to 99999999 Set the coordinate values of the reference positions in the machine coordinate system. #7 #6 #5 #4 #3 #2 #1 #0 1300 LZR [Data type] Bit LZR Checking of stored stroke limit 1 during the time from power–on to t
- Page 203B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT 1821 Reference counter size for each axis [Data type] Two–word axis [Valid data range] 0 to 99999999 Set the size of the reference counter. To set the size of the reference counter, specify the grid interval for the reference position return in the
- Page 2044. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 NOTE When this parameter has been set, the power must be turned off before operation is continued. #7 #6 #5 #4 #3 #2 #1 #0 3003 DEC [Data type] Bit DEC Deceleration signal (*DEC1 to *DEC4) for manual reference position return 0 : Deceleration is app
- Page 205B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Reference item OPERATOR’S MANUAL MANUAL REFERENCE III.3.1 (M series) (B–63844EN) POSITION RETURN Series 0i–B OPERATOR’S MANUAL MANUAL REFERENCE III.3.1 (T series) (B–63834EN) POSITION RETURN OPERATOR’S MANUAL MANUAL REFERENCE III.3.1 (M series) (B–6
- Page 2064. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 4.2 SETTING THE REFERENCE POSITION WITHOUT DOGS General This function moves each axis in the manual continuous feed mode near the reference position. It then sets the reference position in the reference position return mode without the deceleration
- Page 207B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Manual reference position return mode +J1 or –J1 Grid . . . . . . ZP1 ZRF1 Feedrate FL rate The following figure shows the positional relation between the reference position and the point to which the tool is positioned by manual continuous feed. –
- Page 2084. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 1002 DLZ JAX [Data type] Bit JAX Number of axes controlled simultaneously in manual continuous feed, manual rapid traverse and manual reference position return 0 : 1 axis 1 : 3 axes DLZ Function for setting the refe
- Page 209B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT [Data type] Bit axis ZMIx The direction of reference position return and the direction of initial backlash at power–on 0 : Positive direction 1 : Negative direction #7 #6 #5 #4 #3 #2 #1 #0 1201 ZCL [Data type] Bit ZCL Local coordinate system when th
- Page 2104. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 1425 FL rate of the reference position return for each axis [Data type] Word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 6 – 15000 6 – 12000 Inch machine 0.1 inch/
- Page 211B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT 1836 Servo error amount where reference position return is possible [Data type] Byte axis [Unit of data] Detection unit [Valid data range] 0 to 127 This parameter sets the servo error used to enable reference position return in manual reference posi
- Page 2124. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 Alarm and message Number Message Description 090 REFERENCE RETURN 1. The reference position return can- INCOMPLETE not be performed normally because the reference position return start point is too close to the reference position or the speed is too
- Page 213B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT 4.3 REFERENCE POSITION SHIFT General When reference position return is performed using the grid method, the reference position can be shifted by a parameter–set distance without having to move the deceleration dog. This function is enabled by settin
- Page 2144. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 (3) Perform reference position return again. The tool stops when it reaches the reference position. Direction of reference position return Deceleration dog | | | | | ↑ ↑ Grid point Reference position (stop position) Parameter #7 #6 #5 #4 #3 #2 #1 #0
- Page 215B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Alarm and message D Diagnostic display 0302 Distance from the position where the deceleration dog is turned off to the first grid point [Data type] Two–word axis [Unit of data] 0.001 mm (metric output), 0.0001 inch (inch output) [Valid data range] –
- Page 2164. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 4.4 REFERENCE POSITION RETURN General The G28 command positions the tool to the reference position, via the specified intermediate point, then sets the completion signal for reference position return (see Section 4.1) to 1. The reference position mu
- Page 217B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Alarm and message Number Message Description 405 SERVO ALARM: Position control system fault. Due to (WRONG ZRN) an CNC or servo system fault in the reference position return, there is a possibility that reference position re- turn could not be execu
- Page 2184. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 4.5 2ND REFERENCE POSITION RETURN/3RD, 4TH REFERENCE POSITION RETURN General The G30 command positions the tool to the 2nd, 3rd, or 4th reference position, via the specified intermediate point. It then sets the completion signal for 2nd, 3rd, or 4th
- Page 219B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT ZP 2 1 1 : Return end signal for the first axis 2 : Return end signal for the second axis 3 : Return end signal for the third axis : : 2 : Second reference position return 3 : Third reference position return 4 : Fourth reference position return [Out
- Page 2204. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 Alarm and message Number Message Description 046 ILLEGAL REFERENCE RE- Other than P2, P3 and P4 are commanded TURN COMMAND for 2nd, 3rd and 4th reference position re- turn command. Correct program. Caution CAUTION 1 If the G30 command is issued in m
- Page 221B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT 4.6 BUTT–TYPE REFERENCE POSITION SETTING General This function automates the procedure of butting the tool against a mechanical stopper on an axis to set a reference position. The purpose of this function is to eliminate the variations in reference
- Page 2224. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 Cycle operation When no reference position has been set (APZx, bit 4 of parameter No. 1815, is 0), operations (A) to (E), below, are performed automatically to set a reference position. Mechanical stopper Current position (A)The tool is moved along
- Page 223B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Mechanical stopper The direction, feedrate, and torque are all specified with parameters. (E)After the tool strikes the mechanical stopper end on the axis, the tool is withdrawn in the direction opposite to the butting direction, along the axis for
- Page 2244. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 After the reference When the reference position has already been set (when APZx, bit 4 of position is set parameter No. 1815, is 1), performing butt–type reference position setting causes the tool to be positioned to the reference position at the ra
- Page 225B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT Signal Torque limit reach signals for butt–type reference position setting CLRCH1 to CLRCH4
[Classification] Output signal [Function] These signals are used to post notification of the torque limit having been reached for each corresponding a - Page 2264. REFERENCE POSITION ESTABLISHMENT B–63833EN–1/02 [Valid data range] –99999999 to 99999999 When the butt–type reference position setting function is used, this parameter sets a distance on an axis, along which withdrawal is performed after the mechanical stopper is hit (distance from the mechanical
- Page 227B–63833EN–1/02 4. REFERENCE POSITION ESTABLISHMENT When the butt–type reference position setting function is used, this parameter sets the feedrate used to hit the stopper on an axis for a second time. 7185 Withdrawal feedrate (common to the first and second butting operations) in butt–type referenc
- Page 2285. AUTOMATIC OPERATION B–63833EN–1/02 5 AUTOMATIC OPERATION 210
- Page 229B–63833EN–1/02 5. AUTOMATIC OPERATION 5.1 CYCLE START/ FEED HOLD General D Start of automatic When automatic operation start signal ST is set to 1 then 0 while the CNC operation (cycle start) is in memory (MEM) mode, DNC operation mode (RMT), or manual data input (MDI) mode, the CNC enters the autom
- Page 2305. AUTOMATIC OPERATION B–63833EN–1/02 D Halt of automatic When the feed hold signal *SP is set to 0 during automatic operation, the operation (feed hold) CNC enters the feed hold state and stops operation. At the same time, cycle start lamp signal STL is set to 0 and feed hold lamp signal SPL is set
- Page 231B–63833EN–1/02 5. AUTOMATIC OPERATION Signal Cycle start signal ST
- Page 2325. AUTOMATIC OPERATION B–63833EN–1/02 Feed hold lamp signal SPL
- Page 233B–63833EN–1/02 5. AUTOMATIC OPERATION Alarm and message D Self–diagnosis During automatic operation, the machine may sometimes show no information movement while no alarm is detected. In that case, the CNC may be performing processing or waiting for the occurrence of an event. The state of the CNC c
- Page 2345. AUTOMATIC OPERATION B–63833EN–1/02 5.2 RESET AND REWIND General The CNC is reset and enters the reset state in the following cases: 1. When the emergency stop signal (*ESP) is set to 0 2. When the external reset signal (ERS) is set to 1 3. When the reset and rewind signal (RRW) is set to 1 4. Whe
- Page 235B–63833EN–1/02 5. AUTOMATIC OPERATION The following parameters are also used to select how to handle processing for CNC data when the CNC is reset. S Bit 7 (MCL) of parameter No. 3203 Whether programs created in MDI mode are erased or stored S Bit 6 (CCV) of parameter No. 6001 Whether custom macro v
- Page 2365. AUTOMATIC OPERATION B–63833EN–1/02 Resetting signal RST
- Page 237B–63833EN–1/02 5. AUTOMATIC OPERATION 3017 Output time of reset signal RST [Data type] Byte [Unit of data] 16 ms [Valid data range] 0 to 255 To extend the output time of reset signal RST, the time to be added is specified in this parameter. RST signal output time = time required for reset + paramete
- Page 2385. AUTOMATIC OPERATION B–63833EN–1/02 Reference item STATUS WHEN TURNING OPERATOR’S MANUAL POWER ON, WHEN APPENDIX E (M series) (B–63844EN) CLEAR AND WHEN RESET Series 0i–B STATUS WHEN TURNING OPERATOR’S MANUAL POWER ON, WHEN APPENDIX E (T series) (B–63834EN) CLEAR AND WHEN RESET STATUS WHEN TURNING
- Page 239B–63833EN–1/02 5. AUTOMATIC OPERATION 5.3 Before machining is started, the automatic running check can be executed. It checks whether the created program can operate the machine TESTING A as desired. This check can be accomplished by running the machine or PROGRAM viewing the position display change
- Page 2405. AUTOMATIC OPERATION B–63833EN–1/02 All–axis machine lock check signal MMLK
- Page 241B–63833EN–1/02 5. AUTOMATIC OPERATION Note NOTE 1 Automatic operation in the machine lock state (M, S, T, and B commands) Machine lock applies only to move commands along controlled axes. Updating modal G codes or setting a coordinate system is performed normally. M, S, T, and B (2nd auxilialy funct
- Page 2425. AUTOMATIC OPERATION B–63833EN–1/02 5.3.2 Dry Run General Dry run is valid only for automatic operation. The tool is moved at a constant feedrate(*1) regardless of the feedrate specified in the program. This function is used, for example, to check the movement of the tool without a workpiece. CAUT
- Page 243B–63833EN–1/02 5. AUTOMATIC OPERATION Dry run check signal MDRN
- Page 2445. AUTOMATIC OPERATION B–63833EN–1/02 1420 Rapid traverse rate for each axis [Data type] Two–word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 30 – 240000 6 – 100000 Inch machine 0.1 inch/min 30 – 96000 6 – 48000 Ro
- Page 245B–63833EN–1/02 5. AUTOMATIC OPERATION 5.3.3 Single Block General Single block operation is valid only for automatic operation. When the single block signal (SBK) is set to 1 during automatic operation, the CNC enters the automatic operation stop state after executing the current block. In subsequent
- Page 2465. AUTOMATIC OPERATION B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G046 SBK F004 MSBK Parameter #7 #6 #5 #4 #3 #2 #1 #0 6000 SBV SBM [Data type] Bit SBM Custom macro statement 0: Not stop the single block 1: Stops the single block If you want to disable the single blocks in custom macro st
- Page 247B–63833EN–1/02 5. AUTOMATIC OPERATION Reference item OPERATOR’S MANUAL III.5.5 Single block (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.5.5 Single block (T series) (B–63834EN) OPERATOR’S MANUAL III.5.5 Single block (M series) (B–63864EN) Series 0i Mate–B OPERATOR’S MANUAL III.5.5 Single
- Page 2485. AUTOMATIC OPERATION B–63833EN–1/02 5.4 MANUAL ABSOLUTE ON/OFF General This function selects whether the movement of the tool with manual operation (such as jog feed and manual handle feed) is counted for calculating the current position in the workpiece coordinate system. A check signal is also o
- Page 249B–63833EN–1/02 5. AUTOMATIC OPERATION When manual absolute The manual move amount is not counted to the present position on the turns off (manual workpiece coordinate system. The present position display on the CRT absolute signal includes the manual move amount. The display is reset to the initial
- Page 2505. AUTOMATIC OPERATION B–63833EN–1/02 Manual absolute check signal MABSM [Classification] Output signal
- Page 251B–63833EN–1/02 5. AUTOMATIC OPERATION 5.5 OPTIONAL BLOCK SKIP/ADDITION OF OPTIONAL BLOCK SKIP General When a slash followed by a number (/n, where n = 1 to 9) is specified at the head of a block, and optional block skip signals BDT1 to BDT9 are set to 1 during automatic operation, the information co
- Page 2525. AUTOMATIC OPERATION B–63833EN–1/02 2. When BDTn is set to 1 while the CNC is reading a block containing /n, the block is not ignored. BDTn ”1” ”0” Reading by CNC ³ ...; /n N123 X100. Y200. ; N234 .... Not ignored 3. When BDTn, currently set to 1, is set to 0 while the CNC is reading a block conta
- Page 253B–63833EN–1/02 5. AUTOMATIC OPERATION Optional block skip check signals MBDT1
[Classification] Output signal [Function] Notify the PMC of the states of the optional block skip signals BDT1 to BDT9. Nine signals are provided, corresponding to the nine optional block ski - Page 2545. AUTOMATIC OPERATION B–63833EN–1/02 Reference item OPERATOR’S MANUAL II.12.2 Program section configuration (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.12.2 Program section configuration (T series) (B–63834EN) OPERATOR’S MANUAL II.12.2 Program section configuration (M series) (B–63864EN
- Page 255B–63833EN–1/02 5. AUTOMATIC OPERATION 5.6 SEQUENCE NUMBER COMPARISON AND STOP General During program execution, this function causes a single block stop right after a block with a specified sequence number is executed. To use this function, first specify the program number (1 to 9999) of a program t
- Page 2565. AUTOMATIC OPERATION B–63833EN–1/02 5.7 PROGRAM RESTART General A program may be restarted at a block by specifying the sequence number of the block, after automatic operation is stopped because of a broken tool or for holidays. This function can also be used as a high–speed program check function
- Page 257B–63833EN–1/02 5. AUTOMATIC OPERATION Signal address #7 #6 #5 #4 #3 #2 #1 #0 G006 SRN F002 SRNMV Parameter 7310 Movement sequence to program restart position This parameter can be set at the “Setting Screen.” [Data type] Byte axis [Valid data range] 1 to no. of controlled axes This parameter sets th
- Page 2585. AUTOMATIC OPERATION B–63833EN–1/02 Warning WARNING As a rule, the tool cannot be returned to a correct position under the following conditions. Special care must be taken in the following cases since none of them cause an alarm: ⋅ Manual operation is performed when the manual absolute mode is OFF
- Page 259B–63833EN–1/02 5. AUTOMATIC OPERATION 5.8 EXACT STOP/ EXACT STOP MODE/ TAPPING MODE/ CUTTING MODE (M SERIES) General NC commands can be used to control a feedrate in continuous cutting feed blocks as described below. D Exact stop (G09) The tool is decelerated in a block specifying G09, and an in–pos
- Page 2605. AUTOMATIC OPERATION B–63833EN–1/02 Reference item Exact Stop (G09, G61) OPERATOR’S MANUAL Series 0i–B II.5.4.1 Cutting Mode (G64) (M series) (B–63844EN) Tapping Mode (G63) Exact Stop (G09, G61) OPERATOR’S MANUAL Series 0i Mate–B II.5.4.1 Cutting Mode (G64) (M series) (B–63864EN) Tapping Mode (G63
- Page 261B–63833EN–1/02 5. AUTOMATIC OPERATION 5.9 DNC OPERATION General By starting automatic operation during the DNC operation mode (RMT), it is possible to perform machining (DNC operation) while a program is being read from the reader/puncher interface. It is possible to select files (programs) saved in
- Page 2625. AUTOMATIC OPERATION B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G043 DNCI #7 #6 #5 #4 #3 #2 #1 #0 F003 MRMT Parameter #7 #6 #5 #4 #3 #2 #1 #0 0100 ND3 This parameter can be set at the “Setting Screen.” [Data type] Bit ND3 In DNC operation, a program is: 0 : Read block by block. (A “DC3”
- Page 263B–63833EN–1/02 5. AUTOMATIC OPERATION Reference item OPERATOR’S MANUAL III.4.5 SCHEDULING FUNCTION (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.4.4 SCHEDULING FUNCTION (T series) (B–63834EN) OPERATOR’S MANUAL III.4.5 SCHEDULING FUNCTION (M series) (B–63864EN) Series 0i Mate–B OPERATOR’S
- Page 2645. AUTOMATIC OPERATION B–63833EN–1/02 5.10 MANUAL INTERVENTION AND RETURN General If the tool movement along the axes is stopped by a feed hold during automatic operation, then restarted after manual intervention such as tool exchange, the tool moves back to the point of intervention before automati
- Page 265B–63833EN–1/02 5. AUTOMATIC OPERATION 5.11 RETRACTION FOR RIGID TAPPING (M SERIES) General When rigid tapping is stopped, either as a result of an emergency stop or a reset, the tap may cut into the workpiece. The tap can subsequently be drawn out by using a PMC signal. This function automatically s
- Page 2665. AUTOMATIC OPERATION B–63833EN–1/02 (4) Resume Once rigid tapping retraction has been stopped, it can be resumed by performing the same operation as that used for starting rigid tapping retraction. If rigid tapping retraction has been completed, however, the start operation does not restart rigid
- Page 267B–63833EN–1/02 5. AUTOMATIC OPERATION Time chart for stopping tapping retraction Tapping retraction start signal RTNT Spindle enable signal ENB Rigid tapping signal RGTAP Spindle excitation Retract movement When tapping retraction is stopped, spindle enable signal is set to 0, in the same way as for
- Page 2685. AUTOMATIC OPERATION B–63833EN–1/02 3. The override value (parameter No. 5381) for rigid tapping retraction is ignored. Example: D Machining program –––––––––– M29 S1000 ; G84 X20. Y20. R–10. Z–30. F500 ; X50. Y50. ; X100. Y100. ; G80 –––––––––– D Retraction program –––––––––– G30 P99 M29 S1000 ;
- Page 269B–63833EN–1/02 5. AUTOMATIC OPERATION Parameter #7 #6 #5 #4 #3 #2 #1 #0 5200 DOV [Data type] Bit DOV For tool extraction during rigid tapping, override is: 0 : Disabled. 1 : Enabled. #7 #6 #5 #4 #3 #2 #1 #0 5202 RG3 [Data type] Bit RG3 Rigid tapping retraction is performed using: 0 : Input signal RT
- Page 2705. AUTOMATIC OPERATION B–63833EN–1/02 Caution CAUTION 1 If rigid tapping is stopped as a result of an emergency stop, the position on the tapping axis (Z–axis) is maintained but the spindle position is lost. In such a case, therefore, the positional relationship between the spindle and tapping axis
- Page 271B–63833EN–1/02 5. AUTOMATIC OPERATION Reference item OPERATOR’S MANUAL II.13.2 Rigid tapping (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.13.6 Rigid tapping (T series) (B–63834EN) OPERATOR’S MANUAL Series 0i Mate–B II.13.2 Rigid tapping (M series) (B–63864EN) CONNECTION MANUAL (This manua
- Page 2726. INTERPOLATION FUNCTION B–63833EN–1/02 6 INTERPOLATION FUNCTION 254
- Page 273B–63833EN–1/02 6. INTERPOLATION FUNCTION 6.1 POSITIONING General The G00 command moves a tool to the position in the workpiece system specified with an absolute or an incremental command at a rapid traverse rate. In the absolute command, coordinate value of the end point is programmed. In the increm
- Page 2746. INTERPOLATION FUNCTION B–63833EN–1/02 1420 Rapid traverse rate for each axis [Data type] Two–word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 30 – 240000 30 – 100000 Inch machine 0.1 inch/min 30 – 96000 30 – 480
- Page 275B–63833EN–1/02 6. INTERPOLATION FUNCTION 6.2 LINEAR INTERPOLATION General Tools can move along a line A tools move along a line to the specified position at the feedrate specified in F. The feedrate specified in F is effective until a new value is specified. It need not be specified for each block.
- Page 2766. INTERPOLATION FUNCTION B–63833EN–1/02 Parameter 1411 Cutting feedrate when the power is turned on This parameter can be set in “Setting screen”. [Data type] Word [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 6 – 32767
- Page 277B–63833EN–1/02 6. INTERPOLATION FUNCTION NOTE 1 This parameter is effective only in linear and circular interpolation. In polar coordinate and cylindrical, the maximum feedrate for all axes specified in parameter No. 1422 is effective. 2 If the setting for each axis is 0, the maximum feedrate specif
- Page 2786. INTERPOLATION FUNCTION B–63833EN–1/02 6.3 CIRCULAR INTERPOLATION General The command below can move a tool along a circular arc in the defined plane. “Clockwise”(G02) and “counterclockwise”(G03) on the XpYp plane (ZpXp plane or YpZp plane) are defined when the XpYp plane is viewed in the positive
- Page 279B–63833EN–1/02 6. INTERPOLATION FUNCTION The distance between an arc and the center of a circle that contains the arc can be specified using the radius, R, of the circle instead of I, J, and K. In this case, one arc is less than 180_, and the other is more than 180_ are considered. For T series, an
- Page 2806. INTERPOLATION FUNCTION B–63833EN–1/02 (Example) (M series) For arc (1) (less than 180_) G91 G02 X60.0 Y20.0 R50.0 F300.0 ; For arc (2) (greater than 180_) G91 G02 X60.0 Y20.0 R–50.0 F300.0 ; (2) r=50mm End point (1) Start point r=50mm Y X NOTE 1 Specifying an arc center with addresses I, K, and J
- Page 281B–63833EN–1/02 6. INTERPOLATION FUNCTION The feedrate in circular interpolation is equal to the feedrate specified by the F code, and the feedrate along the arc (the tangential feedrate of the arc) is controlled to be the specified feedrate. The error between the specified feedrate and the actual to
- Page 2826. INTERPOLATION FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3402 G19 G18 [Data type] Bit G18 and G19 Plane selected when power is turned on or when the control is cleared G19 G18 G17, G18 or G19 mode 0 0 G17 mode (plane XY) 0 1 G18 mode (plane ZX) 1 0 G19 mode (plane YZ) 3410 Tolerance of arc r
- Page 283B–63833EN–1/02 6. INTERPOLATION FUNCTION Number Message Description 023 ILLEGAL RADIUS In circular interpolation by radius des- COMMAND ignation, negative value was com- (T series) manded for address R. Modify the program. 025 CANNOT COMMAND F0 F0 (rapid traverse) was instructed by IN G02/G03 F1 –di
- Page 2846. INTERPOLATION FUNCTION B–63833EN–1/02 6.4 THREAD CUTTING 6.4.1 Thread Cutting General Tool movement can be synchronized with spindle rotation when cutting threads. The spindle speed is continuously read through the position coder attached to the spindle. Then, it is converted to a cutting feedrat
- Page 285B–63833EN–1/02 6. INTERPOLATION FUNCTION Signal Thread cutting signal THRD
- Page 2866. INTERPOLATION FUNCTION B–63833EN–1/02 Checking the spindle speed arrival signal before starting threading #7 #6 #5 #4 #3 #2 #1 #0 3708 SAT SAR SAR [Data type] Bit SAR: The spindle speed arrival signal is: 0 : Not checked 1 : Checked SAT: Check of the spindle speed arrival signal at the start of e
- Page 287B–63833EN–1/02 6. INTERPOLATION FUNCTION Setting the FL feedrate for the thread cutting cycle 1627 FL rate of exponential acceleration /deceleration in the thread cutting cycle for each axis [Data type] Word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A,
- Page 2886. INTERPOLATION FUNCTION B–63833EN–1/02 Setting the finishing allowance for the multiple repetitive canned cycle G76 5141 Finishing allowance in the multiple repetitive canned cycle G76 [Data type] Two–word [Unit of data] Increment system IS–A IS–B IS–C Unit Metric input 0.01 0.001 0.0001 mm Inch i
- Page 289B–63833EN–1/02 6. INTERPOLATION FUNCTION Warning WARNING During threading, stopping feed without stopping the spindle is dangerous because the cutting depth will abruptly increase. Feed hold is, therefore, disabled during threading. If attempted during threading, feed stops in the same way as single
- Page 2906. INTERPOLATION FUNCTION B–63833EN–1/02 Reference item OPERATOR’S MANUAL II.4.7 THREAD CUTTING (M series) (B–63844EN) CONSTANT LEAD THREAD II.4.6 CUTTING Series 0i–B VARIABLE LEAD THREAD II.4.7 OPERATOR’S MANUAL CUTTING (T series) (B–63834EN) CONTINUOUS THREAD CUT- II.4.8 TING II.4.9 MULTIPLE THREA
- Page 291B–63833EN–1/02 6. INTERPOLATION FUNCTION 6.4.2 Thread Cutting Cycle Retract (T series) General When the automatic operation stop signal *SP
- Page 2926. INTERPOLATION FUNCTION B–63833EN–1/02 Caution CAUTION While the tool is retracting, automatic operation stop signal *SP
- Page 293B–63833EN–1/02 6. INTERPOLATION FUNCTION 6.5 SINGLE DIRECTION POSITIONING General For accurate positioning without play of the machine (lost motion), positioning is performed in one direction finally. Overrun distance Start point Start point Temporary stop End point + Example where positioning is pe
- Page 2946. INTERPOLATION FUNCTION B–63833EN–1/02 D Overview of operation X Overrun distance in the Z–axis direction Overrun distance in the X–axis direction Programmed end point Z Programmed start point In the case of positioning of non–linear interpolation type (bit 1 (LRP) of parameter No. 1401 = 0) As sh
- Page 295B–63833EN–1/02 6. INTERPOLATION FUNCTION Parameter #7 #6 #5 #4 #3 #2 #1 #0 5431 PDI MDL [Data type] Bit MDL Specifies whether the G code for single direction positioning (G60) is included in one–shot G codes (00 group) or modal G codes (01 group) 0: One–shot G codes (00 group) 1: Modal G codes (01 g
- Page 2966. INTERPOLATION FUNCTION B–63833EN–1/02 Notes 1. Single direction positioning is not performed along an axis for which no overrun distance is set in parameter No. 5440. 2. Single direction positioning is not performed along an axis for which travel distance 0 is specified. 3. The mirror image funct
- Page 297B–63833EN–1/02 6. INTERPOLATION FUNCTION The direction of the compensation command Xa is determined by the inclination angle q of the angular axis and the direction of the move command Yp for the orthogonal axis. When tan q is plus, the direction of the move command for the angular axis is opposite
- Page 2986. INTERPOLATION FUNCTION B–63833EN–1/02 +X (orthogonal axis) X–axis: Compensation in the plus direction Move command in the minus direction Y–axis: Positioning in the +Y (angular axis) minus direction Actual move coordinate system q (inclination angle) Program coordinate system Move command in the
- Page 299B–63833EN–1/02 6. INTERPOLATION FUNCTION Program coordinate system +X (orthogonal axis) Y–axis: Positioning in the minus direction X–axis: Compensation in the minus direction Move command in the minus direction q (inclination angle) +Y (angular axis) Actual move coordinate system Move command in the
- Page 3006. INTERPOLATION FUNCTION B–63833EN–1/02 6.6 HELICAL INTERPOLATION General Helical interpolation is enabled by specifying up to two other axes which move synchronously with the circular interpolation by circular commands. The command method is to simply add one or two move command axes which are not
- Page 301B–63833EN–1/02 6. INTERPOLATION FUNCTION
When HFC is 0 No. 1430: Maximum cutting feedrate for each axis Since the cutting feedrate for the arc is clamped to the above parameter value, the feedrate along the linear axis is clamped to the smaller parameter value. Example - Page 3026. INTERPOLATION FUNCTION B–63833EN–1/02 6.7 POLAR COORDINATE INTERPOLATION General Polar coordinate interpolation is a function that exercises contour control in converting a command programmed in a Cartesian coordinate system to the movement of a linear axis (movement of a tool) and the movement o
- Page 303B–63833EN–1/02 6. INTERPOLATION FUNCTION Parameter 1422 Maximum cutting feedrate for all axes [Data type] Two–word [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 6 – 240000 6 – 100000 Inch machine 0.1 inch/min 6 – 96000 6
- Page 3046. INTERPOLATION FUNCTION B–63833EN–1/02 Alarm and message No. Message Description 145 ILLEGAL CONDITIONS The conditions are incorrect when the polar IN POLAR COORDINATE coordinate interpolation starts or it is can- INTERPOLATION celed. 1) In modes other than G40, G12.1/G13.1 was specified. 2) An er
- Page 305B–63833EN–1/02 6. INTERPOLATION FUNCTION 6.8 CYLINDRICAL INTERPOLATION General The amount of travel of a rotary axis specified by an angle is internally converted to a distance of a linear axis along the outer surface so that linear interpolation or circular interpolation can be performed with anoth
- Page 3066. INTERPOLATION FUNCTION B–63833EN–1/02 1022 Setting of each axis in the basic coordinate system [Data type] Byte axis To determine the following planes used for circular interpolation, cutter compensation C (for the M series), tool nose radius compensation (for the T series), etc., each control ax
- Page 307B–63833EN–1/02 6. INTERPOLATION FUNCTION Reference item OPERATOR’S MANUAL II.4.9 Cylindrical Interpolation (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.4.6 Cylindrical Interpolation (T series) (B–63834EN) OPERATOR’S MANUAL Series 0i Mate–B II.4.4 Cylindrical Interpolation (M series) (B–63
- Page 3086. INTERPOLATION FUNCTION B–63833EN–1/02 6.9 Polygonal turning means machining a polygonal figure by rotating the workpiece and tool at a certain ratio. POLYGONAL TURNING (T SERIES) Workpiece Workpiece Tool Fig. 6.9 (a) Polygonal turning By changing conditions which are rotation ratio of workpiece a
- Page 309B–63833EN–1/02 6. INTERPOLATION FUNCTION 6.9.1 Polygonal Turning General One of the axes (servo axes) controlled by the CNC is assigned as a tool rotation axis. Either serial spindle or analog spindle can be used as a workpiece axis (spindle). Polygonal turning using a servo axis is detailed in the
- Page 3106. INTERPOLATION FUNCTION B–63833EN–1/02 (With the above setting, the reference counter capacity is 36000.) Parameter No. 1820 = 2 (CMR) Parameter No. 1821 = 36000 (reference counter capacity) Parameter No. 2084 = 36 (DMR numerator) Parameter No. 2085 = 1000 (DMR denominator) For the other servo par
- Page 311B–63833EN–1/02 6. INTERPOLATION FUNCTION 360 No. 1420 = 72000 (= 2000 ) 10 Also specify other feedrates in 10 degrees/min units. D Commands from the NC program When the machine is not performing polygonal turning, the machining program can issue move commands to the polygon axis. Such commands can b
- Page 3126. INTERPOLATION FUNCTION B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 7600 PLZ [Data type] Bit PLZ Synchronous axis using G28 command 0: Returns to the reference position in the same sequence as the manual reference position return. 1: Returns to the reference position by positioning at a rapid
- Page 313B–63833EN–1/02 6. INTERPOLATION FUNCTION Alarm and message Number Message Description 217 DUPLICATE G251 (COM- G51.2 (or G251) is further comman- MANDS) ded in the polygonal turning mode. Modify the program. 218 NOT FOUND P/Q COM- P or Q is not commanded in the MAND IN G251 G51.2 (or the G251) block
- Page 3146. INTERPOLATION FUNCTION B–63833EN–1/02 6.10 NORMAL DIRECTION CONTROL (M SERIES) General When a tool with a rotation axis (C–axis) is moved in the XY plane during cutting, the normal direction control function can control the tool so that the C–axis is always perpendicular to the tool path (Fig. 6.
- Page 315B–63833EN–1/02 6. INTERPOLATION FUNCTION [Data type] Bit axis [Valid data range] ROTx, ROSx Setting linear or rotation axis ROSx ROTx Description 0 0 Linear axis @ Inch/metric conversion is done. @ All coordinate values are linear axis type. (Not rounded in 0 to 360_) @ Stored pitch error compensati
- Page 3166. INTERPOLATION FUNCTION B–63833EN–1/02 5482 Limit value that ignores the rotation insertion of normal direction control axis [Data type] Two–word [Unit of data] Increment system IS–A IS–B IS–C Unit Rotation axis 0.01 0.001 0.0001 deg [Valid data range] 1 to 99999999 The rotation block of a normal
- Page 317B–63833EN–1/02 6. INTERPOLATION FUNCTION #7 #6 #5 #4 #3 #2 #1 #0 5484 CTI SDC [Data type] Bit SDC In normal direction control: 0 : A C–axis movement is automatically inserted between blocks so that the C–axis is directed at right angles to the direction of motion at the start point of each block. (A
- Page 3186. INTERPOLATION FUNCTION B–63833EN–1/02 NOTE When this parameter is set to 1, no interference check is made in cutter compensation C. 5485 Limit imposed on the insertion of a single block for rotation about the normal direction control axis [Data type] 2–word [Unit of data] Increment system IS–A IS
- Page 319B–63833EN–1/02 6. INTERPOLATION FUNCTION NOTE To specify the maximum cutting feedrate for each axis, use parameter No. 1430 instead. Reference item OPERATOR’S MANUAL Series 0i–B II.14.9 Normal Direction Control (M series) (B–63844EN) 301
- Page 3206. INTERPOLATION FUNCTION B–63833EN–1/02 6.11 LINEAR INTERPOLATION (G28, G30, G53) General When positioning operation of linear interpolation type is specified (bit 1 (LRP) of parameter No. 1401 = 1), the following operations can also be set as operations of linear interpolation type by setting bit
- Page 321B–63833EN–1/02 6. INTERPOLATION FUNCTION Note 1 Manual intervention Positioning of non–linear interpolation type is performed if the automatic operation stop state is set by feed hold or mode switching during movement then the subsequent operation of the program is performed after the machine is mov
- Page 3227. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7 FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL 304
- Page 3237. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.1 The feed functions control the feedrate of the tool. The following two feed functions are available: FEEDRATE CONTROL 1. Rapid traverse When the positioning command (G00) is specified, the tool moves at a rapid traverse rat
- Page 3247. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 NOTE 1 The rapid traverse in automatic operation includes all rapid traverses in canned cycle positioning, automatic reference point return, etc., as well as the move command G00. The manual rapid traverse also includes the rap
- Page 3257. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 1424 Manual rapid traverse rate for each axis [Data type] Two–word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 30 – 240000 30 – 100000 Inch m
- Page 3267. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.2 Cutting Feedrate Clamp General A common upper limit can be set on the cutting feedrate along each axis with parameter No. 1422. If an actual cutting feedrate (with an override applied) exceeds a specified upper limit, it
- Page 3277. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 1430 Maximum cutting feedrate for each axis [Data type] Two–word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min 6 – 240000 6 – 100000 Inch machi
- Page 3287. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.3 Feed Per Minute General D Feed per minute (G94) After specifying G94 (G98 for T series) (in the feed per minute mode), the amount of feed of the tool per minute is specified by setting a number after F. G94 (G98 for T ser
- Page 3297. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Parameter #7 #6 #5 #4 #3 #2 #1 #0 1403 MIF [Data type] Bit MIF Cutting feedrates at feed per minute is specified by F commands 0 : In units of 1 mm/min for millimeter machines or 0.01 inches/min for inch machines. 1 : In unit o
- Page 3307. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3402 FPM [Data type] Bit FPM When the power is turned on: 0 : Feed per revolution mode is entered. 1 : Feed per minute mode is entered. Alarm and message Number Message Description 011 NO FEEDRATE COM- F
- Page 3317. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.1.4 Feed Per Revolution/ Manual Feed Per Revolution General D Feed per revolution After specifying G95 (G99 for T series) (in the feed per revolution mode), the amount of feed of the tool per spindle revolution is to be direc
- Page 3327. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 1423 Feedrate in jog feed for each axis [Data type] Word axis When JRV, bit 4 of parameter No. 1402, is set to 1 (feed per revolution) in T series, specify a feedrate in jog feed (feed per revolution) with an override of 100% a
- Page 3337. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.1.5 F1-digit Feed (M series) General When a one–digit number from 1 to 9 is specified after F, the feedrate set for that number in a parameter (Nos. 1451 to 1459) is used. When F0 is specified, the rapid traverse rate is appl
- Page 3347. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Parameter 1450 Number of revolution of manual pulse generator to reach maximum feedrate [Data type] Byte [Valid data range] 1 to 127 Set the constant that determines the change in feedrate as the manual pulse generator is rotat
- Page 3357. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 1460 Upper limit of feedrate for the F1–digit feed command (F1 to F4) 1461 Upper limit of feedrate for the F1-digit feed command (F5 to F9) [Data type] Two–word [Unit of data] Valid data range Increment system Unit of data [Val
- Page 3367. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.6 Override 7.1.6.1 Rapid traverse override General An override of four steps (F0, 25%, 50%, and 100%) can be applied to the rapid traverse rate. F0 is set by a parameter (No. 1421). Also, 1% rapid traverse override select s
- Page 3377. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Signal Rapid traverse override signal ROV1,ROV2
- Page 3387. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 ⋅ Signals *HROV0 to *HROV6 are inverted signals. To set an override value of 1%, set signals *HROV0 to *HROV6 to 1111110, which corresponds to a binary code of 0000001. Signal address #7 #6 #5 #4 #3 #2 #1 #0 G014 ROV2 ROV1 G096
- Page 3397. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Reference item OPERATOR’S MANUAL III.5.3 Rapid traverse override (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.5.3 Rapid traverse override (T series) (B–63834EN) OPERATOR’S MANUAL III.5.3 Rapid traverse override (M s
- Page 3407. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Signal Feedrate Override signal *FV0 to *FV7
[Classification] Input signal [Function] These signals override the cutting feedrate. Eight binary code signals correspond to override values as follows: 7 Override value = Σ - Page 3417. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Reference item OPERATOR’S MANUAL II.5.3 Cutting feed (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.5.3 Cutting feed (T series) (B–63834EN) OPERATOR’S MANUAL II.5.3 Cutting feed (M series) (B–63864EN) Series 0i Mate–B
- Page 3427. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.7 Automatic Corner Override (M series) General D Inner corner automatic When G62 is specified, and the tool path with cutter compensation override applied forms an inner corner, the feedrate is automatically overridden at b
- Page 3437. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL D Override value An override value is set with parameter No. 1712. An override value is valid even for dry run and F1–digit feed specification. In the feed per minute mode, the actual feedrate is as follows: F × (inner corner a
- Page 3447. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 In circular cutting with an inward offset, the actual feedrate for a specified feedrate (F) becomes as follows: Rc Rc: Radius of the path of the cutter’s center F Rp: Programmed radius Rp As the actual feedrate becomes the valu
- Page 3457. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 1713 Distance Le from the starting point in inner corner automatic override [Data type] Word [Unit of data] Increment system IS–A IS–B IS–C Unit Input in mm 1 0.1 0.01 mm Input in inches 0.1 0.01 0.001 inch [Valid data range] 0
- Page 3467. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.8 External Deceleration General These signals decelerate the feedrate of the control axes down to the speed which has been set by parameter No. 1426 and 1427. Signal External deceleration signal *+ED1 to *+ED4
*–ED1 t - Page 3477. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Parameter #7 #6 #5 #4 #3 #2 #1 #0 1005 EDMx EDPx [Data type] Bit axis EDPx External deceleration signal in the positive direction for each axis 0 : Valid only for rapid traverse 1 : Valid for rapid traverse and cutting feed EDM
- Page 3487. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.9 Feedrate Clamping by Arc Radius (M series) General When an arc is cut at a high speed in circular interpolation, a radial error exists between the actual tool path and the programmed arc. An approximation of this error ca
- Page 3497. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL When a given arc radius R and the maximum permissible speed V for that arc radius are set as parameters, the maximum permissible speed v for an arc with a programmed radius r can be obtained from expression 3. Then, if a specif
- Page 3507. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Expressions 1, 2, and 4 are approximate expressions. This means that, as the arc radius becomes smaller, the approximate precision lowers. Therefore, even when the feedrate is clamped to the maximum permissible speed v obtained
- Page 3517. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.1.10 Automatic Corner Deceleration General This function automatically controls the feedrate during corner machining according to the angle of a corner made by machining blocks or according to the feedrate difference for each
- Page 3527. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 @ When linear acceleration/deceleration before interpolation for cutting feed is enabled If the angle made by blocks A and B is smaller than that specified in parameter No. 1740 (for the selected plane), and if the feedrates pr
- Page 3537. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Block A (G01) Block B (G01) θ θ Block A (G02) Block B(G01) Angle made by two lines If a circular path is included, the angle between the tangent of the arc and another line is considered. 1741 Feedrate for assuming the terminat
- Page 3547. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Caution CAUTION 1 The angle of the machining tool path is compared with that specified in parameter No. 1740 only for the selected plane. The actual feedrate and that specified in parameter No. 1741 are compared only for the fi
- Page 3557. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL @ When linear acceleration/deceleration before interpolation for cutting feed is enabled If the difference between the feedrates of blocks A and B for each axis exceeds the value specified in parameter No. 1780, the feedrate at
- Page 3567. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 N1 G01 G91 X100. F1000 ; N2 N2 Y100. ; N1 Tool path if corner deceleration is not applied ← Tool path when corner deceleration was applied Speed F1000 Feedrate Without corner deceleration along With corner deceleration X axis F
- Page 3577. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL D Parameter #7 #6 #5 #4 #3 #2 #1 #0 1601 ACD [Data type] Bit ACD Function for automatically reducing the feedrate at corners (automatic corner deceleration function) 0 : The function is not used. 1 : The function is used. #7 #6
- Page 3587. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 1781 Allowable speed difference for the speed difference–based automatic corner deceleration function (for acceleration/deceleration after interpolation) [Data type] Word axis [Unit of data] Valid data range Increment system Un
- Page 3597. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.1.11 Advanced Preview Control General This function is designed for high–speed precise machining. With this function, the delay due to acceleration/deceleration and the delay in the servo system which increase with the feedra
- Page 3607. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Parameter 1431 Maximum cutting feedrate for all axes in the advanced preview control mode [Data type] Two–word [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine
- Page 3617. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE 1 This parameter is effective only in linear and circular interpolation. In polar coordinate, cylindrical, and involute interpolation, the maximum feedrate for all axes specified in parameter No. 1431 is effective. 2 If a
- Page 3627. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 1602 LS2 CSD FWB [Data type] Bit FWB Cutting feed acceleration/deceleration before interpolation 0 : Type A of acceleration/deceleration before interpolation is used. 1 : Type B of acceleration/decelerat
- Page 3637. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 1762 Exponential acceleration/deceleration time constant for cutting feed in the advanced preview control mode [Data type] Word axis [Unit of data] 1 ms [Valid data range] 0 to 4000 Set an exponential acceleration/deceleration
- Page 3647. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 1770 Parameter 1 for setting an acceleration for linear acceleration/deceleration before interpolation in the advanced preview control mode (maximum machining speed during linear acceleration/deceleration before interpolation)
- Page 3657. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL CAUTION 1 When 0 is set in parameter No. 1770 or parameter No. 1771, linear acceleration/deceleration before interpolation is disabled. 2 In parameter Nos. 1770 and 1771, set values that satisfy the following: Parameter No. 177
- Page 3667. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 1780 Allowable speed difference for the speed difference based corner deceleration function (for linear acceleration/deceleration before interpolation) [Data type] Word [Unit of data] Valid data range Increment system Unit of d
- Page 3677. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE 1 When 0 is set in this parameter, the control described above is not exercised. 2 Use type–B linear acceleration/deceleration before interpolation (by setting bit 0 (FWB) of parameter No. 1602 to 1). #7 #6 #5 #4 #3 #2 #1
- Page 3687. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 @ Parameters for automatic corner deceleration Parameter No. Parameter description Advanced Normal mode preview control mode Automatic corner deceleration according to the corner angle or the speed difference CSD (1602#4) CSD (
- Page 3697. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE S Cs contour control (usable in the advanced preview control mode by setting bit 5 (G8S) of parameter No. 1602. The serial spindle parameter also needs to be set.) S Constant surface speed control S Spindle speed fluctuati
- Page 3707. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.1.12 AI Advanced Control (M Series) General The AI advanced control function is provided for high–speed, high–precision machining. This function enables suppression of acceleration/deceleration delays and servo delays that be
- Page 3717. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Linear acceleration/ deceleration before interpolation Pulse Specified distribution Acceleration/ Calculation feedrate Calculation of Servo deceleration af- of feedrate interpolation ter interpolation control Linear interpolati
- Page 3727. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Automatic corner When there are axes for which the difference in feedrate between blocks deceleration exceeds the allowable feedrate difference set in parameter 1783, the automatic corner deceleration function calculates the fe
- Page 3737. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL N1 G01 G91 X100. F1000 ; N2 Y100. ; N2 Tool path when tool movement is not decelerated at the corner Tool path when tool movement is decelerated at the corner Feedrate on the X–axis N1 Feedrate When deceleration is not performe
- Page 3747. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Feedrate clamping by When a curve is made up of a series of short straight lines as shown in the acceleration figure below, the difference in feedrate on each axis at each corner is not large. Therefore, deceleration by feedrat
- Page 3757. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Feedrate on X Feedrate on Y Tongent direction feed rate N1 N5 N9 N1 N5 N9 Without feedrate clamping Without feedrate clamping Feedrate clamping by This function can suppress acceleration in an arc machining block to an arc radi
- Page 3767. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 NOTE As the specified arc radius becomes smaller, the maximum allowable feedrate v falls. To prevent the maximum allowable feedrate from becoming too small, the lower limit for feedrate clamping based on the arc radius can be s
- Page 3777. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Feedrate Linear acceleration/deceleration Bell–shaped acceleration/deceleration ta: Depends on linear acceleration/deceleration. tb: Bell–shaped time constant tc: Bell–shaped acceleration/deceleration time tc = ta + tb ta is no
- Page 3787. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Specifications Axis control f : Can be programmed : Cannot be programmed Name Description Controlled axes 3 to 4 axes Simultaneously controlled Up to 4 axes axes Axis name Basic three axes: Always X, Y, and Z Other axes: U, V,
- Page 3797. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Interpolation function f : Can be programmed : Cannot be programmed Name Description Positioning (G00) f Single direction positioning f To perform single direction positioning in the (G60) AI advanced preview control mode, bit
- Page 3807. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Feed functions f : Can be programmed : Cannot be programmed Name Description Rapid traverse rate Up to 240 m/min (0.01 mm) Up to 100 m/min (0.0001 mm) Rapid traverse rate override F0, 25, 50, 100 % Rapid traverse rate override
- Page 3817. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Name Description Local coordinate system f * (G52) Machine coordinate system f * (G53) Workpiece coordinate system f * (G54 to G59) (G54.1Pxx) Workpiece coordinate system f * (G92) Workpiece coordinate system f * preset (G92.1)
- Page 3827. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Auxiliary functions/spindle functions f : Can be programmed : Cannot be programmed Name Description Miscellaneous function f Only the output of the function code signal (Mxxxx) and function strobe signal is performed. Second au
- Page 3837. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Name Description Program restart f As an acceleration/deceleration time constant for movement to a restart position, the following parameters are used: When exponential acceleration/decelera- tion is used: Parameter No. 1624 an
- Page 3847. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Signal AI advanced preview control mode signal AICC
- Page 3857. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE 1 When parameter 1770 or 1771 is set to 0, linear acceleration/deceleration before interpolation is not performed. 2 Set these parameters so that parameter 1770/parameter 1771 = 5 or more. Feedrate (mm/min) Parameter 1770
- Page 3867. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 If the following condition is satisfied, deceleration is performed: Distance required for de- Distance to the celerating the current speed stored stroke limit < (tangent direction feedrate) on an axis to the speed set in parame
- Page 3877. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL D Parameter related to feedrate clamping by acceleration 1785 Parameter for determining the allowable acceleration in feedrate clamping by acceleration [Data type] Word axis [Unit of data] 1 ms [Valid data range] 0 to 32767 Thi
- Page 3887. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 (Example) Specified feedrate N1 a N2 b r a b N3 N1 N2 N3 Time 1732 Lower limit RVmin for feedrate clamping by arc radius [Data type] Word [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS–A, IS
- Page 3897. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE Be sure to set a maximum cutting feedrate in both of parameter No. 1422 and No. 1432. #7 #6 #5 #4 #3 #2 #1 #0 1603 RBL [Data type] Bit RBL In the AI advanced preview control, acceleration/deceleration of rapid traverse is:
- Page 3907. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 NOTE When a value of ”0” is set as the character code, ”AI APC” blinks. #7 #6 #5 #4 #3 #2 #1 #0 6901 PSF [Data type] Bit PSF In AI advanced preview control mode, position switches are: 0 : Not used. 1 : Used. NOTE The position
- Page 3917. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL D The rigid mode cancel command and cutting feed move command cannot be specified simultaneously. If they are specified simultaneously, P/S alarm No. 5110 is issued. (Additional information: The rigid mode cancel command and ra
- Page 3927. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 NOTE 1 When an index table indexing axis is specified, G27, G28, G30, G30.1, or G53 is executed with AI advanced preview control turned off, regardless of the setting of bit 3 (AZR) of parameter No. 7054. 2 When G27, G28, G30,
- Page 3937. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE 1 If an axis for which a reference position is established and an axis for which no reference position is established are simultaneously specified with G28 when bit 2 (ALZ) of parameter No. 7055 is set to 1, G28 is execute
- Page 3947. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 (2) Parameters related to automatic corner deceleration Parameter No. Parameter Standard Advanced AI advanced mode preview preview control control Method for determining auto- CSD/1602#4 None matic corner deceleration (angle/fe
- Page 3957. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL (5) Other parameters Parameter No. Parameter Standard Advanced AI advanced mode preview preview control control Precision of radius error in cir- PCIR1/3403#0 None cular interpolation Maximum cutting feedrate 1422 1431 1422 (fo
- Page 3967. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Caution 1 When the total distance for the blocks under advanced preview control is equal to or less than the deceleration distance from the current feedrate, deceleration starts. When advanced preview control has proceeded upon
- Page 3977. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Details of NC statement and macro statement execution > N1 G01 G91 X50.0 Y30.0 F100 ; N2 #1=100 ; N3 X100.0 ; > : Block being executed N4 #2=200 ; j : Block read into the buffer N5 Y50.0 ; | N1 NC statement execution N2 N4 Macr
- Page 3987. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Meaning Read/ Variable Remarks (when buffering write number is not suppressed) Block end (work- Read #5001 to The block end of up to the piece coordinate #5008 third block ahead can be system) read. Machine coordi- Read #5021 t
- Page 3997. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2 ACCELERATION/ DECELERATION CONTROL 7.2.1 Automatic Acceleration/ Deceleration 7.2.1.1 Automatic acceleration/ deceleration General D Automatic acceleration/ To prevent a mechanical shock, acceleration/deceleration is automa
- Page 4007. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Rapid traverse:Linear acceleration/deceleration (time constant per axis is set by parameter 1620) Cutting feed: Exponential acceleration/deceleration (time constant per axis is set by parameter 1622) Jog feed : Exponential acce
- Page 4017. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE When parameter No. 1621 (time constant T2 used for bell–shaped acceleration/deceleration in rapid traverse) is set to 0, linear acceleration/deceleration is applied in rapid traverse even. In this case, this parameter stan
- Page 4027. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 1625 FL rate of exponential acceleration/deceleration in jog feed for each axis [Data type] Word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS-A, IS-B IS-C Millimeter machine 1 mm/min
- Page 4037. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2.1.2 Rapid traverse block overlap General Rapid traverse blocks may be arranged successively or a rapid traverse block may be followed by a block that does not cause movement. In this case, execution of the next block can be
- Page 4047. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 NOTE The parameter No. 1722 is effective when parameter No. 1601 #4 (RTO) is set to 1. Example Fh: Rapid traverse feedrate X–axis feedrate α: Setting of parameter No. 1722 (feedrate reduction ratio) Fd: Feedrate where decelerat
- Page 4057. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2.2 Rapid Traverse Bell–shaped Acceleration/ Deceleration General Rapid traverse bell–shaped acceleration/deceleration smoothly increases or decreases the rapid traverse rate, reducing the stress and strain imposed on the mac
- Page 4067. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02
Speed Rapid traverse rate Time T: Time constant for linear T acceleration/deceleration T Speed Rapid traverse rate T1: Set - Page 4077. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL NOTE When parameter No. 1621 (time constant T2 used for bell–shaped acceleration/deceleration in rapid traverse) is set to 0, linear acceleration/deceleration is applied in rapid traverse even. In this case, this parameter stan
- Page 4087. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 7.2.3 Linear Acceleration/ Deceleration after Cutting Feed Interpolation General If linear acceleration/deceleration after interpolation for cutting feed is enabled (bit 0 of parameter No. 1610, CTL), acceleration/deceleration
- Page 4097. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL Linear acceleration/deceleration after cutting feed interpolation function is enabled when the CTL bit (bit 0 of parameter No. 1610) is specified. The time constants for cutting feed and jog feed for each axis are specified in
- Page 4107. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Note NOTE 1 If linear acceleration/deceleration after interpolation for cutting feed is enabled, linear acceleration/deceleration is executed during cutting feed and during a dry run. Linear acceleration/deceleration can also b
- Page 4117. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2.4 Corner Control 7.2.4.1 In–position check General Whether the position of the servo motor is within a specified range is checked. If the in–position check function is enabled, the CNC checks the position during deceleratio
- Page 4127. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Signal address . #7 #6 #5 #4 #3 #2 #1 #0 F104 INP4 INP3 INP2 INP1 Parameter #7 #6 #5 #4 #3 #2 #1 #0 1601 NCI [Data type] Bit NCI Inposition check at deceleration 0 : Performed 1 : Not performed 1826 In–position width for each a
- Page 4137. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2.4.2 In–position check independently of feed/rapid traverse General If separate in–position check for cutting feed and rapid traverse is executed, a small in–position check range can be specified between those cutting feed b
- Page 4147. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 1826 In–position width for each axis [Data type] Word axis [Unit of data] Detection unit [Valid data range] 0 to 32767 The in–position width is set for each axis. When the deviation of the machine position from the specified po
- Page 4157. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2.4.3 Error detect (T series) General Generally, the CNC does not zero the feedrate at the interface of two blocks during cutting feed. Because of this, a corner of a tool path may be rounded. This part causes the corner of t
- Page 4167. FEEDRATE CONTROL/ACCELERATION AND DECELERATION CONTROL B–63833EN–1/02 Siganl address #7 #6 #5 #4 #3 #2 #1 #0 G053 SMZ Note NOTE If the error detect signal is on, a cutting block is not executed until the acceleration/deceleration of the previous cutting block has been completed. This function alo
- Page 4177. FEEDRATE CONTROL/ACCELERATION B–63833EN–1/02 AND DECELERATION CONTROL 7.2.5 Feed Forward in Rapid Traverse General Feed–forward control can be performed even during rapid traverse. In this case, the servo position error is reduced, thus reducing the time required for positioning to within the spe
- Page 4188. AUXILIARY FUNCTION B–63833EN–1/02 8 AUXILIARY FUNCTION 400
- Page 419B–63833EN–1/02 8. AUXILIARY FUNCTION 8.1 MISCELLANEOUS FUNCTION/2ND AUXILIARY FUNCTION General D Miscellaneous Function When an M code address is programmed, a code signal and a strobe signal (M code) are sent to the machine. The machine uses these signals to turn on or off its functions. Usually, o
- Page 4208. AUXILIARY FUNCTION B–63833EN–1/02 3. It is possible to change over the scale factor of B output 1000 or 10000 when the decimal point input is omitted in the inch input system, using the parameter AUX (No.3405#0). When DPI=1. Command Output value When AUX is 1: B1 10000 When AUX is 0: B1 1000 Basi
- Page 421B–63833EN–1/02 8. AUXILIARY FUNCTION (6) If the completion signal remains set to 1 for longer than period TFIN, specified in parameter No. 3011 (standard value: 16 msec), the CNC sets the strobe signal to 0 and reports that the completion signal has been received. (7) When the strobe signal is set t
- Page 4228. AUXILIARY FUNCTION B–63833EN–1/02 2b. Execution of a miscellaneous function after move command completion (1)(2) (3) (4) (5) (6)(7)(8) (9) M command Mxx Move command Code signals M00–M31 (*2) Strobe signal MF PMC side action End signal FIN Distribution end signals DEN TMF TFIN Signal Miscellaneou
- Page 423B–63833EN–1/02 8. AUXILIARY FUNCTION Decode M signals DM00
- Page 4248. AUXILIARY FUNCTION B–63833EN–1/02 Second auxiliary function code signals B00 to B31
- Page 425B–63833EN–1/02 8. AUXILIARY FUNCTION The DEN signal turns to “0” when: · The execution of one block is completed NOTE A parameter NCI (No.1601#5) can specify, whether to only check if an acceleration/deceleration delay is eliminated, or to also check if a servo delay (error) has been reduced to with
- Page 4268. AUXILIARY FUNCTION B–63833EN–1/02 Parameter 3010 Time lag in strobe signals MF, SF, TF, and BF [Data type] Word [Unit of data] 1 ms [Valid data range] 16 to 32767 The time required to send strobe signals MF, SF, TF, and BF after the M, S, T, and B codes are sent, respectively. M, S, T, B code MF,
- Page 427B–63833EN–1/02 8. AUXILIARY FUNCTION NOTE The time is counted in units of 8 ms. If the set value is not a multiple of eight, it is raised to the next multiple of eight. Example: When 30 is set, 32 ms is assumed. 3030 Allowable number of digits for the M code 3031 Allowable number of digits for the S
- Page 4288. AUXILIARY FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3405 AUX [Data type] Bit AUX The least increment of the command of the second miscellaneous function specified with a decimal point 0 : Assumed to be 0.001 1 : Depending on the input increment. (For input in mm, 0.001 is assumed, or for in
- Page 429B–63833EN–1/02 8. AUXILIARY FUNCTION [Data type] Word [Valid data range] 0 to 65535 When a specified M code is within the range specified with parameter Nos. 3421 and 3422, 3433 and 3424, 3425 and 3426, 3427 and 3428, 3429 and 3430, or 3431 and 3432, buffering for the next block is not performed unt
- Page 4308. AUXILIARY FUNCTION B–63833EN–1/02 Note NOTE 1 When a move command and miscellaneous function are specified in the same block, the commands are executed in one of the following two ways: i) Simultaneous execution of the move command and miscellaneous function commands. ii) Executing miscellaneous
- Page 431B–63833EN–1/02 8. AUXILIARY FUNCTION 8.2 AUXILIARY FUNCTION LOCK General Inhibits execution of a specified M, S, T and B function. That is, code signals and strobe signals are not issued. This function is used to check a program. Signal Auxiliary function lock signal AFL
- Page 4328. AUXILIARY FUNCTION B–63833EN–1/02 Auxiliary function lock check signal MAFL
- Page 433B–63833EN–1/02 8. AUXILIARY FUNCTION 8.3 MULTIPLE M COMMANDS IN A SINGLE BLOCK General So far, one block has been able to contain only one M code. However, this function allows up to three M codes to be contained in one block. Up to three M codes specified in a block are simultaneously output to the
- Page 4348. AUXILIARY FUNCTION B–63833EN–1/02 A time chart for this procedure is shown below: M command (MaaMbbMcc;) Code signal M00-M31 Strobe signal MF Code signal M200-M215 Strobe signal MF2 Code signal M300-M315 Strobe signal MF3 PMC side operation End signal FIN TMF TFIN Signal 2nd, 3rd M function code
- Page 435B–63833EN–1/02 8. AUXILIARY FUNCTION Parameter #7 #6 #5 #4 #3 #2 #1 #0 3404 M3B [Data type] Bit M3B The number of M codes that can be specified in one block 0 : One 1 : Up to three Caution CAUTION 1 M00, M01, M02, M30, M98, M99, or M198 must not be specified together with another M code. 2 Some M co
- Page 4368. AUXILIARY FUNCTION B–63833EN–1/02 Reference item OPERATOR’S MANUAL Multiple M commands in a single II.11.2 (M series) (B–63844EN) block Series 0i–B OPERATOR’S MANUAL Multiple M commands in a single II.11.2 (T series) (B–63834EN) block OPERATOR’S MANUAL Multiple M commands in a single II.11.2 (M s
- Page 437B–63833EN–1/02 8. AUXILIARY FUNCTION 8.4 HIGH–SPEED M/S/T/B INTERFACE General To accelerate M/S/T/B function execution, the high–speed M/S/T/B interface has simplified the transfer of the strobe and completion signals of the M/S/T/B functions. Whether to use the usual system or high–speed system for
- Page 4388. AUXILIARY FUNCTION B–63833EN–1/02 Next block Code signal Mxx Myy Strobe signal MF PMC side operation Miscellaneous function completion signal MFIN Fig. 8.4 (a) Timing chart of the high–speed system Next block Code signal Mxx Myy Strobe signal MF PMC side operation Completion signal FIN Fig. 8.4 (
- Page 439B–63833EN–1/02 8. AUXILIARY FUNCTION Spindle function completion signal SFIN
- Page 4408. AUXILIARY FUNCTION B–63833EN–1/02 [Operation] Refer to the description of the output conditions and procedure described in “basic procedure.” External operation function completion signal (M series) EFIN
- Page 441B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9 SPINDLE SPEED FUNCTION 423
- Page 4429. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.1 SPINDLE SPEED FUNCTION (S CODE OUTPUT) General When up to five digits are specified after address S, code and strobe signals are sent out and used to control the spindle speed. The code signals are retained until another S code is issued. One S code is us
- Page 443B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.2 SPINDLE SERIAL OUTPUT/SPINDLE ANALOG OUTPUT General There are two types of spindle motor control interfaces, spindle serial output and spindle analog output. The spindle serial output interface can control up to two serial spindles. The spindle analog out
- Page 4449. SPINDLE SPEED FUNCTION B–63833EN–1/02 The table below lists the relationship between the spindles and functions. f=Available ×=Unavailable Serial spindle Analog spindle Spindle Function When used as the When used as the First serial Second serial first spindle (with third spindle spindle spindle
- Page 445B–63833EN–1/02 9. SPINDLE SPEED FUNCTION The signals and parameters for spindle speed control are common to both spindle serial output and spindle analog output. (See Section 9.3.) The table below lists the differences related to direct control of the spindle control unit. Spindle control unit for S
- Page 4469. SPINDLE SPEED FUNCTION B–63833EN–1/02 Signal address D For 1st SERIAL SPINDLE #7 #6 #5 #4 #3 #2 #1 #0 G070 MRDYA ORCMA SFRA SRVA CTH1A CTH2A TLMHA TLMLA G071 RCHA RSLA SOCNA MCFNA SPSLA *ESPA ARSTA G072 RCHHGA MFNHGA INCMDA OVRIDA DEFMDA NRROA ROTAA INDXA G073 MPOFA SLVA MORCMA #7 #6 #5 #4 #3 #2
- Page 447B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Parameter D Connection of serial spindle control unit #7 #6 #5 #4 #3 #2 #1 #0 3701 SS2 ISI [Data type] Bit ISI Specifieds whether the serial spindle interface is used. 0 : Used 1 : Not used NOTE 1 This parameter is enabled only when the serial spindle interfa
- Page 4489. SPINDLE SPEED FUNCTION B–63833EN–1/02 Alarm and message Number Message Contents 749 S–SPINDLE LSI ERROR It is serial communication error while system is executing after power supply on. Following reasons can be considered. 1) Optical cable connection is fault or cable is not connected or cable is
- Page 449B–63833EN–1/02 9. SPINDLE SPEED FUNCTION DIAGNOSIS SCREEN D Information on spindle control #7 #6 #5 #4 #3 #2 #1 #0 400 SAI SS2 SSR POS SIC SIC 0: No module is present for spindle serial output. 1: A module for spindle serial output is present. POS 0: No module is present for spindle analog output. 1
- Page 4509. SPINDLE SPEED FUNCTION B–63833EN–1/02 D Load and speed meter readings for the serial spindle 410 First serial spindle: Load meter reading (%) 411 First serial spindle: Speed meter reading (min–1) 412 Second serial spindle: Load meter reading (%) 413 Second serial spindle: Speed meter reading (min
- Page 451B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.3 SPINDLE SPEED CONTROL General This section describes spindle speed control. It also explains the position coder and the spindle speed arrival signal (SAR). 433
- Page 4529. SPINDLE SPEED FUNCTION B–63833EN–1/02 Command flow of The following chart summarizes spindle speed control. spindle speed control CNC PMC and machine Machining program, etc. ↓ Gear select signal output Output to the PMC ⋅ S command (M series) (to change the machine gear). (GR3O, GR2O, GR1O) ⋅S co
- Page 453B–63833EN–1/02 9. SPINDLE SPEED FUNCTION D S command The S command specifies the spindle speed entered from machining programs, etc. for the CNC. For constant surface speed control (during G96 mode), the CNC converts the specified surface speed to the spindle speed. In the M series with bit 4 (GTT)
- Page 4549. SPINDLE SPEED FUNCTION B–63833EN–1/02 D Processing for gear Although the S command contains the spindle speed, the object that is changing actually controlled is the spindle motor. Therefore, the CNC must have some provision to detect the gear stage between the speed and spindle motor. There are
- Page 455B–63833EN–1/02 9. SPINDLE SPEED FUNCTION The speed commands output to the spindle motor are as follows: ⋅ For the serial spindle, the speed commands are processed as values 0 to 16383 between the CNC and spindle control unit. ⋅ For the analog spindle, the speed commands are output to the analog volt
- Page 4569. SPINDLE SPEED FUNCTION B–63833EN–1/02 NOTE If a specified voltage of 10 V is already higher than the acceptable input voltage for the spindle drive system, calculate the spindle speed that corresponds to 10 V using a proportional calculation method and use it instead. Now, in response to the spec
- Page 457B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Spindle motor speed command (analog voltage output) 10V VC VH GR3O VL GR1O GR2O Spindle speed command A B C (S code input) Vmin Vmaxl Vmaxh Vmax A× A× B× C× 4095 4095 4095 4095 VC: Voltage corresponding to the upper limit of output value to spindle motor. VH:
- Page 4589. SPINDLE SPEED FUNCTION B–63833EN–1/02 · Spindle speed A (Parameter No.3741) (min–1) with low-speed gears when the command voltage is 10V · Spindle speed B (Parameter No.3742) (min–1) with high-speed gears when the command voltage is 10V (medium-speed gear for 3-stage) · Spindle speed C (Parameter
- Page 459B–63833EN–1/02 9. SPINDLE SPEED FUNCTION D When Gear select signal change S code read To next block Gear select signal TM GR3O F /GR2O /GR1O SF FIN TMF TFIN Spindle speed command VH VL 0V Fig. 9.3 (e) Time chart when gear select signal changes In this case, the gear select signal is output; after el
- Page 4609. SPINDLE SPEED FUNCTION B–63833EN–1/02 In addition, for the speed command output to the spindle motor, analog voltages 0 to 10 V for analog spindle control correspond to digital data 0 to 16383 for serial spindle control. However, it might be easier if you consider them code signals from 0 to 4095
- Page 461B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Reference→ Block Diagram for Analog Voltage Output With the constant surface speed control CNC Power magnetics cabinet [Surface speed] M code Gear change command S(m/min) Spindle speed X–axis pres- command ent value Constant r S (min–1) surface min–1/10V spee
- Page 4629. SPINDLE SPEED FUNCTION B–63833EN–1/02 Keep the following in mind: Even with bit 7 (TCW) of parameter No. 3706 = 1, the CNC cannot determine the output polarity if it has not issued M03/M04, and therefore, actual output does not work even if the speed command has been specified. D Command output t
- Page 463B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Control unit max+10V SVC SVC Spindle speed 2mA analog voltage Name Connector/Pin ES Output ES output SVC JA8A/7 impedance 100Ω ES JA8A/5 ENB1 ENB Enable signal ENB1 JA8A/8 ENB2 ENB2 JA8A/9 WARNING Since the output voltage is a weak signal, do not relay it thr
- Page 4649. SPINDLE SPEED FUNCTION B–63833EN–1/02 Signal Spindle stop signal *SSTP
- Page 465B–63833EN–1/02 9. SPINDLE SPEED FUNCTION low gear range, the gear select signal does not change and the command output is calculated and output to obtain the set speed at high gear. When the spindle motor speed is set by parameter GST (No. 3705#1)=1, the command output is output regardless of gear s
- Page 4669. SPINDLE SPEED FUNCTION B–63833EN–1/02 → When this function is not in use, specify an override of 100%; otherwise, an override of 0% becomes effective, thus disabling the spindle from rotating. Spindle speed arrival signal SAR
- Page 467B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Spindle enable signal ENB
- Page 4689. SPINDLE SPEED FUNCTION B–63833EN–1/02 S12–bit code signal R01O to R12O
- Page 469B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Signal address #7 #6 #5 #4 #3 #2 #1 #0 G027 CON *SSTP3 *SSTP2 *SSTP1 SWS3 SWS2 SWS1 G028 GR2 GR1 G029 *SSTP SOR SAR G030 SOV7 SOV6 SOV5 SOV4 SOV3 SOV2 SOV1 SOV0 G032 R08I R07I R06I R05I R04I R03I R02I R01I G033 SIND SSIN SGN R12I R11I R10I R09I #7 #6 #5 #4 #3
- Page 4709. SPINDLE SPEED FUNCTION B–63833EN–1/02 GST: The SOR signal is used for: 0 : Spindle orientation 1 : Gear shift SGB: Gear switching method 0 : Method A (Parameters No. 3741 to 3743 for the maximum spindle speed at each gear are used for gear selection.) 1 : Method B (Parameters No. 3751 and 3752 fo
- Page 471B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE 1 Type M: The gear selection signal is not entered externally. In response to an S command, the CNC selects a gear according to the speed range for each gear specified in parameters. Then the CNC reports the selection of a gear by outputting the gear sel
- Page 4729. SPINDLE SPEED FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3709 SAM [Data type] Bit SAM The sampling frequency to obtain the average spindle speed 0 : 4 (Normally, set to 0.) 1: 1 3730 Data used for adjusting the gain of the analog output of spindle speed [Data type] Word [Unit of data] 0.1 %
- Page 473B–63833EN–1/02 9. SPINDLE SPEED FUNCTION (5) After setting the parameters, command “0”, confirm that the output is 0V. NOTE This parameter need not to be set for serial spindles. 3732 The spindle speed during spindle orientation or the spindle motor speed during spindle gear shift [Data type] Two–wo
- Page 4749. SPINDLE SPEED FUNCTION B–63833EN–1/02 Spindle motor speed Max. speed (4095, 10V) Spindle motor max. clamp speed (Parameter No. 3736) Spindle motor minimum clamp speed (Parameter No. 3735) Spindle speed (S command) NOTE If the function of constant surface speed control or bit 4 (GTT) of parameter
- Page 475B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 3741 Maximum spindle speed for gear 1 3742 Maximum spindle speed for gear 2 3743 Maximum spindle speed for gear 3 3744 Maximum spindle speed for gear 4 [Data type] Word [Unit of data] min–1 [Valid data range] 0 to 32767 Set the maximum spindle speed correspon
- Page 4769. SPINDLE SPEED FUNCTION B–63833EN–1/02 3751 Spindle motor speed when switching from gear 1 to gear 2 3752 Spindle motor speed when switching from gear 2 to gear 3 [Data type] Word [Valid data range] 0 to 4095 For gear switching method B, set the spindle motor speed when the gears are switched. Spi
- Page 477B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 3761 Spindle speed when switching from gear 1 to gear 2 during tapping 3762 Spindle speed when switching from gear 2 to gear 3 during tapping [Data type] Word [Unit of data] min–1 [Valid data range] 0 to 32767 When method B is selected (SGT,#3 of parameter 37
- Page 4789. SPINDLE SPEED FUNCTION B–63833EN–1/02 3772 Maximum spindle speed [Data type] Word [Unit of data] min–1 [Valid data range] 0 to 32767 This parameter sets the maximum spindle speed. When a command specifying a speed exceeding the maximum speed of the spindle is specified , or the speed of the spind
- Page 479B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Caution CAUTION This section mentioned a spindle speed control that should be prepared on the CNC side. But it is also necessary to design the signals to the spindle control unit. Consult the manual of the spindle control unit used and take necessary actions
- Page 4809. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.4 CONSTANT SURFACE SPEED CONTROL General With the spindle serial output or analog output function, specifying the surface speed (m/min or feet/min) directly in an S command makes it possible to change the spindle output continuously so as to maintain a cons
- Page 481B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Example of Spindle Assume that gear switching is two stage switching. If the spindle speed Analog Output with the output 10 V is 1000 min–1 for the low speed gear (G1) and 2000 min–1 for the high speed gear (G2), set these speeds to the parameter No. 3741, 37
- Page 4829. SPINDLE SPEED FUNCTION B–63833EN–1/02 Spindle Serial Output The output to the spindle in spindle serial output is a digital data. Therefore assume the following relation for calculation: Spindle analog output (voltage) 10V = Spindle serial output (digital data) 4095. The above calculation becomes
- Page 483B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Parameter #7 #6 #5 #4 #3 #2 #1 #0 1405 FPR [Data type] Bit FPR Specifies the feed–per–revolution function with no position coder. 0 : Not used. 1 : Used. NOTE If you set this parameter to 1, reset parameter NPC (bit 0 of parameter No. 1402) to 0. 3741 Maximum
- Page 4849. SPINDLE SPEED FUNCTION B–63833EN–1/02 3772 Maximum spindle speed [Data type] Word [Unit of data] min–1 [Valid data range] 0 to 32767 This parameter sets the maximum spindle speed. When a command specifying a speed exceeding the maximum spindle speed is specified, or the spindle speed exceeds the
- Page 485B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Note NOTE Simultaneous use of multi–spindle control enables constant surface speed control for spindles other than the first spindle. (See Section 9.9.) Reference item OPERATOR’S MANUAL CONSTANT SURFACE SPEED II.9.3 (M series) (B–63844EN) CONTROL (G96, G97) S
- Page 4869. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.5 SPINDLE SPEED FLUCTUATION DETECTION General With this function, an overheat alarm (No. 704) is raised and the spindle speed fluctuation detection alarm signal SPAL is issued when the spindle speed deviates from the specified speed due to machine condition
- Page 487B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 1. When an alarm is issued after a specified spindle speed is reached Spindle speed Sr Sd Sq Specified Sq Sd speed Sr Actual speed Check No check Check Time Specification of Start of check Alarm another speed 2. When an alarm is issued before a specified spin
- Page 4889. SPINDLE SPEED FUNCTION B–63833EN–1/02 Signal Spindle fluctuation detection alarm signal SPAL
- Page 489B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 4911 Percent tolerance (q) of the target spindle speed to begin checking [Data type] Word [Unit of data] Unit of data 1% 0. 1% (T series) Data range 1 – 100 1 – 1000 [Valid data range] NOTE Unit of data depends on parameter No. 4900#0 FLR (T series only) Set
- Page 4909. SPINDLE SPEED FUNCTION B–63833EN–1/02 Alarm and message Number Message Description 704 OVER HEAT : SPINDLE Spindle overheat in the spindle fluc- tuation detection (1) If the cutting load is heavy, relieve the cutting condition. (2) Check whether the cutting tool is share. (3) Another possible cau
- Page 491B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.6 ACTUAL SPINDLE SPEED OUTPUT (T SERIES) General The PMC can read actual spindle speed. Signal Actual spindle speed signal AR0 to AR15
- Page 4929. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.7 SPINDLE POSITIONING (T SERIES) General This function positions the spindle using the spindle motor and position coder. The function has a coarser least command increment compared with the Cs contour control function and has no interpolation capability wit
- Page 493B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Selecting a spindle Any axis in the control axis group can be used as the C axis (parameter positioning axis no. 1020). Specify *1 as its servo axis number (parameter no. 1023). The spindle subjected to spindle positioning is the first spindle. Switching to s
- Page 4949. SPINDLE SPEED FUNCTION B–63833EN–1/02 Command system The command system comes in two types: The first positions a semi-fixed angle; the second positions an optional angle. D Semi-fixed angle A 2-digit numerical value following the M address is used for the positioning by M code command. There are
- Page 495B–63833EN–1/02 9. SPINDLE SPEED FUNCTION D Absolute and Positioning by specifying a semi–fixed angle (by M code) is always incremental commands incremental. To perform positioning by specifying an optional angle, specify the distance between the program origin and the end point (absolute) with addre
- Page 4969. SPINDLE SPEED FUNCTION B–63833EN–1/02 Signal Spindle stop complete signal SPSTP
- Page 497B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Other signals Gear selection signal Refer to 9.3 “Spindle Speed Control.” GR1, GR2,
- Page 4989. SPINDLE SPEED FUNCTION B–63833EN–1/02 Sequence (Time chart) - Spindle Orientation M code MF SPSTP POSITION LOOP INITIALIZE Spindle enable on SUCLP *SUCPF Spindle movement ZPx SCLP Spindle enable off *SCPF FIN ⇒ POSITION LOOP INITIALIZE is performed within the CNC. ⇒ Spindle ENABLE ON/OFF specifie
- Page 499B–63833EN–1/02 9. SPINDLE SPEED FUNCTION - Spindle Positioning by M code M code MF SPSTP Spindle enable on SUCLP *SUCPF Spindle movement SCLP Spindle enable off *SCPF FIN 481
- Page 5009. SPINDLE SPEED FUNCTION B–63833EN–1/02 - Spindle Positioning by Address C,H SPSTP Spindle enable ON SUCLP *SUPCF Spindle movement SCLP Spindle enable OFF *SCPF - Spindle Positioning Reset M code MF SPSTP POSITION CODER INITIALIZE SUCLP *SUPCF FIN ⇒ POSITION CODER INITIALIZE is performed only in th
- Page 501B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Parameter #7 #6 #5 #4 #3 #2 #1 #0 1006 ZMIx [Data type] Bit axis ZMIx The direction of reference position return and the direction of initial backlash at power–on 0 : Positive direction 1 : Negative direction NOTE When the serial spindle is being used, this p
- Page 5029. SPINDLE SPEED FUNCTION B–63833EN–1/02 1420 Rapid traverse rate for each axis [Data type] Word axis Set the rapid traverse rate when the rapid traverse override is 100% for each axis. For spindle positioning. [Unit of data] 10 deg/min [Valid data range] 30 to 12000 1421 F0 rate of rapid traverse o
- Page 503B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 1820 Command multiply for each axis (CMR) [Data type] Byte axis D When command multiply is 1/2 to 1/27 1 Set value= +100 [Valid data range: 102 to 127] (Command multiply) D When command multiply is 0.5 to 48 Set value = 2 command multiply [Valid data range: 1
- Page 5049. SPINDLE SPEED FUNCTION B–63833EN–1/02 1850 Grid shift for each axis [Data type] Two–word axis [Unit of data] Detection unit [Valid data range] –99999999 to 99999999 Set a grid shift for each axis. NOTE Set this parameter when the analog spindle is used. When the serial spindle is used, set the va
- Page 505B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 4044 Velocity loop proportion gain in servo mode (High gear) 4045 Velocity loop proportion gain in servo mode ( Low gear) [Data type] Word [Valid data range] 0 to 32767 This parameter sets a velocity loop proportional gain in servo mode (spindle positioning,
- Page 5069. SPINDLE SPEED FUNCTION B–63833EN–1/02 4065 Position gain in servo mode (HIGH) 4066 Position gain in servo mode (MEDIUM HIGH) 4067 Position gain in servo mode (MEDIUM LOW) 4068 Position gain in servo mode (LOW) [Data type] Word [Unit of data] 0.01 sec–1 [Valid data range] 0 to 32767 This parameter
- Page 507B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE The extended specification includes the following two extensions: D With the conventional specification, the number of M codes for specifying a spindle positioning angle is always 6. With the extended specification, an arbitrary number of such M codes fr
- Page 5089. SPINDLE SPEED FUNCTION B–63833EN–1/02 4960 M code specifying spindle orientation [Data type] Word [Unit of data] Integer [Valid data range] 6 to 97 Set an M code to change the spindle rotating mode to the spindle positioning mode. Setting the M code performs the spindle orientation. Spindle posit
- Page 509B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE θ represents the basic angular diplacement set in pamrameter No. 4963. 4963 M code for specifying a spindle positioning angle [Data type] Word [Unit of data] deg [Valid data range] 1 to 60 This parameter sets a basic angular displacement used for semi–fi
- Page 5109. SPINDLE SPEED FUNCTION B–63833EN–1/02 4971 Servo loop gain multiplier of the spindle for gear 1 4972 Servo loop gain multiplier of the spindle for gear 2 4973 Servo loop gain multiplier of the spindle for gear 3 4974 Servo loop gain multiplier of the spindle for gear 4 [Data type] Word Set the se
- Page 511B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Alarm and message Number Message Description 053 TOO MANY ADDRESS In the chamfering and corner R com- COMMANDS mands, two or more of I, K and R are specified. Otherwise, the character af- ter a comma(”,”) is not C or R in direct drawing dimensions programming
- Page 5129. SPINDLE SPEED FUNCTION B–63833EN–1/02 Caution CAUTION 1 Feed hold is invalid during spindle positioning. 2 Spindle positioning stops when emergency stop is applied; restart with orientation operation. 3 Dry run, machine lock, and auxiliary function lock are not available during spindle positionin
- Page 513B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.8 Cs CONTOUR CONTROL General The Cs contour control function positions the serial spindle using the spindle motor in conjunction with a dedicated detector mounted on the spindle. This function can perform more accurate positioning than the spindle positioni
- Page 5149. SPINDLE SPEED FUNCTION B–63833EN–1/02 Command Address The address for the move command in Cs contour control is the axis name specified in parameter no.1020. This address is arbitrary. When the second auxiliary function is provided, address B cannot be used for the name of the contour axis. For t
- Page 515B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Reference Position After the serial spindle is switched from spindle speed control to Cs Return of Cs Contour contour control mode, the current position is undefined. Return the Control Axis spindle to the reference position. The reference position return of
- Page 5169. SPINDLE SPEED FUNCTION B–63833EN–1/02 - Interruption of reference position return (i) Manual operation Return to the reference position can be interrupted by reset- ting, emergency stop, or turning off the feed axis and direction select signal. When the interrupted return operation is re- sumed,
- Page 517B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Spindle contour control change completion signal FSCSL
- Page 5189. SPINDLE SPEED FUNCTION B–63833EN–1/02 Clutch/Gear signal Refer to the manual of serial spindle. (Serial spindle) CTH1A, CTH2A These signals determine what parameter (loop gain, etc.) to be used for
- Page 519B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Signals on manual Feed axis and direction select signal +Jn, *Jn
- Page 5209. SPINDLE SPEED FUNCTION B–63833EN–1/02 1020 Name of the axis used for programming for each axis [Data type] Byte axis Set the name of the program axis for each control axis, with one of the values listed in the following table: Axis Set Axis Set Axis Set Axis Set name value name value name value n
- Page 521B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 1023 Number of the servo axis for each axis [Data type] Byte axis Set the servo axis for each control axis. Generally, the same number shall be assigned to the control axis and the corresponding servo axis. Set –1 as the number of servo axis to the Cs contour
- Page 5229. SPINDLE SPEED FUNCTION B–63833EN–1/02 1828 Positioning deviation limit for each axis in movement [Data type] Two–word axis [Unit of data] Detection unit [Valid data range] 0 to 99999999 Set the positioning deviation limit in movement for each axis. 1829 Positioning deviation limit for each axis i
- Page 523B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 3901 Loop gain of the servo axis that interpolates with Cs contour control axis during interpolation (High gear) 3902 Loop gain of the servo axis that interpolates with Cs contour control axis during interpolation (Medium high gear) 3903 Loop gain of the serv
- Page 5249. SPINDLE SPEED FUNCTION B–63833EN–1/02 3920 Number of servo axis that interpolates with Cs contour control [Data type] Byte axis [Valid data range] 0 to 8 Set the number of servo axis that interpolates with Cs contour control axis (3rd group) NOTE When there is no servo axis or less than three ser
- Page 525B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 3931 Loop gain of the servo axis that interpolates with Cs contour control axis during interpolation (High gear) 3932 Loop gain of the servo axis that interpolates with Cs contour control axis during interpolation (Medium high gear) 3933 Loop gain of the serv
- Page 5269. SPINDLE SPEED FUNCTION B–63833EN–1/02 4056 Gear ratio (HIGH) 4057 Gear ratio (MEDIUM HIGH) 4058 Gear ratio (MEDIUM LOW) 4059 Gear ratio (LOW) [Data type] Word axis [Unit of data] (Number of motor rotations to one spindle rotation) 100 [Valid data range] 0 to 32767 Set the gear ratio between spind
- Page 527B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Alarm and message Number Message Description 194 SPINDLE COMMAND IN A contour control mode, spindle positioning SYNCHRO–MODE (Cs–axis control) mode, or rigid tapping mode was specified during the serial spindle synchronous control mode. Correct the pro- gram
- Page 5289. SPINDLE SPEED FUNCTION B–63833EN–1/02 Reference item FANUC SERVO AMPLIFIER ai series DESCRIPTIONS 11.6 Cs Contour Control Function (B–65282EN) FANUC AC SPINDLE MOTOR ai series PARAMETER MANUAL 2.4 Cs Contour Control (B–65280EN) 510
- Page 529B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.9 MULTI–SPINDLE CONTROL General In addition to the conventional (first) spindle, second and third spindles can be controlled. These additional spindles allow two-stage gear changes. A single S code is used to command to any of these spindles. The spindle to
- Page 5309. SPINDLE SPEED FUNCTION B–63833EN–1/02 Basic control (Common An S command is sent as a speed command to each spindle selected, using to TYPE-A and TYPE-B) a spindle selection signal (SWS1 to SWS3
- Page 531B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Multi-spindle control Select Type B control by setting parameter MSI No. 3709#2 to “1”. (TYPE-B) Each spindle has its own SIND, SSIN and SGN signals. Each of these signals functions regardless of selection state of the spindle selection signals (SWS1 to SWS3)
- Page 5329. SPINDLE SPEED FUNCTION B–63833EN–1/02 Connection of spindle Spindle configuration when multi-spindle control is used: · Multi-spindle control · Spindle serial output Necessary parameter · Parameter SS2 (No. 3701#4) = 1 (to use second spindle) · Spindle analog output (to use third spindle) Connect
- Page 533B–63833EN–1/02 9. SPINDLE SPEED FUNCTION D Spindle positioning or When the spindle motor is used for positioning, as in the case of spindle Cs contour control positioning or Cs contour control, the first spindle will allows function as the positioning spindle. Switching to the positioning mode and p
- Page 5349. SPINDLE SPEED FUNCTION B–63833EN–1/02 Individual spindle stop signal *SSTP1, *SSTP2, *SSTP3
- Page 535B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Spindle enable signal ENB2
- Page 5369. SPINDLE SPEED FUNCTION B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G027 *SSTP3 *SSTP2 *SSTP1 SWS3 SWS2 SWS1 G028 PC2SLC GR2 GR1 G029 *SSTP GR31 GR21 G031 G032 R08I R07I R06I R05I R04I R03I R02I R01I G033 SIND SSIN SGN R12I R11I R10I R09I G034 R08I2 R07I2 R06I2 R05I2 R04I2 R03I2 R02I2 R0
- Page 537B–63833EN–1/02 9. SPINDLE SPEED FUNCTION #7 #6 #5 #4 #3 #2 #1 #0 3702 EMS [Data type] Bit EMS Multi–spindle control is 0 : Used 1 : Not used #7 #6 #5 #4 #3 #2 #1 #0 3706 PG2 PG1 GTT PG2 PG1 [Data type] Bit PG2, PG1 Gear ration of spindle to first position coder For the setting, see the description o
- Page 5389. SPINDLE SPEED FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3707 P22 P21 PG2, PG1 (Bits 1 and 0 of parameter No.3702) Gear ratio of spindle to first position coder P22, P21 Gear ratio of spindle to second position coder Magnification PG2, P22 PG1, P21 1 0 0 2 0 1 4 1 0 8 1 1 (Number of spindle
- Page 539B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE 1 When the constant surface speed control option is selected, the spindle speed is clamped at the maximum speed, regardless of whether the G96 mode or G97 mode is specified. 2 When the multi–spindle control option is selected, set the maximum speed for e
- Page 5409. SPINDLE SPEED FUNCTION B–63833EN–1/02 3811 Maximum spindle speed for gear 1 of the second spindle 3812 Maximum spindle speed for gear 2 of the second spindle [Data type] Word [Unit of data] min–1 [Valid data range] 0 to 32767 Set the maximum spindle speed for each gear of the second spindle. NOTE
- Page 541B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 3822 Maximum speed of the third spindle [Data type] Word [Unit of data] min–1 [Valid data range] 0 to 32767 This parameter sets the maximum speed for the third spindle. When a command specifying a speed exceeding the maximum spindle speed is specified, or the
- Page 5429. SPINDLE SPEED FUNCTION B–63833EN–1/02 Warning WARNING Do not switch between the first and second position coders while a function that uses position coder feedback information is being executed. That is, PMC signal PC2SLC
- Page 543B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10 RIGID TAPPING 9.10.1 In a tapping cycle (M series: G84/G74, T series: G84/G88), synchronous control is applied to the tapping operation of a tapping axis and the General operation of the spindle. This capability eliminates the need to use a tool such as
- Page 5449. SPINDLE SPEED FUNCTION B–63833EN–1/02 The descriptions given in this section (such as spindle gear switching and M–type/T–type) are based on the explanation given in Section 9.3. Refer to Section 9.3 as necessary. Specification of The differences in the specifications for rigid tapping for the M
- Page 545B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.2 As shown in the figure below a gear ratio can be inserted between the Connection Among spindle and spindle motor, and between the spindle and position coder. Spindle, Spindle Motor, and Position Coder Spindle control Error Spindle amplifier Spindle mot
- Page 5469. SPINDLE SPEED FUNCTION B–63833EN–1/02 The 1024 or 512 pulses/rev position coder is built into the spindle motor. For the 512 pulses/rev version, specify double the number of teeth on each gear for the position coder. (Double the number of teeth need not be specified for the serial spindle.) 1st s
- Page 547B–63833EN–1/02 9. SPINDLE SPEED FUNCTION S Gear ratio is 1:1, 1:2, 1:4, If the gear ratio is either 1:1, 1:2, 1:4, and 1:8, it is set using parameters 1:8 (VGR=0) PG1 and PG2 (No. 3706 #0, #1). This applies if the position coder is mounted in a spindle or built into a spindle motor when only one sta
- Page 5489. SPINDLE SPEED FUNCTION B–63833EN–1/02 Changing gears during rigid tapping requires a different process from that for gear changes during normal machining. As described above, changing gears conforms to the gear change specifications mentioned in section 9.3 when the M type gear selection method h
- Page 549B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE This table show an example of three gears. For the basic spindle motor speed, refer to the spindle motor description manual. “+ α” means that the spindle motor speed may slightly exceed the basic spindle motor speed. If the M type gear selection method i
- Page 5509. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.10.3 Rigid Tapping Specification D Feed rate In rigid tapping mode, the tapping axis is fed at a rate specified by F. The spindle speed is specified by S 360(deg/min). Use of override is invalid for both of them. An override of 200% can be applied to withdr
- Page 551B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.4 For rigid tapping adjustment, the diagnosis screen displays information Display Data on the related to rigid tapping. Diagnosis Screen For part of the display data, the user can choose between two sets of data items relating to the synchronization of t
- Page 5529. SPINDLE SPEED FUNCTION B–63833EN–1/02 Diagnosis No. 0452 is cleared to “0” when rigid tapping mode is set or canceled, and diagnosis No. 0453 is cleared to “0” in the positioning of the rigid tapping cycle. The following figure shows the tapping axis as the Z axis. Z–axis error Zc Ze Speed 1 1 Zc
- Page 553B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Diagnosis screen D Spindle position deviation 0450 SPINDLE MOTION ERROR Spindle position deviation during rigid tapping [Unit] Pulse D Number of pulses distributed to the spindle 0451 SPINDLE MOTION PULSE Number of pulses distributed to the spindle during rig
- Page 5549. SPINDLE SPEED FUNCTION B–63833EN–1/02 D Spindle–converted move command difference during rigid tapping (momentary value) 0455 SYNC. PULSE(SUM) Momentary spindle–converted move during command difference between the spindle and the tapping axis during rigid tapping [Unit] Pulse NOTE This data item
- Page 555B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.5 Command Format Command format for the The rigid tapping command format for the T series is described below. T series For an explanation of the command format used with the M series, refer to Section II.13.2.2 of the “Operator’s Manual for Machining Cen
- Page 5569. SPINDLE SPEED FUNCTION B–63833EN–1/02 D Specifying M29 and G84 (G88) in the same block (Note, however, that M29 and Mjj for C–axis clamping cannot be specified in the same block.) GjjX (Z) __Z (X) __R__P__F__K__M29****; X (Z) __C__; Rigid X (Z) __C__; tapping · mode · G80; D Converting G84 (G88)
- Page 557B–63833EN–1/02 9. SPINDLE SPEED FUNCTION G84⋅G85 ( Tapping cycle) G84 (G88) (G98 mode) G84 (G88) (G99 mode) Spindle Spindle stop stop Initial point Motion 1 Motion 2 Motion 6 Spindle CW R point Spindle CW R point Spindle Spindle stop stop Motion 3 Motion 5 Spindle CCW Spindle CCW Z (X) point Z(X)poi
- Page 5589. SPINDLE SPEED FUNCTION B–63833EN–1/02 Rigid tapping in feed per Rigid tapping is classified into two types: rigid tapping in feed per rotation mode rotation mode (G99) and rigid tapping in feed per minute mode (G98). Example) The example below specifies rigid tapping in feed per rotation mode for
- Page 559B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.6 Signal 9.10.6.1 Signals for the rigid tapping function Rigid tapping signal RGTAP
- Page 5609. SPINDLE SPEED FUNCTION B–63833EN–1/02 Rigid tapping in–progress signal RTAP
- Page 561B–63833EN–1/02 9. SPINDLE SPEED FUNCTION M series: SF output depends on the gear selection method, as described below. [1] M–type gear selection method SF output depends on bit 6 (SFA) of parameter No. 3705. [2] T–type gear selection method SF output depends on the setting of bit 5 (NSF) of paramete
- Page 5629. SPINDLE SPEED FUNCTION B–63833EN–1/02 Reference information: The table below indicates the relationship between the output signals and gear selection. GR3O GR2O GR1O 1st (low) speed gear × × f 2nd (medium) speed gear × f × 3rd (high) speed gear f × × Gear selection signals (input) GR2, GR1
- Page 563B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.6.4 Signals related to second spindle rigid tapping Gear selection signal See the description of the signals related to gear switching, given above. (input) GR21
- Page 5649. SPINDLE SPEED FUNCTION B–63833EN–1/02 (T series) When bit 7 (SRS) of parameter No. 5200 is set to 1, to select a spindle to be used for rigid tapping, set the signals as indicated below. Signal state Spindle used for rigid tapping RGTSP1 RGTSP2 First spindle “1” “1” or “0” Second spindle “1” “1”
- Page 565B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.6.5 Signal addresses #7 #6 #5 #4 #3 #2 #1 #0 G027 *SSTP2 *SSTP1 SWS2 SWS1 G028 PC2SLC GR2 GR1 G029 GR21 G061 RGTSP2 RGTSP1 RGTAP #7 #6 #5 #4 #3 #2 #1 #0 F001 ENB F007 SF F034 GR3O GR2O GR1O F038 ENB2 F065 RGSPM RGSPP F076 RTAP 9.10.6.6 The following desc
- Page 5669. SPINDLE SPEED FUNCTION B–63833EN–1/02 T–type gear selection When T–type gear selection is used, the PMC must determine whether method gear switching is to be performed, and subsequently perform gear switching as required. For this purpose, each time a spindle–speed function code is specified, the
- Page 567B–63833EN–1/02 9. SPINDLE SPEED FUNCTION D When T–type gear The spindle–speed function strobe signal SF
are output to the PMC. (However, parameter setting is required to enable output of the S codes and SF s - Page 5689. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.10.7 The timing chart for rigid tapping specification depends on the method Timing Charts for Rigid used to specify rigid tapping mode, the gear selection method (M–type or T–type), and whether to perform gear switching. Tapping Specification From the table
- Page 569B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.7.1 When M29 is specified before G84 (G74) M type gear selection method M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle output SF GR1O GR2O GR3O *SSTP SOR RGTAP 250ms or more FIN Rotation Excitation SFR Position l
- Page 5709. SPINDLE SPEED FUNCTION B–63833EN–1/02 M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle *Gear output change motion SF GR1O GR2O GR3O *SSTP SOR RGTAP 250ms or more FIN Rotation Gear change Excitation SFR Position loop Note This time chart show an example wher
- Page 571B–63833EN–1/02 9. SPINDLE SPEED FUNCTION T type gear selection method M29 RTAP First bllock Second block G84 (G74) ENB To be masked to the second block Spindle output SF S code output GR1 GR2 *SSTP SOR RGTAP 250ms or more FIN Rotation Excitation SFR Position loop Fig. 9.10.7.1 (c) Gear change is not
- Page 5729. SPINDLE SPEED FUNCTION B–63833EN–1/02 M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle *Gear output change motion SF S code output GR1 GR2 *SSTP SOR RGTAP 250ms or more FIN Rotation Gear change Excitation SFR Position loop Note This time chart shows an exam
- Page 573B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.7.2 M29 and G84 (G74) are specified in the same block M type gear selection M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle output SF GR1O GR2O GR3O *SSTP SOR RGTAP 250ms or more FIN Rotation Excitation SFR Positi
- Page 5749. SPINDLE SPEED FUNCTION B–63833EN–1/02 M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle output SF GR1O GR2O GR3O *SSTP SOR RGTAP 250ms or more FIN Rotation Gear change Excitation SFR Position loop Note This time chart shows an example where the gear has shif
- Page 575B–63833EN–1/02 9. SPINDLE SPEED FUNCTION T type gear selection method M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle output SF S code output GR1 GR2 *SSTP SOR RGTAP 250ms or more FIN Rotation Excitation SFR Position loop Fig. 9.10.7.2 (c) When gear change is
- Page 5769. SPINDLE SPEED FUNCTION B–63833EN–1/02 M29 RTAP First block Second block G84 (G74) ENB To be masked to the second block Spindle outpout SF S code out- put GR1 GR2 *SSTP SOR RGTAP 250ms or more FIN Rotation Gear change Excitation SFR Position loop Note This time chart shows an example where the gea
- Page 577B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.7.3 Specifying G84 (G74) for rigid tapping by parameters M type gear selection M29 RTAP First block Second block G84 (G74) M29 is commanded internally. ENB To be masked to the second block Spindle output SF GR1O GR2O GR3O *SSTP SOR RGTAP 250ms or more FI
- Page 5789. SPINDLE SPEED FUNCTION B–63833EN–1/02 M29 RTAP First block Second block G84 (G74) M29 is commanded internally. ENB To be masked to the second block Spindle output SF GR1O GR2O GR3O *SSTP SOR RGTAP 250ms or more FIN Rotation Gear change Excitation SFR Position loop Note This time chart shows an ex
- Page 579B–63833EN–1/02 9. SPINDLE SPEED FUNCTION T type gear selection method M29 RTAP First block Second block G84 (G74) M29 is commanded internally. ENB To be masked to the second block Spindle outoput SF S code output GR1 GR2 *SSTP SOR RGTAP 250ms or more FIN Rotation Excitation SFR Position loop Fig. 9.
- Page 5809. SPINDLE SPEED FUNCTION B–63833EN–1/02 M29 RTAP First blcok Second block G84 (G74) M29 is commanded internally ENB To be masked to the second blcok Spindle output SF S code output GR1 GR2 *SSTP SOR RGTAP 250ms or more FIN Rotation Gear change Excitation SFR Position loop Note This time chart shows
- Page 581B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.7.4 When rigid tapping is completed, the mode is canceled if a G code (such Timing to cancel rigid as G80, canned cycle G code, or Group 01 G code) is issued. The S command used during rigid tapping is automatically cleared when tapping mode rigid mode i
- Page 5829. SPINDLE SPEED FUNCTION B–63833EN–1/02 WARNING 1 If rigid tapping mode is canceled by a Group 01 G code, such as G00 or G01, the block containing the G code is executed at the same time the ENB signal is turned to “0”. Therefore, if the block contains an M code for controlling the spindle, an erro
- Page 583B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.10.8 Parameter #7 #6 #5 #4 #3 #2 #1 #0 3705 EVS ESF SFA NSF SGT ESF [Data type] Bit ESF When the spindle control function (S analog output or S serial output) is used, and the consatant surface speed control function is used or bit 7 (GTT) of parameter No.
- Page 5849. SPINDLE SPEED FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3706 PG2 PG1 GTT PG2 PG1 [Data type] Bit PG2, PG1 Gear ratio of spindle to position coder Magnific PG2 PG1 ation 1 0 0 Magnification = 2 0 1 Number of spindle revolutions 4 1 0 Number of position coder revolutions 8 1 1 GTT Selection o
- Page 585B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Spindle motor speed Max. output (4095, 10V) Spindle motor max. clamp speed (Parameter No. 3736) Spindle motor min. clamp speed (Parameter No. 3735) Spindle speed command Max. speed Max. speed Max. speed (S command) at gear1 at gear2 at gear3 parameter paramet
- Page 5869. SPINDLE SPEED FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 SRS FHD DOV SIG CRG VGR G84 5200 FHD PCP DOV SIG CRG VGR G84 [Data type] Bit G84 Method for specifying rigid tapping 0 : An M code specifying the rigid tapping mode is specified prior to the issue of the G84 (or G74) command. (See para
- Page 587B–63833EN–1/02 9. SPINDLE SPEED FUNCTION #7 #6 #5 #4 #3 #2 #1 #0 OV3 OVU TDR 5201 OV3 OVU TDR NIZ [Data type] Bit NIZ Smoothing in rigid tapping is: 0 : Not performed. 1 : Performed. TDR Cutting time constant in rigid tapping 0 : Uses a same parameter during cutting and extraction (Parameter Nos. 52
- Page 5889. SPINDLE SPEED FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 OVS RGS RFF 5203 OVS RFF [Data type] Bit REF Feed forward during movement from the initial point to point R in rigid tapping is: 0 : Disabled. 1 : Enabled. When this parameter is set, the following function is also enabled: D When rigi
- Page 589B–63833EN–1/02 9. SPINDLE SPEED FUNCTION #7 #6 #5 #4 #3 #2 #1 #0 5204 SPR DGN NOTE When this parameter is set, the power must be turned off before operation is continued. [Data type] Bit DGN On the diagnosis screen: 0 : A rigid tapping synchronization error is displayed. (Nos. 455 to 457) 1 : An err
- Page 5909. SPINDLE SPEED FUNCTION B–63833EN–1/02 NOTE When you want to perform rigid tapping, do not set this parameter. If rigid tapping is performed with this parameter set, a tapping tool, workpiece, or machine may be damaged. 5210 Rigid tapping mode specification M code [Data type] Byte [Valid data rang
- Page 591B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 5213 Return or clearance in peck tapping cycle [Data type] Word [Unit of data] Increment system IS–A IS–B IS–C Unit Millimeter input 0.01 0.001 0.0001 mm Input in incluse 0.001 0.0001 0.00001 inch [Valid data range] 0 to 32767 This parameter sets the return o
- Page 5929. SPINDLE SPEED FUNCTION B–63833EN–1/02 5221 Number of spindle gear teeth (first–stage gear) 5222 Number of spindle gear teeth (second–stage gear) 5223 Number of spindle gear teeth (third–stage gear) Number of spindle gear teeth (fourth–stage gear) 5224 5225 Number of second spindle gear teeth (fir
- Page 593B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 5231 Number of position coder gear teeth (first–stage gear) 5232 Number of position coder gear teeth (second–stage gear) 5233 Number of position coder gear teeth (third–stage gear) Number of position coder gear teeth (fourth–stage gear) 5234 5235 Number of po
- Page 5949. SPINDLE SPEED FUNCTION B–63833EN–1/02 5241 Maximum spindle speed in rigid tapping (first–stage gear) 5242 Maximum spindle speed in rigid tapping (second–stage gear) 5243 Maximum spindle speed in rigid tapping (third–stage gear) Maximum spindle speed in rigid tapping (fourth–stage gear) 5244 5245
- Page 595B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Linear acceleration/deceleration time constant for the spindle and tapping axis 5261 (first–stage gear) Linear acceleration/deceleration time constant for the spindle and tapping axis 5262 (second–stage gear) Linear acceleration/deceleration time constant for
- Page 5969. SPINDLE SPEED FUNCTION B–63833EN–1/02 5271 Time constant for the spindle and tapping axis in extraction operation (first–stage gear) Time constant for the spindle and tapping axis in extraction operation 5272 (second–stage gear) 5273 Time constant for the spindle and tapping axis in extraction op
- Page 597B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Position control loop gain for the spindle and tapping axis in rigid tapping 5280 (common to all gears) Position control loop gain for the spindle and tapping axis in rigid tapping 5281 (first–stage gear) Position control loop gain for the spindle and tapping
- Page 5989. SPINDLE SPEED FUNCTION B–63833EN–1/02 5291 Spindle loop gain multiplier in the rigid tapping mode (for gear 1) 5292 Spindle loop gain multiplier in the rigid tapping mode (for gear 2) 5293 Spindle loop gain multiplier in the rigid tapping mode (for gear 3) Spindle loop gain multioplier in the rig
- Page 599B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 5300 Tapping axis in–position width in rigid tapping 5301 Spindle in–position width in rigid tapping [Data type] Word [Unit of data] Detection unit [Valid data range] 1 to 32767 These parameters are used to set tapping axis and spindle in–position widths in r
- Page 6009. SPINDLE SPEED FUNCTION B–63833EN–1/02 5310 Positional deviation limit imposed during tapping axis movement in rigid tapping [Data type] Word [Unit of data] Detection unit [Valid data range] 1 to 32767 This parameter is used to set a positional deviation limit during tapping axis movement in rigid
- Page 601B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE 1 The detection unit is α = La/2048 when the position coder built–in spindle motor uses a position coder of 512 pulses per revolution. 2 When rigid tapping is performed using the second spindle • When the SPR parameter (bit 1 of parameter No.5204) is set
- Page 6029. SPINDLE SPEED FUNCTION B–63833EN–1/02 5314 Positional deviation limit imposed during tapping axis movement in rigid tapping [Data type] 2–word [Unit of data] Detection unit [Valid data range] 0 to 99999999 Usually, parameter No.5310 is used to set a positional deviation limit imposed during tappi
- Page 603B–63833EN–1/02 9. SPINDLE SPEED FUNCTION NOTE When rigid tapping is performed using the second spindle • When the SPR parameter (bit 1 of parameter No.5204) is set to 1, the settings of parameters No.5325 and No.5326 are applied to the second spindle. • When the SPR parameter (bit 1 of parameter No.
- Page 6049. SPINDLE SPEED FUNCTION B–63833EN–1/02 NOTE 1 To use a varied loop gain on a gear–by–gear basis, set parameter No.5341 to 0, and set a loop gain for each gear in parameters No.5342 and No.5343. 2 This parameter is enabled when the SPR parameter (bit 1 of parameter No.5204) is set to 1. Positional
- Page 605B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Positional deviation limit imposed while the spindle is stopped in rigid tapping 5353 using the second spindle [Data type] Word [Unit of data] Detection unit [Valid data range] 1 to 32767 This parameter is used to set a positional deviation limit imposed whil
- Page 6069. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.10.9 Alarm and Message Number Message Description 200 ILLEGAL S CODE COM- In rigid tapping, an S value is out of the MAND range or is not specified. The maximum value for S which can be specified in rigid tapping is set in pa- rameter (No.5241 to 5243). Cha
- Page 607B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Number Message Description 413 SERVO ALARM: n–th The contents of the error register for the AXIS – LSI OVERFLOW n–th axis (axis 1–4 of rigid tapping axis) are beyond the range of –231 to 231. This error usually occurs as the result of an improperly set parame
- Page 6089. SPINDLE SPEED FUNCTION B–63833EN–1/02 NOTE 1 A spindle pitch error is not compensated for in rigid tapping mode. Drift compensation is not made with an analog spindle. 2 The maximum number of pulses that can be distributed to the spindle is: ⋅ 32,767 pulses per 8 msec for a serial spindle ⋅ 4,096
- Page 609B–63833EN–1/02 9. SPINDLE SPEED FUNCTION CAUTION (continued) 3 When the Cs contouring control function for the serial spindle is used together with the rigid tapping function, the same motor is used for spindle rotation control, Cs contouring control, and rigid tapping modes. The following points mu
- Page 6109. SPINDLE SPEED FUNCTION B–63833EN–1/02 ⋅ When the spindle is an analog spindle, the loop gains of the spindle and tapping axis are switched according to the values set in these parameters. ⋅ When the spindle is a serial spindle, the loop gain of the tapping axis is switched according to the values
- Page 611B–63833EN–1/02 9. SPINDLE SPEED FUNCTION CAUTION 1 Set a loop gain for spindle position control in rigid tapping using a serial spindle. In these parameters, basically, set the same values as those set in parameter Nos. 5280 and 5281 to 5284 (loop gains for position control of the tapping axis). Whi
- Page 6129. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.11 SPINDLE SYNCHRONOUS CONTROL General This function enables the synchronous control of two spindles. It also enables the control of the rotation phase of a spindle, allowing non–standard workpieces as well as rods to be held by either of the two spindles.
- Page 613B–63833EN–1/02 9. SPINDLE SPEED FUNCTION D Constant surface speed control can be executed in synchronization control even while a workpiece is being held with the two spindles. However, if the speed is to change in excess of the specified time constant, the speed changes within the extent specified
- Page 6149. SPINDLE SPEED FUNCTION B–63833EN–1/02 D In spindle synchronization control , the compensation value for spindle speed offset (parameter No. 3731) is disabled. D A spindle–phase synchronous control command is effective only in synchronous spindle control mode. The specified phase can be repeatedly
- Page 615B–63833EN–1/02 9. SPINDLE SPEED FUNCTION This parameter is used to output the inter–spindle phase error detection signal SYCAL in the serial spindle synchronization control mode. The SYCAL
- Page 6169. SPINDLE SPEED FUNCTION B–63833EN–1/02 9.12 SPINDLE ORIENTATION General This function stops the spindle at a specified position. The spindle can be stopped in either of the following two ways. · The spindle is stopped using mechanical stop. · The spindle is stopped by applying a function of the sp
- Page 617B–63833EN–1/02 9. SPINDLE SPEED FUNCTION Signal address #7 #6 #5 #4 #3 #2 #1 #0 G078 SHA07 SHA06 SHA05 SHA04 SHA03 SHA02 SHA01 SHA00 G079 SHA11 SHA10 SHA09 SHA08 G080 SHB07 SHB06 SHB05 SHB04 SHB03 SHB02 SHB01 SHB00 G081 SHB11 SHB10 SHB09 SHB08 Parameter #7 #6 #5 #4 #3 #2 #1 #0 3702 OR2 OR1 [Data typ
- Page 6189. SPINDLE SPEED FUNCTION B–63833EN–1/02 Reference item FANUC SERVO AMPLIFIER Position coder method spindle orientation 11.1 ai series DESCRIPTIONS Magnetic sensor method spindle 11.2 (B–65282EN) orientation FANUC AC SPINDLE Position coder method spindle orientation MOTOR ai series 2.1 Magnetic sens
- Page 619B–63833EN–1/02 9. SPINDLE SPEED FUNCTION 9.13 SPINDLE OUTPUT SWITCHING General Spindle output switching switches between the two motor windings, one for low speed and the other for high speed, incorporated into the special spindle motors. This ensures that the spindle motor demonstrates stable outpu
- Page 6209. SPINDLE SPEED FUNCTION B–63833EN–1/02 D When gear selection output signals, GR2O and GR1O
, are used (for machining centers in which constant surface speed control is not provided and GTT, bit 4 of parameter No. 3706, is set to 0) Set two gears, which are almost the same. (Example: V - Page 621B–63833EN–1/02 10. TOOL FUNCTIONS 10 TOOL FUNCTIONS 603
- Page 62210. TOOL FUNCTIONS B–63833EN–1/02 10.1 TOOL FUNCTION General D M series Selection of tools can be done by commanding tool numbers with up to an 8-digit numeral after address T. D T series Selection of tools and offset amounts can be done by commanding tool numbers and offset numbers with up to an 8-
- Page 623B–63833EN–1/02 10. TOOL FUNCTIONS #7 #6 #5 #4 #3 #2 #1 #0 5002 LGN LD1 [Data type] Bit LD1 Wear offset number of tool offset 0 : Specified using the lower two digits of a T code 1 : Specified using the lower one digit of a T code LGN Geometry offset number of tool offset 0 : Is the same as wear offs
- Page 62410. TOOL FUNCTIONS B–63833EN–1/02 Note NOTE When a move command and a tool function are specified in the same block, the commands are executed in one of the following two ways: (i) Simultaneous execution of the move command and tool function commands. (ii) Executing tool function commands upon compl
- Page 625B–63833EN–1/02 10. TOOL FUNCTIONS 10.2 TOOL COMPENSATION VALUE/ TOOL COMPENSATION NUMBER/ TOOL COMPENSATION MEMORY 10.2.1 Tool Compensation Value/Tool Compensation Number/Tool Compensation Memory General (M series) Tool compensation values include tool geometry compensation values and tool wear comp
- Page 62610. TOOL FUNCTIONS B–63833EN–1/02 D Tool compensation (1) Tool compensation memory C memory Memory for geometry compensation and wear compensation is sepa- rate in tool compensation memory C. Geometry compensation and wear compensation can thus be set separately. Separate memories are prepared for c
- Page 627B–63833EN–1/02 10. TOOL FUNCTIONS D Tool compensation The memory can hold 64 sets of tool compensation values. number D Tool compensation Memory for geometry compensation and wear compensation is prepared memory separately. Geometry compensation and wear compensation can thus be set separately. The
- Page 62810. TOOL FUNCTIONS B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 3109 DWT [Data type] Bit DWT Characters G and W in the display of tool wear/geometry compensation amount 0 : The characters are displayed at the left of each number. 1 : The characters are not displayed. #7 #6 #5 #4 #3 #2 #1 #0 3205
- Page 629B–63833EN–1/02 10. TOOL FUNCTIONS Bit 0 (WOF) of parameter No. 3290 = 1 (Disables tool wear compensation value modification.) Parameter No. 3294 = 100 Parameter No. 3295 = 11 If bit 0 (WOF) of parameter No. 3290 is set to 0, the modification of the tool geometry compensation values alone is disabled
- Page 63010. TOOL FUNCTIONS B–63833EN–1/02 5013 Maximum value of tool wear compensation [Data type] Two–word [Unit of data] Increment system IS–A IS–B IS–C Unit Metric input 0.01 0.001 0.0001 mm Inch input 0.001 0.0001 0.00001 inch [Valid data range] Increment system IS–A IS–B IS–C Metric input 0 to 99999 0
- Page 631B–63833EN–1/02 10. TOOL FUNCTIONS Alarm and message Number Message Description 032 ILLEGAL OFFSET VALUE In setting an offset amount by G10 or IN G10 in writing an offset amount by system variables, the offset amount was ex- cessive. 5300 SET ALL OFFSET DATAS After the inch/metric automatic con- AGAI
- Page 63210. TOOL FUNCTIONS B–63833EN–1/02 10.3 TOOL LIFE MANAGEMENT 10.3.1 Tool life management General When tools are classified into several groups, average tool life (No. of uses or time) is designated for each group. Whenever a tool is used, the usage time is subtracted from the tool life; when the tool
- Page 633B–63833EN–1/02 10. TOOL FUNCTIONS Tool change reset signal TLRST
- Page 63410. TOOL FUNCTIONS B–63833EN–1/02 Tool skip signal TLSKP
- Page 635B–63833EN–1/02 10. TOOL FUNCTIONS T code output Tool function strobe signal TF New tool selecting signal TLNW End signal FIN Tool group number select signal TL01 to TL256 (M series)
- Page 63610. TOOL FUNCTIONS B–63833EN–1/02 ȍ {2 9 i Override value = Vi} i+0 *TLV0 0.1 *TLV1 0.2 *TLV2 0.4 *TLV3 0.8 *TLV4 1.6 *TLV5 3.2 *TLV6 6.4 *TLV7 12.8 *TLV8 25.6 *TLV9 51.2 (Example) When *TLV7, *TLV6, and *TLV3 are set to “0”, the override value is calculated as follows: 12.8 + 6.4 + 0.8 = 20.0 The l
- Page 637B–63833EN–1/02 10. TOOL FUNCTIONS Parameter #7 #6 #5 #4 #3 #2 #1 #0 6800 SNG GRS SIG LTM GS2 GS1 M6T IGI SNG GRS SIG LTM GS2 GS1 [Data type] Bit GS1, GS2 This parameter sets the combination of the number of tool life groups which can be entered, and the number of tools which can be entered per group
- Page 63810. TOOL FUNCTIONS B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 6801 EXG TSM M6E EXT EMD LFV [Data type] Bit TSM When a tool takes several tool numbers, life is counted in tool life management: 0 : For each of the same tool numbers. 1 : For each tool. LFV Specifies whether life count override is enabled o
- Page 639B–63833EN–1/02 10. TOOL FUNCTIONS Example: When the LTM parameter (bit 2 of parameter No.6800) is set to 0 G10 L3 ; P1 L10 Q1 ; (Q1: The life of group 1 is specified as a count.) : P2 L20 Q2 ; (Q2: The life of group 2 is specified as a duration.) : P3 L20 ; (Omission of Q: The life of group 3 is spe
- Page 64010. TOOL FUNCTIONS B–63833EN–1/02 Alarm and message Number Message Description 149 FORMAT ERROR IN G10L3 A code other than Q1,Q2,P1 or P2 was spe- cified as the life count type in the extended tool life management. 150 ILLEGAL TOOL GROUP Tool Group No. exceeds the maximum allow- NUMBER able value. M
- Page 641B–63833EN–1/02 10. TOOL FUNCTIONS 10.3.2 Tool Life Arrival Notice Signal (M Series) General Once the remaining life of tools (to be kept used until new tools are selected) is set up for each group, it becomes possible to check the remaining tool life for the groups. When the actual remaining life of
- Page 64210. TOOL FUNCTIONS B–63833EN–1/02 10.4 CUTTER COMPENSATION 10.4.1 Cutter Compensation C (M Series) General When the tool is moved, the tool path can be shifted by the radius of the tool. To make an offset as large as the radius of the tool, first create an offset vector with a length equal to the ra
- Page 643B–63833EN–1/02 10. TOOL FUNCTIONS Parameter #7 #6 #5 #4 #3 #2 #1 #0 5001 OFH [Data type] Bit OFH Offset number of tool length compensation, cutter compensation and tool offset 0 : Specifies the tool length compensation using an H code, and cutter compensation C using a D code Tool offset conforms to
- Page 64410. TOOL FUNCTIONS B–63833EN–1/02 G39 The corner rounding function (G39) in cutter compensation C mode is: 0 : Disabled. 1 : Enabled. CNV The interference check and vector erasure of cutter compensation C (M series) or tool–nose radius compensation (T series) are: 0 : Performed. 1 : Not performed. M
- Page 645B–63833EN–1/02 10. TOOL FUNCTIONS [FS15 format] B Start point A End point Center If the end point is in the A region separated by the line L drawn between the start point and the center, the movement is made along the shortcut. If the end point is in the B re- gion, almost a single turn is made. NOT
- Page 64610. TOOL FUNCTIONS B–63833EN–1/02 Alarm and message Number Message Description 033 NO SOLUTION AT CRC A point of intersection cannot be deter- mined for cutter compensation C. Modify the program. 034 NO CIRC ALLOWED IN The start up or cancel was going to be ST–UP /EXT BLK performed in the G02 or G03
- Page 647B–63833EN–1/02 10. TOOL FUNCTIONS 10.4.2 Tool Nose Radius Compensation (T Series) General It is difficult to produce the compensation necessary to form accurate parts when using only the tool offset function due to tool nose roundness in taper cutting or circular cutting. The tool nose radius compen
- Page 64810. TOOL FUNCTIONS B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 5003 CCN [Data type] Bit CCN When automatic reference position return (G28) is specified in the cutter compensation C mode (M series) or in tool nose radius compensation (T series): 0 : The cutter compensation vector is cancelled in movement
- Page 649B–63833EN–1/02 10. TOOL FUNCTIONS [FS16 format] C B Start point D A End point Center If the end point viewed from the start point is in the A region, the movement is made along the shortcut. If the end point is in the B, C, or D region, almost a single turn is made. [FS15 format] B Start point A End
- Page 65010. TOOL FUNCTIONS B–63833EN–1/02 Alarm and message Number Message Description 033 NO SOLUTION AT CRC A point of intersection cannot be deter- mined for tool nose radius compensa- tion. Modify the program. Modify the program. 034 NO CIRC ALLOWED IN The start up or cancel was going to be ST–UP /EXT B
- Page 651B–63833EN–1/02 11. PROGRAM COMMAND 11 PROGRAM COMMAND 633
- Page 65211. PROGRAM COMMAND B–63833EN–1/02 11.1 DECIMAL POINT PROGRAMMING/ POCKET CALCULATOR TYPE DECIMAL POINT PROGRAMMING General Numerical values can be entered with a decimal point. A decimal point can be used when entering a distance, time, or speed. Decimal points can be specified with the following a
- Page 653B–63833EN–1/02 11. PROGRAM COMMAND #7 #6 #5 #4 #3 #2 #1 #0 3455 AXD [Data type] Bit axis AXD If a decimal point is omitted for an address with which a decimal point can be used, the value is determined: 0 : In accordance with the least input increment. 1 : In millimeters, inches, or seconds. (calcul
- Page 65411. PROGRAM COMMAND B–63833EN–1/02 11.2 G CODE SYSTEM (T SERIES) General There are three G code systems : A,B, and C (Table 11.2). Select a G code system using parameter GSC (No. 3401#7) and parameter GSB (No. 3401#6). Table 11.2 G code list for T series (1/3) G code Group Function A B C G00 G00 G00
- Page 655B–63833EN–1/02 11. PROGRAM COMMAND Table 11.2 G code list for T series (2/3) G code Group Function A B C Automatic tool compensation X (When the bit 3 (G36) of G36 G36 G36 parameter No. 3405 is set to 0) G37 G37 G37 Automatic tool compensation Z 00 G37.1 G37.1 G37.1 Automatic tool compensation X G37
- Page 65611. PROGRAM COMMAND B–63833EN–1/02 Table 11.2 G code list for T series (3/3) G code Group Function A B C G71 G71 G72 Traverse grinding cycle (for grinding machine) Traverse direct constant–dimension grinding cycle G72 G72 G73 01 (for grinding machine) G73 G73 G74 Oscilation grinding cycle (for grind
- Page 657B–63833EN–1/02 11. PROGRAM COMMAND Parameter #7 #6 #5 #4 #3 #2 #1 #0 3401 GSC GSB [Data type] Bit GSB, GSC The G code system is set. GSC GSB G code 0 0 G code system A 0 1 G code system B 1 0 G code system C #7 #6 #5 #4 #3 #2 #1 #0 3402 CLR G91 G01 [Data type] Bit G01 Mode entered when the power is
- Page 65811. PROGRAM COMMAND B–63833EN–1/02 Note NOTE 1 If the CNC enters the clear state (see bit 6 (CLR) of parameter 3402) when the power is turned on or the CNC is reset, the modal G codes change as follows. (1) G codes marked with in Table 11.2 are enabled. (2) When the system is cleared due to power-on
- Page 659B–63833EN–1/02 11. PROGRAM COMMAND Reference item PREPARATORY II.3 FUNCTION (G FUNCTION) OPERATOR’S MANUAL STATUS WHEN TURNING Series 0i–B (T series) (B–63834EN) POWER ON, WHEN APPENDIX E CLEAR AND WHEN RESET PREPARATORY II.3 FUNCTION (G FUNCTION) OPERATOR’S MANUAL STATUS WHEN TURNING Series 0i Mate
- Page 66011. PROGRAM COMMAND B–63833EN–1/02 11.3 PROGRAM CONFIGURATION General A program consists of the following components: Table 11.3 Program components Components Descriptions Tape start Symbol indicating the start of a program file Leader section Used for the title of a program file, etc. Program start
- Page 661B–63833EN–1/02 11. PROGRAM COMMAND Parameter #7 #6 #5 #4 #3 #2 #1 #0 0100 CTV This parameter can be set at “Setting Screen.” [Data type] Bit CTV: Character counting for TV check in the comment section of a program. 0 : Not performed 1 : Performed #7 #6 #5 #4 #3 #2 #1 #0 3201 NPE N99 [Data type] Bit
- Page 66211. PROGRAM COMMAND B–63833EN–1/02 Alarm and message Number Message Description 001 TH PARITY ALARM TH alarm (A character with incorrect parity was input). 002 TV PARITY ALARM TV alarm (The number of characters in a block is odd). This alarm will be gener- ated only when the TV check is effective (w
- Page 663B–63833EN–1/02 11. PROGRAM COMMAND 11.4 INCH/METRIC CONVERSION General Either inch or metric input can be selected by G code. Signal Inch input signal INCH
- Page 66411. PROGRAM COMMAND B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 1006 ROSx ROTx NOTE When this parameter is changed, turn off the power before continuing operation. [Data type] Bit axis ROTx, ROSx Setting linear or rotation axis ROSx ROTx Description 0 0 Linear axis @ Inch/metric conversion is done. @ All
- Page 665B–63833EN–1/02 11. PROGRAM COMMAND NOTE M series are not equipped with this parameter. Cutting feedrates are specified by F commands in units of 0.001 mm/min for millimeter machines or 0.00001 inches/min for inch machines. #7 #6 #5 #4 #3 #2 #1 #0 3104 MCN [Data type] Bit MCN Machine position is: 0 :
- Page 66611. PROGRAM COMMAND B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 8003 PIM [Data type] Bit PIM When only the axes controlled by the PMC are used, the linear axis is: 0 : Influenced by inch/millimeter input. 1 : Not influenced by inch/millimeter input. Warning WARNING When switching inch input (G20) to metr
- Page 667B–63833EN–1/02 11. PROGRAM COMMAND 11.5 CUSTOM MACRO 11.5.1 Custom Macro General Although subprograms are useful for repeating the same operation, the custom macro function also allows use of variables, arithmetic and logic operations, and conditional branches for easy development of general program
- Page 66811. PROGRAM COMMAND B–63833EN–1/02 P : Macro number of bolt hole circle r : Radius α : Start angle β : Angle between circles k : Number of circles Signal Custom Macro Input Signal UI000 to UI015
- Page 669B–63833EN–1/02 11. PROGRAM COMMAND [Function] No function is provided for the control unit. These signals can be read or written by a custom macro as a type of system variable, and are used for interface signals between custom macros and the PMC. These signals correspond to system variables as indic
- Page 67011. PROGRAM COMMAND B–63833EN–1/02 Parameter D Settings for executing single block stop and custom macros #7 #6 #5 #4 #3 #2 #1 #0 6000 SBV SBM HGO HMC MGO [Data type] Bit MGO When a GOTO statement for specifying custom macro control is executed, a high–speed branch to 20 sequence numbers executed fr
- Page 671B–63833EN–1/02 11. PROGRAM COMMAND SBV Custom macro statement 0 : Not stop the single block 1 : Stops the single block To control single blocks in custom macro statements using system variable #3003, use this parameter to enable or disable single blocks in custom macro statements. This bit is valid
- Page 67211. PROGRAM COMMAND B–63833EN–1/02 *0 to *7 Set the hole pattern of an EIA code indicating *. =0 to =7 Set the hole pattern of an EIA code indicating =. #0 to#7 Set the hole pattern of an EIA code indicating #. [0 to [7 Set the hole pattern of an EIA code indicating [. ]0 to ]7 Set the hole pattern
- Page 673B–63833EN–1/02 11. PROGRAM COMMAND NOTE Setting value 0 is invalid. No custom macro can be called by G00. D Setting M codes that call subprograms of program Nos.9001 to 9009 6071 M code that calls the subprogram of program number 9001 6072 M code that calls the subprogram of program number 9002 6073
- Page 67411. PROGRAM COMMAND B–63833EN–1/02 D Setting M codes that call custom macros of no.9020 to 9029 6080 M code that calls the custom macro of program number 9020 6081 M code that calls the custom macro of program number 9021 6082 M code that calls the custom macro of program number 9022 6083 M code tha
- Page 675B–63833EN–1/02 11. PROGRAM COMMAND Alarm and message Number Message Description 076 ADDRESS P NOT Address P (program number) was not com- DEFINED manded in the block which includes an M98, G65, or G66 command. Modify the program. 077 SUB PROGRAM The subprogram was called in five folds. NESTING ERROR
- Page 67611. PROGRAM COMMAND B–63833EN–1/02 Number Message Description 124 MISSING END DO – END does not correspond to 1 : 1. STATEMENT Modify the program. 125 FORMAT ERROR IN
format is erroneous. Modify the MACRO program. 126 ILLEGAL LOOP NUMBER In DOn, 1x n x 3 is not established. Modify the prog - Page 677B–63833EN–1/02 11. PROGRAM COMMAND 11.5.2 Interruption Type Custom Macro General When a program is being executed, another program can be called by inputting an interrupt signal (UINT) from the machine. This function is referred to as an interruption type custom macro function. Program an interrupt
- Page 67811. PROGRAM COMMAND B–63833EN–1/02 When M96Pxxxx is specified in a program, subsequent program operation can be interrupted by an interrupt signal (UINT) input to execute the program specified by Pxxxx. Any interrupt signal (UNIT, asterisked in Fig. 11.5.2) issued after M97 is ignored. Do not enter
- Page 679B–63833EN–1/02 11. PROGRAM COMMAND MPR Custom macro interrupt valid/invalid M code 0 : M96/M97 1 : M code set using parameters (Nos. 6033 and 6034) MSB Interrupt program 0 : Uses a dedicated local variable (Macro–type interrupt) 1 : Uses the same local variable as in the main program (Subprogram– ty
- Page 68011. PROGRAM COMMAND B–63833EN–1/02 Reference item OPERATOR’S MANUAL II.15.11 Interruption type custom macro (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.15.11 Interruption type custom macro (T series) (B–63834EN) OPERATOR’S MANUAL II.15.11 Interruption type custom macro (M series) (B–6386
- Page 681B–63833EN–1/02 11. PROGRAM COMMAND 11.6 CANNED CYCLE (M SERIES)/CANNED CYCLE FOR DRILLING (T SERIES) General Canned cycles make it easier for the programmer to create programs. With a canned cycle, a frequently–used machining operation can be specified in a single block with a G function; without ca
- Page 68211. PROGRAM COMMAND B–63833EN–1/02 SPINDLE CONTROL In some canned cycles, a spindle command to rotate the spindle in reverse direction may be output. The following canned cycles require spindle control: M series T series Reverse tapping cycle G74 Face tapping cycle (G84) Fine boring cycle G76 Side t
- Page 683B–63833EN–1/02 11. PROGRAM COMMAND D G74 (Counter tapping cycle) X, Y Z Z Z Dwell Dwell (Note) (Note) Note) It is possible to not output M05 M03 M05 M04 M05 code by using parame- ter M5T (No. 5101#6). MF MF MF MF Next block (G98 mode) FIN FIN FIN FIN Next block (G99 mode) D G76 (Fine boring cycle) X
- Page 68411. PROGRAM COMMAND B–63833EN–1/02 D G86 (Boring cycle) X, Y Return to initial level in G98 mode Z Z M05 M03 M03 MF MF MF FIN FIN FIN Next block (G98 mode) D G87 (Back boring cycle) Next block (G99 mode) X or Y X or Y X, Y X or Y Z Z Z Dwell (Note 2) (Note 2) M05 M19 M03 M05 M19 M03 MF MF MF MF MF M
- Page 685B–63833EN–1/02 11. PROGRAM COMMAND D G84 (Face tapping cycle) G88 (Side tapping cycle) X, C (Z, C) Z (X) Z (X) Z Z (X) Dwell Dwell (Note 1) (Note 2) (Note 1) (Note 2) M05 M04 M05 M03 MF MF MF MF Next block (G98 mode) (Note 1) When parameter M5T FIN FIN FIN FIN (No. 5101#6)=0, M05 is not output. Next
- Page 68611. PROGRAM COMMAND B–63833EN–1/02 Signal Tapping signal TAP
- Page 687B–63833EN–1/02 11. PROGRAM COMMAND RD2, RD1 Set the axis and direction in which the tool in drilling canned cycle G76 or G87 is got free. RD2 and RD1 are set as shown below by plane selection. RD2 RD1 G17 G18 G19 0 0 +X +Z +Y 0 1 –X –Z –Y 1 0 +Y +X +Z 1 1 –Y –X –Z M5T When a spindle rotates from the
- Page 68811. PROGRAM COMMAND B–63833EN–1/02 5110 C–axis clamp M code in drilling canned cycle [Data type] Byte [Valid data range] 0 to 99 This parameter sets the C–axis clamp M code in a drilling canned cycle. 5111 Dwell time when C–axis unclamping is specified in drilling canned cycle [Data type] Word [Unit
- Page 689B–63833EN–1/02 11. PROGRAM COMMAND 5114 Return or clearance value of drilling canned cycle G83 Return value of high–speed peck drilling cycle G73 [Data type] Word [Unit of data] Increment system IS-A IS-B IS-C Unit Metric input 0.01 0.001 0.001 mm Inch input 0.001 0.0001 0.0001 inch [Valid data rang
- Page 69011. PROGRAM COMMAND B–63833EN–1/02 5115 Clearance canned cycle G83 [Data type] Word [Unit of data] Increment system IS-A IS-B IS-C Unit Metric input 0.01 0.001 0.001 mm Inch input 0.001 0.0001 0.0001 inch [Valid data range] 0 to 32767 G83 for M series q : Depth of cut d : Clearance value R point q d
- Page 691B–63833EN–1/02 11. PROGRAM COMMAND Reference item OPERATOR’S MANUAL II.13.1 Canned cycle (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL II.13.3 Canned cycle for hole machining (T series) (B–63834EN) OPERATOR’S MANUAL Series 0i Mate–B II.13.1 Canned cycle (M series) (B–63864EN) 673
- Page 69211. PROGRAM COMMAND B–63833EN–1/02 11.7 EXTERNAL MOTION FUNCTION (M SERIES) General Upon completion of positioning in each block in the program, an external operation function signal can be output to allow the machine to perform specific operation. G81 IP_ ; (The IP_ is axis move command ) Every tim
- Page 693B–63833EN–1/02 11. PROGRAM COMMAND Signal External Operation Signal EF
- Page 69411. PROGRAM COMMAND B–63833EN–1/02 11.8 CANNED CYCLE (T SERIES)/MULTIPLE REPETITIVE CANNED CYCLE (T SERIES) General The option canned cycles makes CNC programming easy. For instance, the data of the finish work shape describes the tool path for rough machining. And also, a canned cycles for the thre
- Page 695B–63833EN–1/02 11. PROGRAM COMMAND Signal Chamfering signal CDZ
- Page 69611. PROGRAM COMMAND B–63833EN–1/02 QSR Before a multiple repetitive canned cycle (G70 to G73) is started, a check to see if the program contains a block that has the sequence number specified in address Q is: 0 : Not made. 1 : Made. (If the sequence number specified in address Q cannot be found, an
- Page 697B–63833EN–1/02 11. PROGRAM COMMAND D Escape in multiple repetitive canned cycles G73 5135 Escape in multiple repetitive canned cycle G73 in X–axis direction 5136 Escape in multiple repetitive canned cycle G73 in Z–axis direction [Data type] Two–word [Unit of data] Increment system IS-A IS-B IS-C Uni
- Page 69811. PROGRAM COMMAND B–63833EN–1/02 D Minimum depth of cut in multiple repetitive canned cycle G76 5140 Minimum depth of cut in multiple repetitive canned cycle G76 [Data type] Two–word [Unit of data] Increment system IS-A IS-B IS-C Unit Metric input 0.01 0.001 0.001 mm Inch input 0.001 0.0001 0.0001
- Page 699B–63833EN–1/02 11. PROGRAM COMMAND Alarm and message Number Message Description 061 ADDRESS P/Q NOT Address P or Q is not specified in G70, FOUND IN G70–G73 G71, G72, or G73 command. Modify the program. 062 ILLEGAL COMMAND IN 1 The depth of cut in G71 or G72 is zero or G71–G76 negative value. 2 The
- Page 70011. PROGRAM COMMAND B–63833EN–1/02 Cautions for multiple 1 Necessary parameters (such as P, Q, X, Z, U, W, and R) must be set repetitive canned cycle correctly for an individual block that specifies a multiple repetitive (G70 to G76) canned cycle. 2 In G71, G72, and G73 blocks having a sequence numb
- Page 701B–63833EN–1/02 11. PROGRAM COMMAND Reference item OPERATOR’S MANUAL II.13.1 Canned cycle Series 0i–B (T series) (B–63834EN) II.13.2 Multiple repetitive canned cycle OPERATOR’S MANUAL II.13.1 Canned cycle Series 0i Mate–B (T series) (B–63854EN) II.13.2 Multiple repetitive canned cycle 683
- Page 70211. PROGRAM COMMAND B–63833EN–1/02 11.9 INDEX TABLE INDEXING FUNCTION (M SERIES) General Indexing the table on a machining center is a complished by specifying a positioning angle. Before and after indexing, the table is automatically unclamped or clamped . Basic Procedure The control axis that inde
- Page 703B–63833EN–1/02 11. PROGRAM COMMAND (9) On the PMC side, when BCLP changes to “0”, *BECLP is set to “1”. This completes the sequence. The time charts for these operations are shown in the figures below. (1) (2) (3) (4) (5) (6) (7) (8) (9) B command (independent) Bbbbb B axis servo on for position con
- Page 70411. PROGRAM COMMAND B–63833EN–1/02 B axis manual feed selection signal +Jb*1
B axis position control servo ON B axis unclamp signal BUCLP B axis return completion signal ZPb*1 - Page 705B–63833EN–1/02 11. PROGRAM COMMAND Signal B axis clamp signal BCLP
- Page 70611. PROGRAM COMMAND B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G038 *BECLP *BEUCP #7 #6 #5 #4 #3 #2 #1 #0 F061 BCLP BUCLP Parameter D Setting linear or rotation axis #7 #6 #5 #4 #3 #2 #1 #0 1006 ROSx ROTx [Data type] Bit axis ROTx, ROSx Define linear or rotation axis ROSx ROTx Description
- Page 707B–63833EN–1/02 11. PROGRAM COMMAND D Setting for positioning the index table #7 #6 #5 #4 #3 #2 #1 #0 5500 IDX SIM G90 INC ABS REL DDP [Data type] Bit DDP Definition of index values 0 : Conventional method (Example IS–B: B1; = 0.001 deg) 1 : Calculator method (Example IS–B: B1; = 1.000 deg) REL Relat
- Page 70811. PROGRAM COMMAND B–63833EN–1/02 D Negative direction rotation command M code 5511 Negative direction rotation command M code [Data type] Byte [Valid data range] 0 to 255 0 : No M code is defined to set the index table rotation to the negative direction. The rotation direction is specified using a
- Page 709B–63833EN–1/02 11. PROGRAM COMMAND Caution CAUTION 1 The secondary auxiliary function can be used, but its address must be different from that of the indexing axis. 2 If the incremental command is used for indexing of the index table, the workpiece zero point offset value on the index table axis mus
- Page 71011. PROGRAM COMMAND B–63833EN–1/02 Reference Item OPERATOR’S MANUAL Series 0i–B II.13.8 Index table indexing function (M series) (B–63844EN) 692
- Page 711B–63833EN–1/02 11. PROGRAM COMMAND 11.10 SCALING (M SERIES) General A programmed figure can be magnified or reduced (scaling). The dimensions specified with X_, Y_, and Z_ can each be magnified or reduced with the same or different rates of magnification. The magnification rate can be specified in t
- Page 71211. PROGRAM COMMAND B–63833EN–1/02 D Scaling of each axis, Each axis can be scaled by different magnifications. Also when a negative programmable mirror magnification is specified, a mirror image is applied. First of all, set a image (negative parameter XSC (No. 5400#6) which validates each axis sca
- Page 713B–63833EN–1/02 11. PROGRAM COMMAND Parameter D Setting valid/invalid and magnification of scaling #7 #6 #5 #4 #3 #2 #1 #0 5400 SCR XSC [Data type] Bit XSC Axis scaling and programmable mirror image 0 : Not active (The scaling magnification is specified by P.) 1 : Active SCR Scaling magnification uni
- Page 71411. PROGRAM COMMAND B–63833EN–1/02 D Scaling magnification for every axis 5421 Scaling magnification for every axis This parameter can be set at “Setting Screen.” [Data type] Two–word axis [Unit of data] 0.001 or 0.00001 times (Selected using SCR, #7 of parameter No. 5400) [Valid data range] *999999
- Page 715B–63833EN–1/02 11. PROGRAM COMMAND 11.11 COORDINATE SYSTEM ROTATION General A programmed shape can be rotated. By using this function it is possible to modify a program using a rotation command. This is useful when a workpiece has been placed with some angle rotated from the programmed position on t
- Page 71611. PROGRAM COMMAND B–63833EN–1/02 Rotation plane G17 Y Center of Angle of rotation rotation R (α,β) X 0 Fig. 11.11 (b) Coordinate system rotation Parameter D Angle specification method of coordinate system rotation #7 #6 #5 #4 #3 #2 #1 #0 5400 RIN [Data type] Bit RIN Coordinate rotation angle comma
- Page 717B–63833EN–1/02 11. PROGRAM COMMAND Alarm and message Number Message Description 144 ILLEGAL PLANE SE- The coordinate rotation plane and arc LECTED or cutter compensation C plane must be the same. Modify the program. 5302 ILLEGAL COMMAND IN A command to set the coordinate sys- G68 MODE tem is specifi
- Page 71811. PROGRAM COMMAND B–63833EN–1/02 11.12 MACRO COMPILER/ EXECUTER General There are two types of NC programs; those which, rarely changed, and those that changed with every execution. These programs are created by the custom macro. The custom macro is an executable form of a part program created by
- Page 719B–63833EN–1/02 11. PROGRAM COMMAND 11.13 SMALL HOLE PECK DRILLING CYCLE (M SERIES) General In peck drilling, the tool enters and retracts from hole based on an overload torque detection signal (skip signal) until the designed hole depth is reached. The spindle speed and cutting feedrate are changed
- Page 72011. PROGRAM COMMAND B–63833EN–1/02 D Changing of cutting The cutting feedrate programmed with the F word is changed during the feedrate second and subsequent cutting operations. Parameter Nos. 5166 and 5167 specify the ratio of change for the case in which a skip signal was received during the previ
- Page 721B–63833EN–1/02 11. PROGRAM COMMAND NOTE This signal is used also as a skip signal. (See Section 14.3.) Small–diameter peck drilling in progress signal PECK2
- Page 72211. PROGRAM COMMAND B–63833EN–1/02 5164 Percentage of the spindle speed to be changed when the tool is retracted after an overload torque signal is received [Data type] Byte [Unit of data] % [Valid data range] 0 to 255 This parameter sets the percentage of the spindle speed change caused by the over
- Page 723B–63833EN–1/02 11. PROGRAM COMMAND 5167 Percentage of the cutting feedrate to be changed when the tool is retracted without an overload torque signal received [Data type] Byte [Unit of data] % [Valid data range] 0 to 255 This parameter sets the percentage of the cutting feedrate change during a peck
- Page 72411. PROGRAM COMMAND B–63833EN–1/02 5172 Speed of retraction to point R when no I address is defined [Data type] Word [Unit of data] mm/min [Valid data range] 0 to 4000 This parameter sets the speed of retraction to point R when no I address is defined. 5173 Speed advancing to the bottom of a hole wh
- Page 725B–63833EN–1/02 11. PROGRAM COMMAND Warning WARNING Forwarding or retracting is not performed by rapid traverse positioning. Instead, it is performed with the same interpolation as for cutting feed. This means exponential acceleration/deceleration is performed. However, the tool life management funct
- Page 72612. DISPLAY/SET/EDIT B–63833EN–1/02 12 DISPLAY/SET/EDIT 708
- Page 727B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1 DISPLAY/SET 12.1.1 Clock Function General Time is displayed in the hour/minute/second format on each display screen. Some screens allows display of the year, month, and day. The custom macro system variable can be used to read the time. Time information can b
- Page 72812. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.2 Displaying Operation History General This function displays a history of the key stroke and signal operations, performed by the CNC operator, when a failure or CNC alarm occurs. The following history data is recorded: (1) MDI key operation sequences Example
- Page 729B–63833EN–1/02 12. DISPLAY/SET/EDIT The following table lists parameter values for respective signal types. Table 12.1.2(b) Signal types and corresponding parameter values Signal type Parameter value Not selected 0 G0000 to G0255 1 F0000 to F0255 3 Y0000 to Y0127 5 X0000 to X0127 6 Method of selecti
- Page 73012. DISPLAY/SET/EDIT B–63833EN–1/02 Example:To select the automatic operation start signal (G7.2) as operation history target No. 2, set up the related parameters as listed below: No.12802=1 No.12842=7 No.12882=00000100 If parameter No. 12802 is 1, parameter Nos. 12842 and 12882 are initialized to 0
- Page 731B–63833EN–1/02 12. DISPLAY/SET/EDIT 3122 Time interval used to record data in the operation history [Data type] Word [Unit of data] Minutes [Valid data range] 0 to 1439 Time data is recorded in the operation history at set intervals. When 0 is specified in this parameter, 10 minutes is assumed as th
- Page 73212. DISPLAY/SET/EDIT B–63833EN–1/02 To deselect a signal type, reset the related parameter to 0 (the address and bit combined with the parameter that is reset are reset simultaneously with that parameter). When a signal type is specified, the parameter for setting the address to be combined and the
- Page 733B–63833EN–1/02 12. DISPLAY/SET/EDIT Note NOTE 1 While the operation history screen is displayed, history data is not recorded. 2 When the duration of the on/off state of an input signal is 16 msec or shorter, that state is not recorded in the history. In addition, some signals are not recorded. 3 Ap
- Page 73412. DISPLAY/SET/EDIT B–63833EN–1/02 Reference item OPERATOR’S MANUAL III.13 HELP FUNCTION (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.13 HELP FUNCTION (T series) (B–63834EN) OPERATOR’S MANUAL III.13 HELP FUNCTION (M series) (B–63864EN) Series 0i Mate–B OPERATOR’S MANUAL III.13 HELP FUNC
- Page 735B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1.5 Servo Tuning Screen General On the servo tuning screen, parameters for each axis are listed for the basic adjustment of the servo motor. Parameter #7 #6 #5 #4 #3 #2 #1 #0 3111 SVS [Data type] Bit SVS Servo tuning screen 0 : Not displayed 1 : Displayed Refer
- Page 73612. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.7 Waveform Diagnosis Display General Waveform diagnosis is classified into two main types. (1) One–shot type One–shot waveform diagnosis provides graphs of waveforms. In one–shot waveform diagnosis, the start of data collection can be triggered by the rising
- Page 737B–63833EN–1/02 12. DISPLAY/SET/EDIT 3120 Time from the output of an alarm to the termination of sampling [Data type] Word [Unit of data] ms [Valid data range] 1 to 32760 When the waveform diagnosis function is used, this parameter sets the time form the output of a servo alarm until data collection.
- Page 73812. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.8 Self–diagnosis General To determine the cause of an alarm, check the following. First, it has to be determined if the breakdown is in the CNC, the PMC or the machine. The CNC checks the following. 1) Abnormality of detection system 2) Abnormality of positio
- Page 739B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1.9 Display of Hardware and Software Configuration General The required hardware/software configuration for the CNC can be displayed on the screen. The system configuration screen displays the following information: (1) Printed circuit board configuration a. Th
- Page 74012. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.10 Position Display Neglect General Disabling the current position display is accomplished by setting bit 0 (NDPx) of parameter No. 3115. Bit 1 (NDAx) of parameter No. 3115 enables the display of positions in the machine coordinate system. Signal Position Dis
- Page 741B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1.11 Run Hour and Parts Count Display General This function displays the integrated power–on time, the integrated cycle operation time, the integrated cutting time and timer (started by an input signal from PMC) on the screen. The integrated cycle operation tim
- Page 74212. DISPLAY/SET/EDIT B–63833EN–1/02 General–purpose integrating meter start signal TMRON
- Page 743B–63833EN–1/02 12. DISPLAY/SET/EDIT 6711 Number of machined parts This parameter can be entered on the setting screen. [Data type] Two–word [Unit of data] One piece [Valid data range] 0 to 99999999 The number of machined parts is counted (+1) together with the total number of completed parts when th
- Page 74412. DISPLAY/SET/EDIT B–63833EN–1/02 6750 Integrated value of power–on period This parameter can be entered on the setting screen. [Data type] Two–word [Unit of data] One minute [Valid data range] 0 to 99999999 This parameter displays the accumulated time when the machine is powered. 6751 Operation t
- Page 745B–63833EN–1/02 12. DISPLAY/SET/EDIT 6754 Accumulated cutting time This parameter can be entered on the setting screen. [Data type] Two–word [Unit of data] One minute [Valid data range] 0 to 99999999 This parameter displays the accumulated cutting time that is performed in machine feed such as linear
- Page 74612. DISPLAY/SET/EDIT B–63833EN–1/02 6758 Operation time (accumulated automatic operation time) This parameter can be entered on the setting screen. [Data type] Two–word [Unit of data] One minute [Valid data range] 0 to 99999999 This parameter is the automatic operation drive time (neither stop nor h
- Page 747B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1.12 Graphic Display/ Dynamic Graphic Display General Graphic Display It is possible to draw the programmed tool path on the screen, and check the progress of machining. In addition, it is also possible to enlarge/reduce the drawing. The drawing coordinates (pa
- Page 74812. DISPLAY/SET/EDIT B–63833EN–1/02 Dynamic graphic display There are two functions of Dynamic Graphics. (M series) Path graphic This is used to draw the path of the tool center. This is used to draw the workpiece figure machined by Solid graphic the tool movement. The path graphic function is used
- Page 749B–63833EN–1/02 12. DISPLAY/SET/EDIT Signal Check drawing–under–way signal CKGRP
- Page 75012. DISPLAY/SET/EDIT B–63833EN–1/02 NZM 0 : Screen image enlargement by a conventional method is enabled. 1 : The screen image is enlarged by specifying the center of the screen and the magnification. (Screen image enlargement by the conventional method is disabled.) #7 #6 #5 #4 #3 #2 #1 #0 6501 CSR
- Page 751B–63833EN–1/02 12. DISPLAY/SET/EDIT 6510 Drawing coordinate system [Data type] Byte [Valid data range] 0 to 7 This parameter specifies the drawing coordinate system for the graphic function. The following show the relationship between the parameter values and the drawing coordinate systems. Set valu
- Page 75212. DISPLAY/SET/EDIT B–63833EN–1/02 6511 Right margin in solid drawing 6512 Left margin in solid drawing 6513 Upper margin in solid drawing 6514 Lower margin in solid drawing [Data type] Word [Unit of data] Dot These parameters set the drawing margins in pixels on the screen. The unit is a dot. Stan
- Page 753B–63833EN–1/02 12. DISPLAY/SET/EDIT Reference item III.12.1 GRAPHICS FUNCTION OPERATOR’S MANUAL (M series) (B–63844EN) III.12.2 DYNAMIC GRAPHIC DISPLAY Series 0i–B OPERATOR’S MANUAL III.12.1 GRAPHICS FUNCTION (T series) (B–63834EN) III.12.1 GRAPHICS FUNCTION OPERATOR’S MANUAL (M series) (B–63864EN)
- Page 75412. DISPLAY/SET/EDIT B–63833EN–1/02 3151 Axis number for the first load meter 3152 Axis number for the second load meter 3153 Axis number for the third load meter 3154 Axis number for the 4th load meter 3155 Axis number for the 5th load meter 3156 Axis number for the 6th load meter 3157 Axis number
- Page 755B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1.14 Software Operator’s Panel General The software operator’s panel function replaces part of the control switches on the machine operator’s panel. The control switches for the functions listed in the following table can be replaced with soft switches. Also av
- Page 75612. DISPLAY/SET/EDIT B–63833EN–1/02 Signal Group Function Output signal Related input signal 1 Mode selection MD1O
Manual rapid tra- RTO - Page 757B–63833EN–1/02 12. DISPLAY/SET/EDIT Signal address #7 #6 #5 #4 #3 #2 #1 #0 F072 OUT7 OUT6 OUT5 OUT4 OUT3 OUT2 OUT1 OUT0 F073 ZRNO MD4O MD2O MD1O F074 F075 SPO KEYO DRNO MLKO SBKO BDTO F076 ROV2O ROV1O MP2O MP1O F077 RTO HS1DO HS1CO HS1BO HS1AO F078 *FV7O *FV6O *FV5O *FV4O *FV3O *FV2O *FV1O *FV0O F07
- Page 75812. DISPLAY/SET/EDIT B–63833EN–1/02 OP7 Feed hold on software operator’s panel 0 : Not operational 1 : Operational 7210 Jog–movement axis and its direction on software operator’s panel “↑” 7211 Jog–movement axis and its direction on software operator’s panel “↓” 7212 Jog–movement axis and its direct
- Page 759B–63833EN–1/02 12. DISPLAY/SET/EDIT Example Under X, Y, and Z axis configuration, to set arrow keys to feed the axes in the direction specified as follows, set the parameters to the values given below. [8°] to the positive direction of the Z axis, [2±] to the negative direction of the Z axis, [6³] t
- Page 76012. DISPLAY/SET/EDIT B–63833EN–1/02 Parameter No. 7223: Sets the character code (078) corresponding to N of SIGNAL 1. Parameter No. 7224: Sets the character code (065) corresponding to A of SIGNAL 1. Parameter No. 7225: Sets the character code (076) corresponding to L of SIGNAL 1. Parameter No. 7226
- Page 761B–63833EN–1/02 12. DISPLAY/SET/EDIT Character to Code Correspondence Table Com- Character Code Character Code Comment ment A 065 6 054 B 066 7 055 C 067 8 056 D 068 9 057 E 069 032 Space F 070 ! 033 Exclamation mark G 071 ” 034 Quotation marks H 072 # 035 Number I 073 $ 036 Dollar mark J 074 % 037 P
- Page 76212. DISPLAY/SET/EDIT B–63833EN–1/02 Note NOTE 1 Only the modes shown below can be selected by soft switches. When the mode for DNC operation is to be required, then, all control switches for mode selection should be on the machine operator’s panel or a general–purpose soft switch should be used to s
- Page 763B–63833EN–1/02 12. DISPLAY/SET/EDIT NOTE 4 The following table lists the jog feedrate override values which can be selected by soft switches. *JV00 – *JV150 (*JV0 – *JV150) 15 12 8 4 0 Override ± ± ± ± ± values (%) bit 0 1 1 1 1 1 1 1 1 1 1 1 1 1 1 1 1 0 1 1 1 1 1 1 1 1 1 1 1 1 1 0 1 0 1 0.1 2 1 1 1
- Page 76412. DISPLAY/SET/EDIT B–63833EN–1/02 NOTE 5 The following table lists the feedrate override values which can be selected by soft switches. *FV0O – *FV7O (*FV0 – *FV7) Override 7 4 0 values (%) ± ± ± 0 1 1 1 1 1 1 1 1 0 1 1 1 1 1 0 1 0 1 10 2 1 1 1 0 1 0 1 1 20 3 1 1 1 0 0 0 0 1 30 4 1 1 0 1 0 1 1 1 4
- Page 765B–63833EN–1/02 12. DISPLAY/SET/EDIT Reference item OPERATOR’S MANUAL Displaying and Setting the III.11.4.10 (M series) (B–63844EN) Software Operator’s Panel Series 0i–B OPERATOR’S MANUAL Displaying and Setting the III.11.4.13 (T series) (B–63834EN) Software Operator’s Panel OPERATOR’S MANUAL Display
- Page 76612. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.16 Remote Diagnosis General With the remote diagnosis function, a commercial PC can be connected, as a service terminal, to the CNC via an RS–232–C interface or a telephone line and used to monitor the status of the CNC and to change data in it by means of me
- Page 767B–63833EN–1/02 12. DISPLAY/SET/EDIT c. CNC ³ computer (1) Alarm information (2) Machine position (3) Absolute position (4) Skip position (5) Servo delay (6) Acceleration/deceleration delay (7) Diagnosis (8) Parameter (9) Tool life management data (10) Display screen status (11) Modal information (12
- Page 76812. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.17 External Operator Message Logging and Display General Parameter setting enables one external operator message (consisting of up 255 characters) or, simultaneously, up to 4 external operator message (consisting of up to 63 characters) to be displayed. Exter
- Page 769B–63833EN–1/02 12. DISPLAY/SET/EDIT #7 #6 #5 #4 #3 #2 #1 #0 3207 OM4 [Data type] Bit OM4 A message displayed on the external operator message screen can have: 0 : Up to 256 characters, and just a single message can be displayed. 1 : Up to 64 characters, and up to four messages can be displayed. Refe
- Page 77012. DISPLAY/SET/EDIT B–63833EN–1/02 D Clearing the screen with The CNC screen is cleared once the period (minutes) specified with automatic erase screen parameter No. 3123 has elapsed, provided the following conditions are display satisfied: Conditions for clearing the CNC screen D Automatic erase s
- Page 771B–63833EN–1/02 12. DISPLAY/SET/EDIT Signal Automatic erase screen display cancel signal *CRTOF
- Page 77212. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.19 Touch Panel General A touch panel can be used on the LCD display, as follows: (1) The soft keys (F0 to F9, FR, and FL) in the lower section on the 10.4–inch color LCD/MDI panel are changed to those for the touch panel. (2) Touch panel operation substitutes
- Page 773B–63833EN–1/02 12. DISPLAY/SET/EDIT Software key control When a rectangular soft key button on the screen is pressed, the soft key button display is indented. This type of a soft key behaves in the same manner as conventional soft keys. Cursor control When the cursor is displayed, pressing the desir
- Page 77412. DISPLAY/SET/EDIT B–63833EN–1/02 4 Press the [TP CAL] soft key. The following touch panel calibration screen appears. CALIBRATION OF TOUCH PANEL PLEASE PUSH CALIBRATED POINTS (+ OF 9 POINTS). IF CALIBRATION IS ENDED, PLEASE PUSH KEY. IF CALIBRATION IS CANCELED, PLEASE PUSH
KEY. IF O - Page 775B–63833EN–1/02 12. DISPLAY/SET/EDIT 0 : Enabled. 1 : Disabled. As described in “Hardware connection,” the touch panel is connected to the RS–232–C serial port 2 (JD36B) on the CNC motherboard. When the touch panel is used, serial port 2 (JD36B) is set up for touch panel operation, regardless of an I
- Page 77612. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.20 Periodic Maintenance Screen General The periodic maintenance screen shows the current statuses of those items that require periodic replacement (backup battery, LCD backlight, touch panel, etc.). An item whose service life has expired is indicated by the m
- Page 777B–63833EN–1/02 12. DISPLAY/SET/EDIT (1) Maintenance item names The names of maintenance items are set up here. They can be registered using either the corresponding menu or MDI keys. 1) Menu–based setup 1 To display the setting menu, place the cursor on the desired item, and press the [ENTRY] soft k
- Page 77812. DISPLAY/SET/EDIT B–63833EN–1/02 NOTE For the CNC edit function, specific strings of two or more characters are registered as reserved words of custom macro commands. (Example: GO for GOTO, WH for WHILE, and SI for SIN) Therefore, when a program to register item names is created in the above form
- Page 779B–63833EN–1/02 12. DISPLAY/SET/EDIT NOTE 1 The asterisk (*) is used as a control code, so it cannot be used in the item name. Likewise, square brackets “[” and “]” and parentheses “(” and “)” must be excluded from the item name. 2 If a null item is selected on the machine maintenance screen, the war
- Page 78012. DISPLAY/SET/EDIT B–63833EN–1/02 [CNC maintenance screen] PERIODICAL MAINTENANCE O0001 N12345 (NC) ITEM NAME 01 BATTERY FOR CONTROLLER 02 BATTERY FOR PULSECODER 03 FAN MOTOR 04 LCD BACK LIGHT 05 06 07 08 09 10 >_ EDIT *** ***** *** **** 19:27:05 [ ][ STATUS ][ MACHIN ][ NC ][ (OPRT) ] [ SELECT ][
- Page 781B–63833EN–1/02 12. DISPLAY/SET/EDIT (2) Remaining lifetime The remaining lifetime of an item is the time allowed before it must be replaced. It is displayed in a count–down format. When the remaining lifetime becomes less than the percentage specified in parameter No. 8911 of the corresponding servi
- Page 78212. DISPLAY/SET/EDIT B–63833EN–1/02 (1) Service life To specify the service life, key in the corresponding data and press [INPUT]. The same data is set up as both the service life and remaining lifetime. In addition, the count type is indicated as: “––––––” Pressing the [+INPUT] soft key causes newl
- Page 783B–63833EN–1/02 12. DISPLAY/SET/EDIT (3) Count type Pressing the [TYPE] causes the following count types to be displayed as soft keys. Select the desired one and press the [EXEC] soft key to set it up. Software Meaning Display [EFFECT] No counting takes place (the counter is halted). ––– [ALL–AX] Cou
- Page 78412. DISPLAY/SET/EDIT B–63833EN–1/02 f Menu screen (machine maintenance only) Format G10 L61 P01 [n] ; G10 L61 P02 [n] ; G10 L61 P03 [n] ; : a : Service life r : Remaining lifetime n : Item name [Alphanumeric character] q : Count type 0 = No counting. 1 = Nonstop counting. 2 = Counting continues as l
- Page 785B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.1.21 Actual Speed Display General The actual speed is displayed on the current position display screen, program check screen, and program screen (MDI mode). PMC controlled axis movement data can be added to the actual speed display. Reflection of movement along
- Page 78612. DISPLAY/SET/EDIT B–63833EN–1/02 12.1.22 Other Functions Displaying the main When a subprogram is being executed, the program number of the main program number during program can be displayed beside the number of the currently running subprogram execution program on a 14–inch screen. Parameter #7
- Page 787B–63833EN–1/02 12. DISPLAY/SET/EDIT 12.2 EDIT 12.2.1 Part Program Storage Length General One of the following part program size can be selected. CNC model Series 0i Series 0i Part Mate program size Package A Package B 320m (128Kbyte) — f — 640m (256Kbyte) f — f f: Standard, —: Not Available NOTE The
- Page 78812. DISPLAY/SET/EDIT B–63833EN–1/02 12.2.2 No. of Registered Programs General The number of registered programs is 200. Alarm and message Number Message Description 072 TOO MANY PROGRAMS The number of programs to be stored exceeded 200. Delete unnecessary programs and execute program registeration a
- Page 789B–63833EN–1/02 12. DISPLAY/SET/EDIT When KEY = 0 @ KEY1: Enables the input of tool compensation values and the workpiece zero point offset values, and workpiece coordinate systems shift amount. @ KEY2: Enables the input of setting data and macro variables, and tool life management data. @ KEY3: Enab
- Page 79012. DISPLAY/SET/EDIT B–63833EN–1/02 Reference item OPERATOR’S MANUAL SETTING AND DISPLAYING III.11 (M series) (B–63844EN) DATA Series 0i–B OPERATOR’S MANUAL SETTING AND DISPLAYING III.11 (T series) (B–63834EN) DATA OPERATOR’S MANUAL SETTING AND DISPLAYING III.11 (M series) (B–63864EN) DATA Series 0i
- Page 791B–63833EN–1/02 12. DISPLAY/SET/EDIT 3210 Password(PASSWD) [Data type] Two–word Set a password to this parameter. Its value is not displayed. CAUTION This parameter shows 0, when no value is set to this parameter. Once a key is locked, parameter NE9 cannot become 0 and PASSWD cannot be changed unless
- Page 79212. DISPLAY/SET/EDIT B–63833EN–1/02 Reference item OPERATOR’S MANUAL III.9.9 PASSWORD FUNCTION (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.9.9 PASSWORD FUNCTION (T series) (B–63834EN) OPERATOR’S MANUAL III.9.9 PASSWORD FUNCTION (M series) (B–63864EN) Series 0i Mate–B OPERATOR’S MANUAL I
- Page 793B–63833EN–1/02 12. DISPLAY/SET/EDIT Reference item OPERATOR’S MANUAL III.9.8 BACKGROUND EDITING (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.9.8 BACKGROUND EDITING (T series) (B–63834EN) OPERATOR’S MANUAL III.9.8 BACKGROUND EDITING (M series) (B–63864EN) Series 0i Mate–B OPERATOR’S MANUA
- Page 79412. DISPLAY/SET/EDIT B–63833EN–1/02 12.2.7 Conversational Programming with Graphic Function General Programs can be created block after block on the conversational screen while displaying the G code menu. Blocks in a program can be modified, inserted, or deleted using the G code menu and converstion
- Page 795B–63833EN–1/02 13. INPUT/OUTPUT OF DATA 13 INPUT/OUTPUT OF DATA 777
- Page 79613. INPUT/OUTPUT OF DATA B–63833EN–1/02 13.1 READER/PUNCHER INTERFACE General The data shown below can be input/output through reader/puncher interface. 1. Program 2. Offset data 3. Parameter 4. Pitch error compensation data 5. Custom macro common variables. Setting the IO4 parameter (bit 4 of No. 0
- Page 797B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Parameter The parameters described below must be set up to use an I/O unit interface (RS–232–C serial port) for inputting and outputting data (such as programs and parameters) between external input/output units and memory cards. The I/O CHANNEL setting parame
- Page 79813. INPUT/OUTPUT OF DATA B–63833EN–1/02 I/O CHANNEL: Selection of an input/output device or selection of input device in 0020 the foreground This parameter can be entered on the setting screen [Data type] Byte [Valid data range] 0 to 35 I/O CHANNEL: Selection of the input/output device to be used Th
- Page 799B–63833EN–1/02 13. INPUT/OUTPUT OF DATA NOTE 1 An input/output device can also be selected using the setting screen. Usually, the setting screen is used. 2 The specifications (such as the baud rate and the number of stop bits) of the input/output devices to be connected must be set in the correspond
- Page 80013. INPUT/OUTPUT OF DATA B–63833EN–1/02 Input/output channel number (parameter No.0020) ↓ 0020 I/O CHANNEL 0101 Stop bit and other data I/O CHANNEL=0 Number specified for the input/ Specify a channel for an in- 0102 (channel 1) output device put/output device. 0103 Baud rate I/ O CHANNEL =0 : Channe
- Page 801B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Note) The EOB output patterns are as shown below: NCR CRF EOB output format 0 0 “LF” “CR” “CR” 0 1 “CR” “LF” 1 0 “LF” 1 1 “CR” “LF” NCR Output of the end of block (EOB) in ISO code 0 : LF, CR, CR are output. 1 : Only LF is output. ND3 In DNC operation, a progr
- Page 80213. INPUT/OUTPUT OF DATA B–63833EN–1/02 (2) Parameters of Channel 1 (I/O CHANNEL=0) #7 #6 #5 #4 #3 #2 #1 #0 0101 NFD ASI SB2 NFD ASI HAD SB2 [Data type] Bit SB2 The number of stop bits 0: 1 1: 2 HAD An alarm raised for the internal handy file is: 0: Not displayed in detail on the NC screen. (PS alar
- Page 803B–63833EN–1/02 13. INPUT/OUTPUT OF DATA 0103 Baud rate (when the I/O CHANNEL is set to 0) [Data type] Byte Set baud rate of the input/output device used when the I/O CHANNEL is set to 0, with a set value in Table 13.1 (b). Table 13.1 (b) Set value Baud rate (bps) Set value Baud rate (bps) 1 50 7 600
- Page 80413. INPUT/OUTPUT OF DATA B–63833EN–1/02 (4) Parameters of Channel 2 (I/O CHANNEL=2) #7 #6 #5 #4 #3 #2 #1 #0 0121 NFD ASI SB2 [Data type] Bit These parameters are used when I/O CHANNEL is set to 2. The meanings of the bits are the same as for parameter 0101. 0122 Number specified for the input/output
- Page 805B–63833EN–1/02 13. INPUT/OUTPUT OF DATA #7 #6 #5 #4 #3 #2 #1 #0 0135 ASC NOTE When this parameter is set, the power must be turned off before operation is continued. [Data type] Bit ASC Communication code except NC data 0: ISO code 1: ASCII code Alarm and message Number Message Description 001 TH PA
- Page 80613. INPUT/OUTPUT OF DATA B–63833EN–1/02 Number Message Description 5230 FILE PROTECTED In communication with the built–in handy file unit, a file is write– or read– protected. 5231 TOO MANY FILES In communication with the built–in handy file unit, a limit to the number of files has been exceeded. 52
- Page 807B–63833EN–1/02 13. INPUT/OUTPUT OF DATA 13.2 Refer to an item of FANUC DNC2 DESCRIPTIONS ( B–61992E ) for detailed information of DNC2 interface. DNC2 INTERFACE 789
- Page 80813. INPUT/OUTPUT OF DATA B–63833EN–1/02 13.3 EXTERNAL I/O DEVICE CONTROL General It is possible to request from an external source that a program be registered, collated, or output. D Registeration/Collation As triggered by the external read start signal EXRD, the background edit function saves prog
- Page 809B–63833EN–1/02 13. INPUT/OUTPUT OF DATA D There are some other conditions to determine whether a program can be registered or collated. For example, a program cannot be registered or collated, if a program with the same program number is being executed in the foreground processing. External Punch St
- Page 81013. INPUT/OUTPUT OF DATA B–63833EN–1/02 Background editing signal BGEACT
- Page 811B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Read/punch alarm signal RPALM
- Page 81213. INPUT/OUTPUT OF DATA B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 3201 NPE N99 REP RAL RDL [Data type] Bit RDL When a program is registered by input/output device external control 0 : The new program is registered following the programs already registered. 1 : All registered programs are deleted, then
- Page 813B–63833EN–1/02 13. INPUT/OUTPUT OF DATA NE9 Editing of subprograms with program numbers 9000 to 9999 0 : Not inhibited 1 : Inhibited The following edit operations are disabled: (1) Program deletion (Even when deletion of all programs is specified, programs with program numbers 9000 to 9999 are not d
- Page 81413. INPUT/OUTPUT OF DATA B–63833EN–1/02 Reference item OPERATOR’S MANUAL III.8.4 PROGRAM INPUT/OUTPUT (M series) (B–63844EN) Series 0i–B OPERATOR’S MANUAL III.8.4 PROGRAM INPUT/OUTPUT (T series) (B–63834EN) OPERATOR’S MANUAL III.8.4 PROGRAM INPUT/OUTPUT (M series) (B–63864EN) Series 0i Mate–B OPERAT
- Page 815B–63833EN–1/02 13. INPUT/OUTPUT OF DATA 13.4 EXTERNAL PROGRAM INPUT General By using the external program input start signal, a program can be loaded from an input unit into CNC memory. When an input unit such as the FANUC Handy File or FANUC Floppy Cassette is being used, a file can be searched for
- Page 81613. INPUT/OUTPUT OF DATA B–63833EN–1/02 Workpiece no. search signal File no. PN16 PN8 PN4 PN2 PN1 0 0 0 1 1 03 0 0 1 0 0 04 0 0 1 0 1 05 0 0 1 1 0 06 0 0 1 1 1 07 0 1 0 0 0 08 0 1 0 0 1 09 0 1 0 1 0 10 0 1 0 1 1 11 0 1 1 0 0 12 0 1 1 0 1 13 0 1 1 1 0 14 0 1 1 1 1 15 1 0 0 0 0 16 1 0 0 0 1 17 1 0 0 1
- Page 817B–63833EN–1/02 13. INPUT/OUTPUT OF DATA In this case, the general operation flow is as shown below. Press the cycle start button. Issuing the external program input start signal (MINP) starts program input. The automatic operation mode signal (STL) is set to 1, then program input starts. When input
- Page 81813. INPUT/OUTPUT OF DATA B–63833EN–1/02 The timing chart for data reading is shown below. Execution of a machining program M code command for the Mxxx next program input Code signal M00~M31 Strobe signal MF Single–block signal SBK Completion signal FIN Cycle start lamp signal STL External program in
- Page 819B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Parameter #7 #6 #5 #4 #3 #2 #1 #0 3201 MIP [Data type] Bit type MIP Specifies whether to load a program into memory according to the external program input start signal (MINP). 0 : Does not load a program into memory. 1 : Loads a program into memory. Note NOTE
- Page 82013. INPUT/OUTPUT OF DATA B–63833EN–1/02 13.5 DATA INPUT/OUTPUT FUNCTIONS BASED ON THE I/O Link General Power mate CNC programs, parameters, macro variables, and diagnostic (PMC) data are input/output through the FANUC I/O Link. With the FANUC I/O Link, slaves from group 0 to group 15 can be connecte
- Page 821B–63833EN–1/02 13. INPUT/OUTPUT OF DATA D Basic data input/output (1) Program input/output procedure (a) Program input · When the data input/output function based on the I/O Link is used 1) Specify a number between 20 to 35 as the I/O channel on the setting screen to specify a group number. 2) Speci
- Page 82213. INPUT/OUTPUT OF DATA B–63833EN–1/02 5) Key in a program number. 6) Using soft keys [(OPRT)], continuous–menu key , [PUNCH], and [EXEC], output the program corresponding to the keyed–in program number. · When data input/output function B based on the I/O Link is used 1) Using the PMC function ins
- Page 823B–63833EN–1/02 13. INPUT/OUTPUT OF DATA (a) Macro variable input · When the data input/output function based on the I/O Link is used With power mate CNC DI signals EDG00 to EDG15, specify a start number for the macro variables to be read. With EDN00 to EDN15, specify the number of macro variables to
- Page 82413. INPUT/OUTPUT OF DATA B–63833EN–1/02 (a) Diagnostic (PMC) data input · When the data input/output function based on the I/O Link is used With power mate CNC DI signals EDG00 to EDG15, specify a start number for the diagnostic data items to be read. With EDN00 to EDN15, specify the number of diagn
- Page 825B–63833EN–1/02 13. INPUT/OUTPUT OF DATA D Stopping input/output There are two methods of forcibly terminating input/output. (1) Termination by a reset Input/output can be terminated by a reset. In this case, however, slave read/write stop signal ESTPIO is not output. Therefore, the operation of the
- Page 82613. INPUT/OUTPUT OF DATA B–63833EN–1/02 D Power Mate state signals When the data input/output function based on the I/O Link is used, the (input) state signals for a specified power mate CNC must be reported to the Series 0i/0i Mate. These signals must be posted to the Series 0i/0i Mate via the foll
- Page 827B–63833EN–1/02 13. INPUT/OUTPUT OF DATA D DI/DO signal timing The DI/DO signal timing charts applicable when data input/output charts function B based on the I/O Link is used are shown below. When the ordinary data input/output function based on the I/O Link is used, 1) through 4) in the figures are
- Page 82813. INPUT/OUTPUT OF DATA B–63833EN–1/02 (6) (9) (10) (12) (3) (15) (1) I/O Link specification signal IOLS (4) (15) (2) External read/punch signal EXRD/EXWT (5) (3) I/O Link confirmation signal IOLACK (13) (4) Power Mate read/write in– progress signal BGION (5) Power Mate read/write alarm signal BGIA
- Page 829B–63833EN–1/02 13. INPUT/OUTPUT OF DATA (2) When an alarm is issued by the Series 0i/0i Mate (including the case where processing is stopped by external read/punch signal EXSTP) Steps 1) to 10) are the same as those for ordinary input/output. 11) When the Series 0i/0i Mate issues an alarm, or when e
- Page 83013. INPUT/OUTPUT OF DATA B–63833EN–1/02 (6) (9) (10) (12) (3) (15) (1) I/O Link specification signal IOLS (4) (2) External read/punch signal EXRD/EXWT (7) (15) (3) I/O Link confirmation signal IOLACK (13) (4) Power Mate read/write in– progress signal BGION (13) (5) Power Mate read/write alarm signal
- Page 831B–63833EN–1/02 13. INPUT/OUTPUT OF DATA (3) When an alarm is issued by the power mate CNC Steps 1) to 10) are the same as those for ordinary input/output. 11) When the power mate CNC issues an alarm, Power Mate read/write alarm signal BGIALM is set to 1, and Power Mate read/write in–progress signal
- Page 83213. INPUT/OUTPUT OF DATA B–63833EN–1/02 (6) (9) (10) (3) (13) (1) I/O Link specification signal IOLS (4) (2) External read/punch signal EXRD/EXWT (7) (13) (3) I/O Link confirmation signal IOLACK (11) (4) Power Mate read/write in– progress signal BGION (11) (5) Power Mate read/write alarm signal BGIA
- Page 833B–63833EN–1/02 13. INPUT/OUTPUT OF DATA D Troubleshooting The data input/output function based on the FANUC I/O Link is implemented by various elements such as ladder programs, I/O Link assignment, Series 0i/0i Mate parameters, and power mate CNC parameters. So, problems may occur when the function
- Page 83413. INPUT/OUTPUT OF DATA B–63833EN–1/02 Symptom Cause and corrective action When an attempt is made to output I/O Link confirmation signal IOLACK data to a power mate CNC: is not set to 1. Series 0i/0i Mate: A ladder program error, I/O Link as- OUTPUT blinks con- signment error may prevent. tinuousl
- Page 835B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Symptom Cause and corrective action When an attempt is made to output Bit 1 (ISO) of parameter No. 0000 is macro variables to a power mate set to 1 (EIA code). CNC: The EIA code does not include #, Series 0i/0i Mate: such that an ISO code must be set. Alarm 86
- Page 83613. INPUT/OUTPUT OF DATA B–63833EN–1/02 Power Mate read/write alarm signal BGIALM
- Page 837B–63833EN–1/02 13. INPUT/OUTPUT OF DATA I/O Link specification signal IOLS
- Page 83813. INPUT/OUTPUT OF DATA B–63833EN–1/02 This signal is set to 0 in the following case: – When data input/output is terminated This signal is a power mate CNC control signal. The corresponding Power Mate side signal is IOLNK
- Page 839B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Slave external write start signal EWTIO
- Page 84013. INPUT/OUTPUT OF DATA B–63833EN–1/02 This signal is set to 0 in the following case: – When data input/output is terminated This signal is a Power Mate control signal. The corresponding power mate CNC side signal is EVAR
- Page 841B–63833EN–1/02 13. INPUT/OUTPUT OF DATA Group number output signals SRLNO0 to SRLNO3
- Page 84213. INPUT/OUTPUT OF DATA B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 G058 EXWT EXSTP EXRD #7 #6 #5 #4 #3 #2 #1 #0 G091 SRLNI3 SRLNI2 SRLNI1 SRLNI0 #7 #6 #5 #4 #3 #2 #1 #0 G092 BGEN BGIALM BGION IOLS IOLACK #7 #6 #5 #4 #3 #2 #1 #0 F053 BGEACT RPALM RPBSY #7 #6 #5 #4 #3 #2 #1 #0 F177 EDGN EP
- Page 843B–63833EN–1/02 13. INPUT/OUTPUT OF DATA 8760 Program number for data registration (data input/output function using the I/O link) [Data type] Word [Valid data range] 0 to 9999 When the data input/output function using the I/O link is used, this parameter sets the program numbers of the programs to b
- Page 84413. INPUT/OUTPUT OF DATA B–63833EN–1/02 Alarm and message Number Message Description 085 COMMUNICATION When entering data in the memory by using ERROR Reader / Puncher interface, or FANUC I/O Link an overrun, parity or framing error was gener- ated. The number of bits of input data or setting of bau
- Page 845B–63833EN–1/02 14. MEASUREMENT 14 MEASUREMENT 827
- Page 84614. MEASUREMENT B–63833EN–1/02 14.1 TOOL LENGTH MEASUREMENT (M SERIES) General The value displayed as a relative position can be set in the offset memory as an offset value by a soft key. Switch to the offset value display screen on the CRT. Relative positions are also displayed on this screen. Then
- Page 847B–63833EN–1/02 14. MEASUREMENT 14.2 AUTOMATIC TOOL LENGTH MEASUREMENT (M SERIES)/ AUTOMATIC TOOL OFFSET (T SERIES) General When a tool is moved to the measurement position by execution of a command given to the CNC, the CNC automatically measures the difference between the current coordinate value a
- Page 84814. MEASUREMENT B–63833EN–1/02 The tool decelerates and temporarily stops at the distance γ before the measuring position. The tool then moves to the measuring position at the speed preset by a parameter No. 6241. If the measuring position reached signal corresponding to the G code is turned “1” aft
- Page 849B–63833EN–1/02 14. MEASUREMENT NOTE 1 The measuring position reached signal requires at least 10 msec. 2 The CNC directly inputs the measuring position reached signals from the machine tool; the PMC does not process them. 3 If automatic tool offset or automatic tool length measurement is not used, t
- Page 85014. MEASUREMENT B–63833EN–1/02 CAUTION Set a radius value irrespective of whether the diameter programming or the radius programming is specified. 6254 e value on X axis during automatic tool offset e value during tool length automatic measurement 6255 e value on Z axis during tool automatic offset
- Page 851B–63833EN–1/02 14. MEASUREMENT Alarm and message Number Message Description 080 G37 ARRIVAL SIGNAL In the automatic tool length measure- NOT ASSERTED ment function (G37), the measurement position reached signal (XAE, YAE, or ZAE) is not turned on within an area specified in parameter 6254 (value ε).
- Page 85214. MEASUREMENT B–63833EN–1/02 Note NOTE 1 Measurement speed, γ, and ε are set as parameters.ε must be positive numbers and satisfy the condition of γ>ε. 2 The compensation value is updated by the following formula: New compensation value =(Current compensation value)+[(Current position of the tool
- Page 853B–63833EN–1/02 14. MEASUREMENT Reference item OPERATOR’S MANUAL AUTOMATIC TOOL LENGTH II.14.2 (M series) (B–63844EN) MEASUREMENT (G37) Series 0i–B OPERATOR’S MANUAL AUTOMATIC TOOL OFFSET II.14.5 (T series) (B–63834EN) (G36, G37) OPERATOR’S MANUAL AUTOMATIC TOOL LENGTH Series 0i Mate–B II.14.2 (M ser
- Page 85414. MEASUREMENT B–63833EN–1/02 14.3 SKIP FUNCTION 14.3.1 Skip Function General Linear interpolation can be commanded by specifying axial move following the G31 command, like G01. If an external skip signal is input during the execution of this command, execution of the command is interrupted and the
- Page 855B–63833EN–1/02 14. MEASUREMENT NOTE 1 The skip signal width requires at least 10 msec. 2 The CNC directly reads the skip signal SKIP
- Page 85614. MEASUREMENT B–63833EN–1/02 Warning WARNING Disable feedrate override, dry run, and automatic acceleration/deceleration (enabled with parameter No. 6200#7 SKF=1) when the feedrate per minute is specified, allowing for reducing an error in the position of the tool when a skip signal is input. Thes
- Page 857B–63833EN–1/02 14. MEASUREMENT 14.3.2 High–speed Skip Signal General The skip function operates based on a high-speed skip signal (HDI0: connected directly to the CNC; not via the PMC) instead of an ordinary skip signal (X004#7). In this case, one signal can be input. (Either can be enabled/disabled
- Page 85814. MEASUREMENT B–63833EN–1/02 P : Distance to be measured [mm/inch] Q : Servo delay [mm/inch] Under the conditions shown above, the NC calculates the following equation using parameter SEA (bit 0 of parameter No. 6201) or SEB (bit 1 of parameter No. 6201): P = Pnc – Q For type A (SEA bit 0 of param
- Page 859B–63833EN–1/02 14. MEASUREMENT Signal High Speed Skip Staus Signal HDO0
- Page 86014. MEASUREMENT B–63833EN–1/02 IGX When the high-speed skip function is used, SKIP (bit 7 of X004), SKIPP (bit 6 of G006), and +MIT1 to –MIT2 (bits 2 to 5 of X004) are: 0 : Enabled as skip signals. 1 : Disabled as skip signals. NOTE SKIPP (bit 6 of G006) and +MIT1 to –MIT2 (bits 2 to 5 of X004) are
- Page 861B–63833EN–1/02 14. MEASUREMENT Signal Skip signal SKIP, SKIP2 to SKIP8
[Classification] Input signal [Function] These signals terminate skip cutting. That is, the position where a skip signal turns to “1” in a command program block containing G31P1 (or G31), G31P2, or G31P3, G31P4 is stored i - Page 86214. MEASUREMENT B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 X004 ESKIP –MIT2 +MIT2 –MIT1 +MIT1 ZAE XAE SKIP (T series) SKIP6 SKIP5 SKIP4 SKIP3 SKIP2 SKIP8 SKIP7 ESKIP ZAE YAE XAE SKIP SKIP5 SKIP4 SKIP3 (M series) SKIP6 SKIP2 SKIP8 SKIP7 WARNING 1 SKIP2 to SKIP6 are at the same addresses as
- Page 863B–63833EN–1/02 14. MEASUREMENT #7 #6 #5 #4 #3 #2 #1 #0 6202 1S8 1S7 1S6 1S5 1S4 1S3 1S2 1S1 6203 2S8 2S7 2S6 2S5 2S4 2S3 2S2 2S1 6204 3S8 3S7 3S6 3S5 3S4 3S3 3S2 3S1 6205 4S8 4S7 4S6 4S5 4S4 4S3 4S2 4S1 6206 DS8 DS7 DS6 DS5 DS4 DS3 DS2 DS1 [Data type] Bit type 1S1–1S8, 2S1–2S8, 3S1–3S8, 4S1–4S8, DS1
- Page 86414. MEASUREMENT B–63833EN–1/02 Note NOTE The skip cutting commands G31 P1, G31 P2, G31 P3, and G31 P4 are all identical, except that they correspond to different skip signals. The tool moves along the specified axis performing linear interpolation until the SKIP signal is set to “1” or the end point
- Page 865B–63833EN–1/02 14. MEASUREMENT 14.3.4 Torque Limit Skip General Specifying a move command after G31 P99 (or G31 P98) with a motor torque limit set (for example, specifying a torque limit on the PMC window) allows the same cutting feed as that specified with G01 to be performed. While the tool is mov
- Page 86614. MEASUREMENT B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 F114 TRQL4 TRQL3 TRQL2 TRQL1 Parameter #7 #6 #5 #4 #3 #2 #1 #0 6201 TSA TSE [Data type] Bit type TSE When a skip operation is performed by the G31 P99 or P98 command used to specify torque limit skip: 0 : Corrects servo errors. (1
- Page 867B–63833EN–1/02 14. MEASUREMENT Alarm and message Number Message Description 015 TOO MANY AXES COM- In the block including the command for MANDED the skip function (G31 P99/P98), to be executed under the control of the torque limit reach signal, no axis move command is specified, or two or more axes
- Page 86814. MEASUREMENT B–63833EN–1/02 14.4 ENTERING COMPENSATION VALUES 14.4.1 Input of Offset Value Measured A (T series) General This is a function of setting an offset value by key-inputting a workpiece diameter manually cut and measured from the MDI keyboard. First the workpiece is cut in the longitudi
- Page 869B–63833EN–1/02 14. MEASUREMENT NOTE To use this signal, set parameter PRC (No.5005#2) to 1. Signal address #7 #6 #5 #4 #3 #2 #1 #0 G040 PRC Parameter #7 #6 #5 #4 #3 #2 #1 #0 5005 PRC [Data type] Bit type PRC Direct input of tool offset value and workpiece coordinate-system shift value 0 : Not use a
- Page 87014. MEASUREMENT B–63833EN–1/02 14.4.2 Input of Tool Offset Value Measured B (T series) General When the touch sensor is provided, the tool offset value can be automatically settable in the tool offset memory, by moving the tool to make contact with the touch sensor during manual operation. The workp
- Page 871B–63833EN–1/02 14. MEASUREMENT D Setting tool offset value Determine a specific point on the machine tool as the measuring reference position. In advance, set the distance from this point to the measuring position (contact face of the touch sensor) as a reference value, using parameter No. 5015 to 5
- Page 87214. MEASUREMENT B–63833EN–1/02 NOTE 1 Pulse storage for automatic decision is carried out in the manual mode while the GOSQM
- Page 873B–63833EN–1/02 14. MEASUREMENT Select, manually or automatically, the tool compensation number to be set up, using the QNI parameter (bit 5 of No. 5005). S QNI = 0 (manual selection) Set the cursor to the desired tool compensation number by operating the MDI (such as page and cursor keys). S QNI = 1
- Page 87414. MEASUREMENT B–63833EN–1/02 Example 1 The difference between the reference tool nose tip position and the measuring tool nose tip position can be set as the tool offset value. Define the reference tool nose tip position at the mechanical reference position (machine zero position) as the measuring
- Page 875B–63833EN–1/02 14. MEASUREMENT Example 2 The measuring reference point may be an imaginary point (imaginary zero point), as shown in the figure below. The difference between the imaginary zero point and the measuring tool nose tip position at the mechanical reference point can be set as the tool off
- Page 87614. MEASUREMENT B–63833EN–1/02 If the tool setter function For the tool set function for a one–turret/two–spindle lathe, the workpiece for a one–turret/ coordinate shift amount for the Z–axis is automatically set in any of two–spindle lathe is workpiece coordinate systems G54 to G59 for workpiece co
- Page 877B–63833EN–1/02 14. MEASUREMENT Machine +X zero point Zt +Z OFSZ –EXOFSZ (0,0) Measuring tool nose position at the mechani- OFSX cal machine position Workpiece coordinate system zero point (programmed zero point) EXOFSz : Workpiece coordinate system shift amount to be set OFSz : Tool geometry offset
- Page 87814. MEASUREMENT B–63833EN–1/02 Basic Procedure to Set To use the tool setter function for a one–turret/two–spindle lathe, first Tool Offset Value specify the spindle to be measured, using the S2TLS (G040.5) (spindle measurement select) signal. (1) Execute manual reference position return. By executi
- Page 879B–63833EN–1/02 14. MEASUREMENT (9) Set the tool compensation value writing mode signal GOQSM to “0”. The writing mode is canceled and the blinking “OFST” indicator light goes off. When the tool setter function for a one–turret/two–spindle lathe is in use, the S1MES or S2MES (spindle under measuremen
- Page 88014. MEASUREMENT B–63833EN–1/02 The writing mode is canceled and the blinking “WSFT” indicator light goes off. When the tool setter function for a one–turret/two–spindle lathe is in use, the S1MES or S2MES (spindle under measurement) signal, whichever is applicable, becomes 0. Signal Tool offset writ
- Page 881B–63833EN–1/02 14. MEASUREMENT If the TS1 parameter (bit 3 of 5004) is 1 +MIT1 : Automatic decision causes the related two directions of each axis to be subjected to interlock. –MIT1 : Not used +MIT2 : Not used –MIT2 : Not used D When signal GOQSM for selecting the mode for writing tool compensation
- Page 88214. MEASUREMENT B–63833EN–1/02 D When signal GOQSM for selecting the mode for writing tool compensation is turned “1”, the manual feed interlock signal also automatically calculates the tool geometry compensation for the tool compensation number pointed to by the cursor and sets the result in tool c
- Page 883B–63833EN–1/02 14. MEASUREMENT Spindle measurement select signal S2TLS
- Page 88414. MEASUREMENT B–63833EN–1/02 Signal address #7 #6 #5 #4 #3 #2 #1 #0 X004 –MIT2 +MIT2 –MIT1 +MIT1 SKIP5 SKIP4 SKIP3 SKIP2 WARNING Since the same addresses are used for both +MIT1, –MIT1, +MIT2, –MIT2 and skip signals SKIP2 to SKIP5 (multi–step skip), be careful when using these two signal types. #7
- Page 885B–63833EN–1/02 14. MEASUREMENT #7 #6 #5 #4 #3 #2 #1 #0 5009 GSC [Data type] Bit GSC Specifies from which the offset write input signal is to be input for the tool compensation amount measurement value direct input B function, as follows: 0 : To be input from the machine. 1 : To be input from the PMC
- Page 88614. MEASUREMENT B–63833EN–1/02 They set the distance (with sign) between the measurement reference position and sensor contact surface. For an axis under diameter program- ming, set it using a diameter value. NOTE Parameter Nos. 5056 to 5069 are valid if the 2NR parameter (bit 0 of parameter No. 505
- Page 887B–63833EN–1/02 14. MEASUREMENT 5020 Tool offset number used for the input of tool offset value measured B [Data type] Byte [Valid data range] 0 to the number of tools to be compensated. Set tool offset number used for the input of tool offset value measured B function (i.e. when workpiece coordinate
- Page 88814. MEASUREMENT B–63833EN–1/02 Example: Tool offset value When setting = 8 When setting = 10 Spindle 1 1 to 8 1 to 10 Spindle 2 9 to 64 11 ro 64 If 0 is set for this parameter, or if 64 is exceeded, the following is assumed: Spindle 1 1 to 32 Spindle 2 33 to 64 5054 Workpiece coordinate system memor
- Page 889B–63833EN–1/02 14. MEASUREMENT 14.4.3 Input of Measured Workpiece Origin Offsets General By directly entering the measured deviation of the actual coordinate system from a programmed work coordinate system, the workpiece zero point offset at the cursor is automatically set so that a commanded value
- Page 89015. PMC CONTROL FUNCTION B–63833EN–1/02 15 PMC CONTROL FUNCTION 872
- Page 891B–63833EN–1/02 15. PMC CONTROL FUNCTION 15.1 PMC AXIS CONTROL 15.1.1 PMC Axis Control General The PMC can directly control any given axis, independent of the CNC. In other words, moving the tool along axes that are not controlled by the CNC is possible by entering commands, such as those specifying
- Page 89215. PMC CONTROL FUNCTION B–63833EN–1/02 PMC CNC DI/ DO Commands from path 1 Group A α axis control Commands from path 2 Group B β axis control Commands from path 3 Group C γ axis control Commands from path 4 Group D ε axis control In the following description, input/output signals from the four path
- Page 893B–63833EN–1/02 15. PMC CONTROL FUNCTION These signals, together with block stop prohibition signal EMSBKg (described later), determine one complete operation, which is tantamount to one block executed during CNC–controlled automatic operation. These signals may be collectively called the axis contro
- Page 89415. PMC CONTROL FUNCTION B–63833EN–1/02 When the execution of command [1] is completed: ⋅ command [2] is transferred from the waiting buffer to the executing buffer; ⋅ command [3] is transferred from the input buffer to the waiting buffer; and ⋅ command [4] is transferred to the input buffer as the
- Page 895B–63833EN–1/02 15. PMC CONTROL FUNCTION (5) Repeat steps (3) and (4) until all the blocks have been issued. When the final block has been issued, set control axis selection signals EAX1 to EAX4 to “0”. Before setting these signals to “0”, however, check that the blocks stored in the CNC’s input, wai
- Page 89615. PMC CONTROL FUNCTION B–63833EN–1/02 No. Symbol Signal name 17 EMBUFg Buffering disable signal 18 *EAXSL Control axis selection status signal 19 EINPg In–position signal 20 ECKZg Following zero checking signal 21 EIALg Alarm signal 22 EGENg Axis moving signal 23 EDENg Auxiliary function executing
- Page 897B–63833EN–1/02 15. PMC CONTROL FUNCTION Signal Detail 1 Control axis selection signals EAX1 to EAX4 [Classification] Input signal [Function] When the signal is set to “1”, the corresponding axis becomes subject to PMC control. When the signal is set to “0”, PMC control becomes invalid. Changing the
- Page 89815. PMC CONTROL FUNCTION B–63833EN–1/02 Axis control command Operation (hexadecimal code) Cutting feed – feed per revolution (exponential acceleration/ deceleration or linear acceleration/deceleration after inter- polation) 02h Performs the same operation as G95 G01, used by the CNC. Skip – feed per
- Page 899B–63833EN–1/02 15. PMC CONTROL FUNCTION Axis control command Operation (hexadecimal code) External pulse synchronization – 2nd manual handle 0Eh Synchronizes with the second manual handle. External pulse synchronization – 3rd manual handle 0Fh Synchronizes with the 3rd manual handle. Speed command (
- Page 90015. PMC CONTROL FUNCTION B–63833EN–1/02 The direction of the grid relative to the proximate position depends on ZMIx, bit 5 of parameter No. 1006. After the reference position has been established, reference position return can be performed at high speed by issuing the reference position return comm
- Page 901B–63833EN–1/02 15. PMC CONTROL FUNCTION Machine coordinate The machine coordinate system selection command (EC0g to EC6g: system selection 20h) performs absolute positioning to move the tool in rapid traverse to a specified position on the machine coordinate system. This command is used to move the
- Page 90215. PMC CONTROL FUNCTION B–63833EN–1/02 (2) Switching from torque control to position control (canceling torque control mode) Torque control mode is canceled when any of the following conditions is satisfied: 1) The reset signal ECLRg is brought to “1”. 2) A servo alarm is issued. 3) An OT alarm is
- Page 903B–63833EN–1/02 15. PMC CONTROL FUNCTION The following table shows the correspondence between the axis control commands and their data: Command block Axis control code Operation Command data signal EC0g to EC6g Rapid traverse 00h Total moving distance EID0g to EID31g Rapid traverse rate EIF0g to EIF1
- Page 90415. PMC CONTROL FUNCTION B–63833EN–1/02 Axis control code Operation Command data signal EC0g to EC6g Torque control 11h Maximum feedrate, EIF0g to EIF15g Torque data, EID0g to EID31g Auxiliary function 12h Auxiliary function code EID0g to EID15g Miscellaneous function 14h Miscellaneous function 2 co
- Page 905B–63833EN–1/02 15. PMC CONTROL FUNCTION [Valid data range] Specify data within the range given in the following table. Data range Unit IS-B IS-C Linear Metric machine 30 to 15000 30 to 12000 mm/min axis Inch machine 30 to 6000 30 to 4800 inch/min Rotation axis 30 to 15000 30 to 12000 deg/min (7) Cut
- Page 90615. PMC CONTROL FUNCTION B–63833EN–1/02 (9) Cutting feed – feed per rotation (EC0g to EC6g: 02h) For this command, the signals are used to specify the amount by which the tool is moved for every rotation of the spindle.
[Unit of data] The data increment depends on the settings of bits - Page 907B–63833EN–1/02 15. PMC CONTROL FUNCTION CAUTION The specified feedrate can be magnified by 1, 10, or 100 by setting bits 6 (FR1) and 7 (FR2) of parameter No. 8002 accordingly. (10) External pulse synchronization – main spindle (EC0g to EC6g: 0Bh) (11) External pulse synchronization – first manual ha
- Page 90815. PMC CONTROL FUNCTION B–63833EN–1/02 D Maximum feedrate (with override of 254%) IS–B IS–C Metric input Inch input Metric input Inch input Magnified 166458mm/ 1664.58inch/ 16645mm/min 166.45inch/ by 1 min min min Magnified 1664589mm/ 16645.89 166458mm/ 1664.58inch/ by 10 min inch/min min min Magni
- Page 909B–63833EN–1/02 15. PMC CONTROL FUNCTION Gears Speed command Amplifier Motor ↑ (b) Axis Detector ↑ (a) (a) The speed command for PMC axis control requires the specification of the servo motor speed, not the feedrate along an axis. To specify a feedrate along the axis when gears are used to link the s
- Page 91015. PMC CONTROL FUNCTION B–63833EN–1/02 The maximum feedrate in torque control mode can be changed in torque control mode by setting the new feedrate data in the signal then inverting the logic of axis control command read signal EBUFg. Valid data range Units 1 to 32767 min–1 NOTE The data units wil
- Page 911B–63833EN–1/02 15. PMC CONTROL FUNCTION (5) Dwell (EC0g to EC6g: 04h) For this command, the signals are used to specify, in binary format, the dwell time. Data range Unit 1 to 9999999 ms When diameter programming is specified with bit 3 (DIAx) of parameter No. 1006, bit 1 (CDI) of parameter No. 8005
- Page 91215. PMC CONTROL FUNCTION B–63833EN–1/02 (9) When a torque control command (EC0g to EC6g: 11h) is specified Specify the torque data. Specify a positive value when the torque is to be applied in the positive direction. Specify a negative value when the torque is to be applied in the negative direction
- Page 913B–63833EN–1/02 15. PMC CONTROL FUNCTION The continuous feed command (EC0g to EC6g: 06h) and external pulse synchronization command (EC0g to EC6g: 0Bh, 0Dh to 0Fh) can be terminated by setting reset signal ECLRg to “1”. When these commands are terminated, the servo motor decelerates and stops, the ax
- Page 91415. PMC CONTROL FUNCTION B–63833EN–1/02 The timing chart for the command operation is shown below. |← More than →| ESBKg 8 msec (input) [1] [2] [3] Command block (input) EBUFg (input) EBSYg (output) The buffer is full. Input buffer [2] [3] Waiting buffer [1] [2] Executing buffer [1] Beginning of exe
- Page 915B–63833EN–1/02 15. PMC CONTROL FUNCTION 15 Auxiliary function completion signal EFINg [Classification] Input signal [Function] When an auxiliary function command (EC0g to EC6g: 12h) is issued by the PMC, the auxiliary function code is specified in a byte (using signals EID0g to EID7g) or two bytes (
- Page 91615. PMC CONTROL FUNCTION B–63833EN–1/02 The timing chart for the command operation is shown below. EMBUFg (input) [1] [2] Command block (input) EBUFg (input) Command disabled EBSYg (output) Input buffer Waiting buffer Executing [1] [2] buffer Beginning of End Beginning of execution execution Bufferi
- Page 917B–63833EN–1/02 15. PMC CONTROL FUNCTION 18 Control axis selection status signal *EAXSL [Classification] Output signal [Function] When this signal is set to “0”, control axis selection signals EAX1 to EAX4 can be changed. This signal is set to “1” in the following cases: (1) When the tool is moving a
- Page 91815. PMC CONTROL FUNCTION B–63833EN–1/02 20 Following zero checking signal ECKZg [Classification] Output signal [Function] This signal is set to “1” when following zero check or in–position check is being performed for the corresponding PMC–controlled axis. 21 Alarm signal EIALg [Classification] Outp
- Page 919B–63833EN–1/02 15. PMC CONTROL FUNCTION NOTE This signal is set to “0” when distribution for the axis is completed (the signal is set to “0” during deceleration). 23 Auxiliary function executing signal EDENg [Classification] Output signal [Function] When an auxiliary function (EC0g to EC6g: 12h) is
- Page 92015. PMC CONTROL FUNCTION B–63833EN–1/02 These signals are set to “0” when the overtravel alarm is released and reset signal ECLRg is set to “1”. See “Alarm signal EIALg” for details of how to release an overtravel alarm. 26 Feedrate override signals *FV0E to *FV7E [Classification] Input signal [Func
- Page 921B–63833EN–1/02 15. PMC CONTROL FUNCTION 28 Rapid traverse override signals ROV1E and ROV2E [Classification] Input signal [Function] These signals can be used to select the override for the rapid traverse rate, independently of the CNC, by setting bit 2 (OVE) of parameter No. 8001. Rapid traverse ove
- Page 92215. PMC CONTROL FUNCTION B–63833EN–1/02 31 Override 0% signal EOV0 [Classification] Output signal [Function] This signal is set to “1” when the feedrate override is 0%. 32 Skip signal ESKIP [Classification] Input signal [Function] When this signal is set to “1” during execution of the skip cutting c
- Page 923B–63833EN–1/02 15. PMC CONTROL FUNCTION 36 External deceleration signals *+ED1 to *+ED4, *–ED1 to *–ED4 [Classification] Input signal [Function] These signals are also used by the CNC. The signals are provided for each direction of the individual controlled axes. The plus or minus sign in the signal
- Page 92415. PMC CONTROL FUNCTION B–63833EN–1/02 37 Accumulated zero check signal ELCKZg [Classification] Input signal [Function] Setting this signal to 1 causes an accumulated zero check between blocks to be made at a subsequent cutting feed command. (1) Cutting feed per minute (EC0g to EC6g: 01h) (2) Cutti
- Page 925B–63833EN–1/02 15. PMC CONTROL FUNCTION #7 #6 #5 #4 #3 #2 #1 #0 G142 EBUFA ECLRA ESTPA ESOFA ESBKA EMBUFA ELCKZA EFINA G143 EMSBKA EC6A EC5A EC4A EC3A EC2A EC1A EC0A G144 EIF7A EIF6A EIF5A EIF4A EIF3A EIF2A EIF1A EIF0A G145 EIF15A EIF14A EIF13A EIF12A EIF11A EIF10A EIF9A EIF8A For group A G146 EID7A
- Page 92615. PMC CONTROL FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G166 EBUFC ECLRC ESTPC ESOFC ESBKC EMBUFC ELCKZC EFINC G167 EMSBKC EC6C EC5C EC4C EC3C EC2C EC1C EC0C G168 EIF7C EIF6C EIF5C EIF4C EIF3C EIF2C EIF1C EIF0C G169 EIF15C EIF14C EIF13C EIF12C EIF11C EIF10C EIF9C EIF8C For group C G170 EID7C
- Page 927B–63833EN–1/02 15. PMC CONTROL FUNCTION CNC→PMC ADDRESS #7 #6 #5 #4 #3 #2 #1 #0 F112 EADEN4 EADEN3 EADEN2 EADEN1 F129 *EAXSL EOV0 #7 #6 #5 #4 #3 #2 #1 #0 F130 EBSYA EOTNA EOTPA EGENA EDENA EIALA ECKZA EINPA For F131 EMF3A EMF2A EABUFA EMFA group A F132 EM28A EM24A EM22A EM21A EM18A EM14A EM12A EM11A
- Page 92815. PMC CONTROL FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F182 EACNT4 EACNT3 EACNT2 EACNT1 F190 TRQM4 TRQM3 TRQM2 TRQM1 Parameter 1427 External deceleration speed of each axis [Data type] Word axis [Unit of data] Valid data range Increment system Unit of data [Valid data range] IS–B IS–C Milli
- Page 929B–63833EN–1/02 15. PMC CONTROL FUNCTION NOTE This parameter is valid when TQF (bit 4 of parameter 1803) is held 0. #7 #6 #5 #4 #3 #2 #1 #0 2000 DGPRx [Data type] Bit axis DGPRx At power–ON, the torque constant (parameter No. 2105): 0 : Is automatically set to the standard value specific to the motor
- Page 93015. PMC CONTROL FUNCTION B–63833EN–1/02 NOTE This parameter is valid when the same axis is controlled alternately by the CNC and PMC. #7 #6 #5 #4 #3 #2 #1 #0 8001 SKE AUX NCC RDE OVE MLE [Data type] Bit MLE Machine lock signal MLK is valid for PMC–controlled axes 0 : Is valid 1 : Is invalid NOTE Eac
- Page 931B–63833EN–1/02 15. PMC CONTROL FUNCTION #7 #6 #5 #4 #3 #2 #1 #0 8002 FR2 FR1 PF2 PF1 F10 SUE DWE RPD [Data type] Bit RPD Rapid traverse rate for PMC–controlled axes 0 : Feedrate specified with parameter No. 1420 1 : Feedrate specified with the feedrate data in an axis control command DWE Minimum tim
- Page 93215. PMC CONTROL FUNCTION B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 8003 PIM NOTE When this parameter is set, the power must be turned off then back on again to make the setting effective. [Data type] Bit type PIM If a linear axis is controlled solely by the PMC, the commands for that axis are: 0 : Affe
- Page 933B–63833EN–1/02 15. PMC CONTROL FUNCTION NOTE The above setting is effective only when the NAHx bit (bit 7 of parameter No. 1819) is set to 0. G8R If a rapid traverse command is specified for a PMC–controlled axis, look–ahead control is: 0 : Disabled. 1 : Enabled. NOTE The above setting is effective
- Page 93415. PMC CONTROL FUNCTION B–63833EN–1/02 NOTE 1 This parameter is valid when the DIAx bit (bit 3 of parameter 1006) is held to 1. 2 When the CDI bit is set to 1, the NDI bit (bit 7 of parameter 8004) is invalid. MFD : The miscellaneous function individual output of the PMC axis control function is: 0
- Page 935B–63833EN–1/02 15. PMC CONTROL FUNCTION 8028 Linear acceleration/deceleration time constant for jog feed specified by the speed command for each PMC–controlled axis [Data type] Word axis [Unit of data] msec/1000 min–1 [Valid data range] 0 to 32767 Specify, for each PMC–controlled axis, the time need
- Page 93615. PMC CONTROL FUNCTION B–63833EN–1/02 (1) P/S Alarm Number Message Description 130 ILLEGAL AXIS An axis control command was given by OPERATION PMC to an axis controlled by CNC. Or an axis control command was given by CNC to an axis controlled by PMC. Modify the program. 139 CAN NOT CHANGE PMC A cu
- Page 937B–63833EN–1/02 15. PMC CONTROL FUNCTION Caution CAUTION 1 Emergency stop or machine lock is enabled. Machine lock can be disabled if the MLE bit (bit 0 of parameter No. 8001) is set to “1”. However, machine lock for an individual axis is always enabled. 2 In consecutive cutting feed blocks, a new bl
- Page 93815. PMC CONTROL FUNCTION B–63833EN–1/02 15.1.2 PMC Axis Control Expansion Overview This function makes it possible to use the following functions. (1) Cutting fees (sec/block) The time period until the end of the block can be specified. (2) Simultaneous start mode on/off If the simultaneous start mo
- Page 939B–63833EN–1/02 15. PMC CONTROL FUNCTION (2) Simultaneous start mode on/off D Specification If the simultaneous start mode is set on, the commands for multiple paths can be simultaneously started. By using this function together with sec/block described in Item (1), ”Cutting feed,” linear interpolati
- Page 94015. PMC CONTROL FUNCTION B–63833EN–1/02 The simultaneous start mode can be set on or off in any command group of any path. If a block for setting on the simultaneous start mode is specified while the simultaneous start mode is set on, the block becomes invalid. For the other paths, normal commands c
- Page 941B–63833EN–1/02 15. PMC CONTROL FUNCTION NOTE 1 Specify a cutting feed command by the automatic operation on the CNC side in the incremental mode. 2 If a signal is switched from 1 to 0 during superimposed operation, alarm 130 will be raised. When setting a signal to 0, do so after checking that the a
- Page 94215. PMC CONTROL FUNCTION B–63833EN–1/02 Parameter #7 #6 #5 #4 #3 #2 #1 #0 8006 ESI [Data type] Bit ESI Superimposed control of the PMC axis control extension function is: 0 : Extended. 1 : Not extended. To use the superimposed command, set this parameter to 1. Alarm and message Number Message Descri
- Page 943B–63833EN–1/02 15. PMC CONTROL FUNCTION 15.2 EXTERNAL DATA INPUT General The following signals are used to send data from the PMC to the CNC. Signal name Signal code Data signal for external data input (input) ED0 to ED15 Address signal for external data input (input) EA0 to EA6 Read signal for exte
- Page 94415. PMC CONTROL FUNCTION B–63833EN–1/02 Data types accessed by external data input E ED15 to ED0 SEEE EEEE No. Item TAAA AAAA 15141312 1110 9 8 7 6 5 4 3 2 1 0 B65 4 321 0 External program number Program number(BCD4 digits) 1 1 0 0 0 ×××× search 0 to 9 0 to 9 0 to 9 0 to 9 External tool compensa- Of
- Page 945B–63833EN–1/02 15. PMC CONTROL FUNCTION 1) External Program A program number (1 to 9999) is specified from an extended source and Number Search is selected in the CNC memory. For machines that can load several kinds of workpieces, this function can automatically select the program to be executed cor
- Page 94615. PMC CONTROL FUNCTION B–63833EN–1/02 Read signal for external data input (ESTB) Read completion signal for external data input (EREND) If RST becomes 1 even momentarily in this period Reset signal (RST) Search completion signal for external ESEND does not become high. data input (ESEND) Search ca
- Page 947B–63833EN–1/02 15. PMC CONTROL FUNCTION 2nd command Read signal for external data input (ESTB) Search command is kept. Read completion signal for external data input (EREND) Search completion signal for external data input (ESEND) Cycle start lamp signal (ST) Cycle start signal (STL) Automatic opera
- Page 94815. PMC CONTROL FUNCTION B–63833EN–1/02 Data specification for external tool compensation (For M series) Address Data E E E E E E E E E E E E E E E E E E E E E E E A A A A A A A D D D D D D D D D D D D D D D D 6 5 4 3 2 1 0 15 14 13 12 11 10 9 8 7 6 5 4 3 2 1 0 0 0 1 ABS 0 0 0 s MSB LSB / i INC g Of
- Page 949B–63833EN–1/02 15. PMC CONTROL FUNCTION 3) External workpiece The external workpiece coordinate system shift adjusts the workpiece coordinate system coordinate system depending on the shift amount set via the PMC. Each shift axis (parameter No. 1220) has this shift amount, and it is added to all the
- Page 95015. PMC CONTROL FUNCTION B–63833EN–1/02 NOTE Two characters are sent at a time (see ISO code given in the table below). ED15 to ED8 . . . . . . Character code in 1st character. ED7 to ED0 . . . . . . . Character code in 2nd character. When sending only one character, fill the second slot with a code
- Page 951B–63833EN–1/02 15. PMC CONTROL FUNCTION 6) Substituting No. of Substitution is possible for the No. of parts required and the No. of parts parts required and No. machined. of parts, machined Data specification for No. of parts required and No. of parts machined. Address Data E E E E E E E E E A A A
- Page 95215. PMC CONTROL FUNCTION B–63833EN–1/02 Read completion signal for external data input EREND
- Page 953B–63833EN–1/02 15. PMC CONTROL FUNCTION Signal address #7 #6 #5 #4 #3 #2 #1 #0 G000 ED7 ED6 ED5 ED4 ED3 ED2 ED1 ED0 G001 ED15 ED14 ED13 ED12 ED11 ED10 ED9 ED8 G002 ESTB EA6 EA5 EA4 EA3 EA2 EA1 EA0 #7 #6 #5 #4 #3 #2 #1 #0 F060 ESCAN ESEND EREND Parameter #7 #6 #5 #4 #3 #2 #1 #0 3202 PSR [Data type] B
- Page 95415. PMC CONTROL FUNCTION B–63833EN–1/02 Number Message Description 132 ALARM NUMBER NOT No alarm No. concerned exists in exter- FOUND nal alarm message clear. Check the PMC ladder diagram. 133 ILLEGAL DATA IN EXT. Small section data is erroneous in ex- ALARM MSG ternal alarm message or external oper
- Page 955B–63833EN–1/02 15. PMC CONTROL FUNCTION 15.3 EXTERNAL WORKPIECE NUMBER SEARCH 15.3.1 External Workpiece Number Search General When several part programs are stored in program storage memory, a program can be searched with the workpiece number search signals PN1 to PN16 from the machine side. When th
- Page 95615. PMC CONTROL FUNCTION B–63833EN–1/02 Workpiece number search signal Workpiece PN16 PN8 PN4 PN2 PN1 number 0 1 1 0 0 12 0 1 1 0 1 13 0 1 1 1 0 14 0 1 1 1 1 15 1 0 0 0 0 16 1 0 0 0 1 17 1 0 0 1 0 18 1 0 0 1 1 19 1 0 1 0 0 20 1 0 1 0 1 21 1 0 1 1 0 22 1 0 1 1 1 23 1 1 0 0 0 24 1 1 0 0 1 25 1 1 0 1 0
- Page 957B–63833EN–1/02 15. PMC CONTROL FUNCTION Alarm and Message Number Message Description 059 PROGRAM NUMBER During an external program number NOT FOUND search or external workpiece number search, a specified program number was not found. Otherwise, a program specified for searching is being edited in ba
- Page 95815. PMC CONTROL FUNCTION B–63833EN–1/02 15.3.2 Expanded External Workpiece Number Search General Using the EPN0 to EPN13 (expanded external workpiece number search) signals enables a search for program numbers O0001 to O9999. Unlike the workpiece number search signal, which triggers an automatic ope
- Page 959B–63833EN–1/02 15. PMC CONTROL FUNCTION Signal address #7 #6 #5 #4 #3 #2 #1 #0 G024 EPN7 EPN6 EPN5 EPN4 EPN3 EPN2 EPN1 EPN0 #7 #6 #5 #4 #3 #2 #1 #0 G025 EPNS EPN13 EPN12 EPN11 EPN10 EPN9 EPN8 Parameter #7 #6 #5 #4 #3 #2 #1 #0 3006 EPS EPN EPN Workpiece number search signals are assigned to: 0 : PN1,
- Page 96015. PMC CONTROL FUNCTION B–63833EN–1/02 15.4 SPINDLE OUTPUT CONTROL BY THE PMC General The PMC can control the speed and polarity of each spindle motor, connected by the spindle serial output/spindle analog output function. The first to third spindles each have their own individual interfaces. By us
- Page 961B–63833EN–1/02 15. PMC CONTROL FUNCTION Spindle speed Spindle motor speed data = 4095 Maximum spindle speed By using this expression, the spindle motor speed data can easily be obtained. Specifying the output The PMC can specify the spindle motor output polarity when the polarity for the spindle fol
- Page 96215. PMC CONTROL FUNCTION B–63833EN–1/02 To specify a rotation command for the second spindle, enter the gears to be used for the second spindle in GR1 and GR2 and obtain the data of the twelve code signals corresponding to the S value. Specify the data as the speed output command for the second spin
- Page 963B–63833EN–1/02 15. PMC CONTROL FUNCTION D Details of the signals D Signal used to select the spindle motor speed command SINDx → The above signal is used to select whether the spindle motor speed is controlled by the CNC or PMC. 1: The spindle motor is controlled according to speed commands (R01Ix t
- Page 96415. PMC CONTROL FUNCTION B–63833EN–1/02 Twelve code signals corresponding to the S value R01O to R12O
- Page 965B–63833EN–1/02 15. PMC CONTROL FUNCTION NOTE For the T series, this parameter is enabled when bit 4 (EVS) of parameter No. 3705 is set to 1. For the M series, SF is not output: (1) For an S command used to specify maximum spindle speed clamping (G92S–––;) in constant surface speed control mode (2) W
- Page 96615. PMC CONTROL FUNCTION B–63833EN–1/02 Note NOTE 1 If the spindle fails to move after the PMC issues the spindle motor speed command, check the following: Type A is selected (the MSI bit, bit 2 of parameter No. 3709, is set to 0) when the multispindle control function is used. → The second and thir
- Page 967B–63833EN–1/02 15. PMC CONTROL FUNCTION 15.5 EXTERNAL KEY INPUT General MDI key codes can be sent from the PMC to CNC by means of interface signals. This allows the CNC to be controlled in the same way as when the operator performs MDI key operation. Control is realized by exchanging the following i
- Page 96815. PMC CONTROL FUNCTION B–63833EN–1/02 NOTE Read processing is controlled by exclusive–ORing (XOR) the key code read signal (EKSET) with the read completion signal (EKENB). When the EKSET and EKENB signals differ in their logic, the CNC reads the input key code. Once reading has been completed, the
- Page 969B–63833EN–1/02 15. PMC CONTROL FUNCTION Program screen display mode signal PRGDPL
- Page 97015. PMC CONTROL FUNCTION B–63833EN–1/02 NOTE GRAPH 1 For the small keyboard, 0EDH is assigned to CUSTOM . For the standard keyboard, 0EDH is assigned to GRAPH . 0EEH is assigned to CUSTOM . 2 Handling of the soft keys [F0] to [F9], [FR], and [FL] in the key code table are the key codes for the soft
- Page 971B–63833EN–1/02 15. PMC CONTROL FUNCTION MDI Key Code Table(00H–7FH) 0 1 2 3 4 5 6 7 0 Space 0 @ P 1 1 A Q 2 2 B R 3 # 3 C S 4 4 D T 5 5 E U 6 & 6 F V 7 7 G W 8 ( 8 H X 9 ) 9 I Y A ; * J Z (EOB) B + K [ C , L D – = M ] E . N F / ? O 953
- Page 97215. PMC CONTROL FUNCTION B–63833EN–1/02 MDI Key Code Table(80H–0FFH) 8 9 A B C D E F 0 RESET [F0] (Note2) 1 [F1] (Note2) 2 [F2] (Note2) 3 [F3] (Note2) 4 INSERT [F4] (Note2) 5 DELETE [F5] (Note2) [F6] 6 CAN ALTER (Note2) 7 [F7] (Note2) 8 Cursor INPUT POS [F8] → (Note2) 9 Cursor PROG [F9] ← (Note2) OF
- Page 973B–63833EN–1/02 15. PMC CONTROL FUNCTION 15.6 DIRECT OPERATION BY PMC OR OPEN CNC 15.6.1 DNC Operation by the PMC or OPEN CNC (PC with HSSB Connection) General Activating memory operation in memory operation mode (MEM) with the direct operation select signal set to 1 enables machining (direct operati
- Page 97416. INTERFACE WITH THE POWER MATE CNC B–63833EN–1/02 16 INTERFACE WITH THE POWER MATE CNC 956
- Page 975B–63833EN–1/02 16. INTERFACE WITH THE POWER MATE CNC 16.1 FANUC SERVO MOTOR b SERIES I/O LINK OPTION MANUAL HANDLE INTERFACE (PERIPHERAL DEVICE CONTROL) General This function enables manual handle feed of the b servo unit with the manual pulse generator on the host side. A pulse signal generated by
- Page 97616. INTERFACE WITH THE POWER MATE CNC B–63833EN–1/02 Signal (on the FS0i/0i Mate side) Manual handle feed generator selection signals IOLBH2, IOLBH3
- Page 977B–63833EN–1/02 16. INTERFACE WITH THE POWER MATE CNC Signal (on the b servo unit side) Mode selection signals MD1, MD2, MD4
- Page 97816. INTERFACE WITH THE POWER MATE CNC B–63833EN–1/02 NOTE 1 The signals are valid when bit 5 (MP) of parameter No. 5 for the b servo unit is set to 1. 2 The signals are valid only in the manual handle mode. 3 The signals are used also as rapid traverse override signals. In the manual handle mode, th
- Page 979B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 17 PCMCIA ETHERNET FUNCTION This chapter describes the specifications of the PCMCIA Ethernet function for Series 0i–B. 961
- Page 98017. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 17.1 The PCMCIA Ethernet function for CNC can be used the PCMCIA Ethernet card. PCMCIA ETHERNET The PCMCIA Ethernet card is inserted into the memory card slot of the CNC unit for temporary communication. NOTE 1 Use the PCMCIA Ethernet card for temporary co
- Page 981B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 17.2 This section describes the setting of the parameters for the PCMCIA Ethernet function for the Series 0i–B. SETTING THE PCMCIA ETHERNET FUNCTION 17.2.1 On the Ethernet parameter setting screen, set the parameters. Ethernet Parameter Setting Screen Disp
- Page 98217. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 PAGE 7 Switch the screen display with the page keys PAGE . If data is already registered, the data is displayed. 964
- Page 983B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION Display item and setting items Display item The item related to the PCMCIA Ethernet function is displayed. Item Description MAC ADDRESS PCMCIA Ethernet card MAC address Setting items Set the TCP/IP–related items of the PCMCIA Ethernet. Item Description IP
- Page 98417. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 17.2.2 This subsection describes the method of parameter input when the Communication PCMCIA Ethernet function for the Series 0i–B is used. Parameter Input Method Basic method of data input The basic method of data input is described below, using an exampl
- Page 985B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION (b) Type 192.168.1.2 with the MDI keys. (c) Press the [INPUT] soft key or the function key INPUT to enter the data. This stores the parameter in the nonvolatile memory of the CNC. NOTE Turn on the power again so that you should make a changed parameter eff
- Page 98617. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 17.3 If an error occurs with the PCMCIA Ethernet function, the error message screen for the PCMCIA Ethernet function displays an error message. PCMCIA ETHERNET ERROR MESSAGE SCREEN Display Procedure 1 Press the function key MESSAGE . 2 Press the continuous
- Page 987B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION PAGE 5 Switch the screen display with the page keys PAGE . [Tip] The latest error message is displayed at the top of the screen. To the right of an error message, the date and time data of the occurrence of the error is displayed. The format of date and ti
- Page 98817. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 17.4 With the PCMCIA Ethernet function, a dedicated maintenance screen is available. PCMCIA ETHERNET The maintenance screen enables operations to be checked when the MAINTENANCE PCMCIA Ethernet function operates abnormally. SCREEN Display Procedure 1 Press
- Page 989B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 6 The screen below is used to check the state of the communication cable and whether a communication destination exists. Enter the IP address of a communication destination through MDI keys, then press the [PING] soft key. Communication is performed three
- Page 99017. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 7 The screen below is used to check the communication state of the PCMCIA Ethernet function and the error detection count of the Ethernet controller. The screen consists of two pages: one page for an error detection count for transmission, and the other fo
- Page 991B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 8 The screen below is used to check the state of each task of the PCMCIA Ethernet function. Symbol Meaning MASTER CTRL E Ethernet controller being initialized D Data being processed(NOTE) W Waiting for data processing(NOTE) P Waiting for parameter setting
- Page 99217. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 Symbol Meaning PMC X Waiting for completion of Ethernet controller initialization D Data being processed(NOTE) W Waiting for data processing(NOTE) NOTE A state change occurs between the states ”Data being processed” and ”Waiting for data processing” even w
- Page 993B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 17.5 This section describes troubleshooting and check items associated with the PCMCIA Ethernet function. TROUBLESHOOTING 17.5.1 1) Is an STP cable used for connection between the hub and PCMCIA Check Items Related to Ethernet? Connection 2) Is the STP cab
- Page 99417. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 17.5.3 This subsection describes how to check the state of communication Checking between the CNC and personal computer. Communication Checking the connection status and settings If communication with the CNC is not satisfactory or fails from time to time,
- Page 995B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 2) When no response is received (error) If no response is received from the CNC, the cause is considered to be a hardware connection error and/or software setting error. Check the hardware connection and software settings. Checking the influence of noise T
- Page 99617. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 3) Count the number of lost packets (to which no response is returned). If lost packets occur in this state, there is probably an influence of noise from peripheral equipment. Action: Locate the noise source and recheck the cabling to eliminate the influen
- Page 997B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 17.6 If an error occurs with the embedded Ethernet function, the log screen of the PCMCIA Ethernet function displays an error message. ERROR MESSAGES This section describes error messages displayed on the log screen. The major error messages are described
- Page 99817. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 17.6.2 TCP PORT NUMBER(???) IS INVALID EMB_ETH The setting (???) of the TCP port number is incorrect. Correct the TCP port number. FOCAS1/ETHER LOG Illegal Broadcast IP ADDRESS Screen The broadcast address for UDP transmission is incorrect. Correct the sub
- Page 999B–63833EN–1/02 17. PCMCIA ETHERNET FUNCTION 17.7 This section briefly describes Ethernet–related terms. The descriptions below provide minimum information only. For further GLOSSARY FOR information, refer to relevant publications available on the market. ETHERNET TCP/IP For Ethernet–based communicat
- Page 100017. PCMCIA ETHERNET FUNCTION B–63833EN–1/02 IP addresses are internationally managed systematically. This means that before an IP address can be used, the IP address must be obtained formally from the international organization. If the network used by a user is a local network closed within the user
- Page 1001APPENDI
- Page 1002
- Page 1003B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC A INTERFACE BETWEEN CNC AND PMC 985
- Page 1004A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 A.1 LIST OF ADDRESSES A.1.1 The figure below illustrates the addresses of interface signals between the Series 0i/0i Mate CNC and PMC. Address List CNC G000 ∼ PMC X000 ∼ MT F000 ∼ Y000 ∼ Following shows table of addresses: In an item where both T serie
- Page 1005B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC MT → PMC Address Bit number #7 #6 #5 #4 #3 #2 #1 #0 X000 X001 X002 X003 SKIP ESKIP –MIT2 +MIT2 –MIT1 +MIT1 ZAE XAE (T series) X004 SKIP6 SKIP5 SKIP4 SKIP3 SKIP2 SKIP8 SKIP7 SKIP ESKIP ZAE YAE XAE (M series) X005 X006 X007 X008 *ESP X009 *DEC4 *DEC3 *DE
- Page 1006A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 D T series/M series PMC → CNC Address Bit number #7 #6 #5 #4 #3 #2 #1 #0 G000 ED7 ED6 ED5 ED4 ED3 ED2 ED1 ED0 G001 ED15 ED14 ED13 ED12 ED11 ED10 ED9 ED8 G002 ESTB EA6 EA5 EA4 EA3 EA2 EA1 EA0 G003 G004 MFIN3 MFIN2 FIN G005 BFIN AFL BFIN TFIN SFIN EFIN M
- Page 1007B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 G025 EPNS EPN13 EPN12 EPN11 EPN10 EPN9 EPN8 G026 G027 CON *SSTP3 *SSTP2 *SSTP1 SWS3 SWS2 SWS1 G028 PC2SLC SPSTP *SCPF *SUCPF GR2 GR1 G029 *SSTP SOR SAR GR21 G030 SOV7 SOV6 SOV5 SOV4 SOV3 SOV2 SOV1 SOV0 G031 G032 R08I R07I R06I R
- Page 1008A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G050 *TLV9 *TLV8 G051 G052 G053 CDZ SMZ UINT TMRON G054 UI007 UI006 UI005 UI004 UI003 UI002 UI001 UI000 G055 UI015 UI014 UI013 UI012 UI011 UI010 UI009 UI008 G056 G057 G058 EXWT EXSTP EXRD MINP G059 G060 *TSB G061 RGTSP2 RGTSP1 R
- Page 1009B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 G075 RCHB RSLB INTGB SOCNB MCFNB SPSLB *ESPB ARSTB G076 RCHHGB MFNHGB INCMDB OVRB DEFMDB NRROB ROTAB INDXB G077 DSCNB MPOFB SLVB MORCMB G078 SHA07 SHA06 SHA05 SHA04 SHA03 SHA02 SHA01 SHA00 G079 SHA11 SHA10 SHA09 SHA08 G080 SHB07
- Page 1010A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G100 +J4 +J3 +J2 +J1 G101 G102 –J4 –J3 –J2 –J1 G103 G104 +EXL4 +EXL3 +EXL2 +EXL1 G105 –EXL4 –EXL3 –EXL2 –EXL1 G106 MI4 MI3 MI2 MI1 G107 G108 MLK4 MLK3 MLK2 MLK1 G109 G110 +LM4 +LM3 +LM2 +LM1 G111 G112 –LM4 –LM3 –LM2 –LM1 G113 G1
- Page 1011B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 G124 G125 IUDD4 IUDD3 IUDD2 IUDD1 G126 SVF4 SVF3 SVF2 SVF1 G127 G128 G129 G130 *IT4 *IT3 *IT2 *IT1 G131 G132 +MIT4 +MIT3 +MIT2 +MIT1 G133 G134 –MIT4 –MIT3 –MIT2 –MIT1 G135 G136 EAX4 EAX3 EAX2 EAX1 G137 G138 SYNC4 SYNC3 SYNC2 SYN
- Page 1012A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G149 EID31A EID30A EID29A EID28A EID27A EID26A EID25A EID24A G150 DRNE RTE OVCE ROV2E ROV1E G151 *FV7E *FV6E *FV5E *FV4E *FV3E *FV2E *FV1E *FV0E G152 G153 G154 EBUFB ECLRB ESTPB ESOFB ESBKB EMBUFB ELCKZB EFINB G155 EMSBKB EC6B E
- Page 1013B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 G174 G175 G176 G177 G178 EBUFD ECLRD ESTPD ESOFD ESBKD EMBUFD ELCKZD EFIND G179 EMSBKD EC6D EC5D EC4D EC3D EC2D EC1D EC0D G180 EIF7D EIF6D EIF5D EIF4D EIF3D EIF2D EIF1D EIF0D G181 EIF15D EIF14D EIF13D EIF12D EIF11D EIF10D EIF9D
- Page 1014A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G199 G200 EASIP4 EASIP3 EASIP2 EASIP1 G201 G202 G203 G204 G205 G206 G207 G208 G209 G210 G211 G212 G213 G214 G215 G216 G217 G218 G219 G220 G221 G222 G223 996
- Page 1015B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 G224 G225 G226 G227 G228 G229 G230 G231 G232 G233 G234 G235 G236 G237 G238 G239 G240 G241 G242 G243 G244 G245 G246 G247 G248 997
- Page 1016A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G249 G250 G251 G252 G253 G254 G255 G256 G257 G258 G259 G260 G261 G262 G263 G264 G265 G266 G267 G268 G269 G270 G271 G272 G273 998
- Page 1017B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 G274 G275 G276 G277 G278 G279 G280 G281 G282 G283 G284 G285 G286 G287 G288 G289 G290 G291 G292 G293 G294 G295 G296 G297 G298 999
- Page 1018A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 G299 G300 G301 G302 G303 G304 G305 G306 G307 G308 G309 G310 G311 1000
- Page 1019B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC CNC → PMC Address Bit number #7 #6 #5 #4 #3 #2 #1 #0 F000 OP SA STL SPL RWD F001 MA TAP ENB DEN BAL RST AL F002 MDRN CUT SRNMV THRD CSS RPDO INCH F003 MTCHIN MEDT MMEM MRMT MMDI MJ MH MINC F004 MREF MAFL MSBK MABSM MMLK MBDT1 F005 MBDT9 MBDT8 MBDT7 MBD
- Page 1020A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F025 S31 S30 S29 S28 S27 S26 S25 S24 F026 T07 T06 T05 T04 T03 T02 T01 T00 F027 T15 T14 T13 T12 T11 T10 T09 T08 F028 T23 T22 T21 T20 T19 T18 T17 T16 F029 T31 T30 T29 T28 T27 T26 T25 T24 F030 B07 B06 B05 B04 B03 B02 B01 B00 F031 B
- Page 1021B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 F050 MORA2B MORA1B PORA2B SLVSB RCFNB RCHPB CFINB CHPB F051 EXOFB INCSTB PC1DTB F052 F053 EKENB BGEACT RPALM RPBSY PRGDPL INHKY F054 UO007 UO006 UO005 UO004 UO003 UO002 UO001 UO000 F055 UO015 UO014 UO013 UO012 UO011 UO010 UO009
- Page 1022A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F075 SPO KEYO DRNO MLKO SBKO BDTO F076 ROV2O ROV1O RTAP MP2O MP1O F077 RTO HS1DO HS1CO HS1BO HS1AO F078 *FV7O *FV6O *FV5O *FV4O *FV3O *FV2O *FV1O *FV0O F079 *JV7O *JV6O *JV5O *JV4O *JV3O *JV2O *JV1O *JV0O F080 *JV15O *JV14O *JV1
- Page 1023B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 F100 ZP44 ZP43 ZP42 ZP41 F101 F102 MV4 MV3 MV2 MV1 F103 F104 INP4 INP3 INP2 INP1 F105 F106 MVD4 MVD3 MVD2 MVD1 F107 F108 MMI4 MMI3 MMI2 MMI1 F109 F110 F111 F112 EADEN4 EADEN3 EADEN2 EADEN1 F113 F114 TRQL4 TRQL3 TRQL2 TRQL1 F115
- Page 1024A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F125 F126 –OT4 –OT3 –OT2 –OT1 F127 F128 F129 *EAXSL EOV0 F130 EBSYA EOTNA EOTPA EGENA EDENA EIALA ECKZA EINPA F131 EABUFA EMFA F132 EM28A EM24A EM22A EM21A EM18A EM14A EM12A EM11A F133 EBSYB EOTNB EOTPB EGENB EDENB EIALB ECKZB E
- Page 1025B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 F150 F151 EM48D EM44D EM42D EM41D EM38D EM34D EM32D EM31D F152 F153 F154 F155 F156 F157 F158 F159 F160 F161 F162 F163 F164 F165 F166 F167 F168 F169 F170 F171 F172 PBATL PBATZ F173 F174 1007
- Page 1026A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F175 F176 F177 EDGN EPARM EVAR EPRG EWTIO ESTPIO ERDIO IOLNK F178 SRLNO3 SRLNO2 SRLNO1 SRLNO0 F179 F180 CLRCH4 CLRCH3 CLRCH2 CLRCH1 F181 F182 EACNT4 EACNT3 EACNT2 EACNT1 F183 F184 F185 F186 F187 F188 F189 F190 F191 F192 F193 F19
- Page 1027B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 F200 F201 F202 F203 F204 F205 F206 F207 F208 F209 F210 F211 F212 F213 F214 F215 F216 F217 F218 F219 F220 F221 F222 F223 F224 1009
- Page 1028A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F225 F226 F227 F228 F229 F230 F231 F232 F233 F234 F235 F236 F237 F238 F239 F240 F241 F242 F243 F244 F245 F246 F247 F248 F249 1010
- Page 1029B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 F250 F251 F252 F253 F254 F255 F256 F257 F258 F259 F260 F261 F262 F263 F264 F265 F266 F267 F268 F269 F270 F271 F272 F273 F274 1011
- Page 1030A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 #7 #6 #5 #4 #3 #2 #1 #0 F275 F276 F277 F278 F279 F280 F281 F282 F283 F284 F285 F286 F287 F288 F289 F290 F291 F292 F293 F294 F295 F296 F297 F298 F299 1012
- Page 1031B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC #7 #6 #5 #4 #3 #2 #1 #0 F300 F301 F302 F303 F304 F305 F306 F307 F308 F309 F310 F311 F312 F313 F314 F315 1013
- Page 1032A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 A.2 SIGNAL SUMMARY A.2.1 Signal Summary f : Available – : Unavailable (In Order of Functions) T M Function Signal name Symbol Address Section series series Power Mate background operation BGEN G092#4 f f 13.5 signal Power Mate read/write alarm signal B
- Page 1033B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series Abnormal load detection ignore signal IUDD1 to IUDD4 G125 f f Servo axis abnormal load detected ABTQSV F090#0 f f signal Abnormal load detection First–spindle abnormal load detected 2.9 ABTS
- Page 1034A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series Data signals for external data input ED0 to ED15 G000, G001 f f Address signals for external data input EA0 to EA6 G002#0 to #6 f f Read signal for external data input ESTB G002#7 f f Read c
- Page 1035B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series XAE X004#0 f f Automatic tool length YAE X004#1 — f measurement (M Measuring position reached signals 14.2 series)/automatic ZAE X004#2 — f tool offset (T series) ZAE X004#1 f — Tool offset
- Page 1036A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series Cs contour control change signal CON G027#7 f f Cs contour control Cs contour control change completion 9.8 FSCSL F044#1 f f signal Outputting the Axis moving signals MV1 to MV4 F102 f f mov
- Page 1037B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series Soft start/stop cancel signals SOCNA G071#4 f f (serial spindle) SOCNB G075#4 f f INTGA G071#5 f f Speed integral signals (serial spindle) INTGB G075#5 f f Output switch request signals RSLA
- Page 1038A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series SARA F045#3 f f Speed arrival signals (serial spindle) SARB F049#3 f f LDT1A F045#4 f f Load detection signals 1 (serial spindle) LDT1B F049#4 f f LDT2A F045#5 f f Load detection signals 2 (
- Page 1039B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series Gear selection signals (output) GR1O, GR2O, GR3O F034#0 to #2 — f Spindle speed Gear selection signals (input) GR1, GR2 G028#1, #2 f f control 9.3 F036#0 to S 12–bit code signals R01O to R12
- Page 1040A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series SKIP X004#7 f f Skip function Skip signals 14.3.1 SKIPP G006#6 f — Start lock signal STLK G007#1 f — Interlock signal *IT G008#0 f f Interlock signal for each axis *IT1 to *IT4 G130 f f Manu
- Page 1041B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series Software operator’s panel signal HS1CO F077#2 f f (HS1C) Software operator’s panel signal HS1DO F077#3 f f (HS1D) Software operator’s panel signal MP1O F076#0 f f (MP1) Software operator’s p
- Page 1042A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series Torque limit skip Torque limit reached signals TRQL1 to TRQL8 F114 f — 14.3.4 (T series) Measurement direct Spindle measurement select signal S2TLS G040#5 f — input of tool offset Spindle 1
- Page 1043B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series ESTPA G142#5 f f Axis control temporary stop signals ESTPB G154#5 f f (PMC axis control) ESTPC G166#5 f f ESTPD G178#5 f f ESBKA G142#3 f f ESBKB G154#3 f f Block stop signals (PMC axis cont
- Page 1044A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series EINPA F130#0 f f EINPB F133#0 f f In–position signals (PMC axis control) EINPC F136#0 f f EINPD F139#0 f f ECKZA F130#1 f f Following zero checking signals (PMC ECKZB F133#1 f f axis control
- Page 1045B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series Distribution completion signals (PMC EADEN1 to EADEN4 F112 f f axis control) EABUFA F131#1 f f PMC axis control EABUFB F134#1 f f 15.1 Buffer full signals (PMC axis control) EABUFC F137#1 f
- Page 1046A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Function Signal name Symbol Address Section series series DM00 F009#7 f f DM01 F009#6 f f Decode M signals DM02 F009#5 f f DM30 F009#4 f f Spindle function code signals S00 to S31 F022 to F025 f f Spindle function strobe signal SF F007#2 f f Miscel
- Page 1047B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Function Signal name Symbol Address Section series series Automatic operation selection check MMEM F003#5 f f signal Memory edit selection check signal MEDT F003#6 f f Manual handle feed selection check Mode selection MH F003#1 f f 2.6 signal Incre
- Page 1048A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 A.2.2 List of Signals f : Available – : Unavailable (In Order of Symbols) T M Referen Group Symbol Signal name Address series series ce item *+ED1 to *+ED4 External deceleration signal G118 f f 7.1.8 *+L1 to *+L4 Overtravel signal G114 f f 2.3.1 *-ED1
- Page 1049B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item *TSB Tailstock barrier select signal G060#7 f – 2.3.4 Axis direction dependent stored stroke limit switch +EXL1 to +EXL4 G104 f f 2.3.2 signal +J1 to +J4 Feed axis and direction selecti
- Page 1050A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item BGEACT Background busy signal F053#4 f f 13.5, 13.3 BGEN Power Mate background busy signal G092#4 f f B BGIALM Power Mate read/write alarm signal G092#3 f f 13.5 BGION Power Mate read/w
- Page 1051B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item EACNT1 to EACNT4 Controlling signal (PMC axis control) F182 f f EADEN1 to EADEN4 Distribution completion signal(PMC axis control) F112 f f 15.1 EAX1 to EAX4 Control axis select signal (
- Page 1052A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item EGENA F130#4 f f EGENB F133#4 f f Axis moving signal (PMC axis control) EGENC F136#4 f f EGEND F139#4 f f EIALA F130#2 f f EIALB F133#2 f f Alarm signal (PMC axis control) EIALC F136#2
- Page 1053B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item EMSBKA G143#7 f f EMSBKB Block stop disable signal G155#7 f f 15.1 EMSBKC (PMC axis control) G167#7 f f EMSBKD G179#7 f f ENB F001#4 f f 9.3 ENB2 Spindle enable signal F038#2 f – 9.9 EN
- Page 1054A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item ESTPA G142#5 f f ESTPB Axis control temporary stop signal (PMC axis G154#5 f f 15.1 ESTPC control) G166#5 f f ESTPD G178#5 f f ESTPIO Slave read/write stop signal F177#2 f f EVAR Slave
- Page 1055B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item IGNVRY All-axis VRDY OFF alarm ignore signal G066#0 f f 2.8 IGVRY1 to IGVRY4 Each-axis VRDY OFF alarm ignore signal G192 f f INCH Inch input signal F002#0 f f 11.4 INCMDA Incremental co
- Page 1056A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item MD1O Software operator's panel signal(MD1) F073#0 f f MD2O Software operator's panel signal(MD2) F073#1 f f 12.1.14 MD4O Software operator's panel signal(MD4) F073#2 f f MDRN Dry run ch
- Page 1057B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item MPOFA G073#2 f f Motor power stop signal (serial spindle) MPOFB G077#2 f f 9.2 MRDYA G070#7 f f Machine ready signal (serial spindle) MRDYB G074#7 f f Manual reference position return s
- Page 1058A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item PORA2A Signal for approximate spindle orientation with a F046#5 f f 9.2 PORA2B position coder (serial spindle) F050#5 f f PRC Position record signal G040#6 f – 14.4.1 PRGDPL program scr
- Page 1059B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item RPDO Rapid traversing signal F002#1 f f 2.7 RRW Reset&rewind signal G008#6 f f 5.2 RSLA G071#6 f f Output switch request signal (serial spindle) 9.2 RSLB G075#6 f f RST Reset signal F00
- Page 1060A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item SIND G033#7 f f SIND2 Spindle motor speed command select signal G035#7 f f 15.4 SIND3 G037#7 f f Skip signal X004#7 f f 14.3.1 SKIP Overload torque signal X004#7 – f 11.13 SKIP2 to SKIP
- Page 1061B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Group Symbol Signal name Address series series ce item ST Cycle start lamp signal G007#2 f f 5.1 STL Cycle start signal F000#5 f f STLK Start lock signal G007#1 f – 2.5 STRD Input and run simultaneous mode select signal G058#5 – f 13.6 STWD
- Page 1062A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Group Symbol Signal name Address series series ce item Workpiece coordinate system shift value write WOQSM G039#6 f – mode select signal W 14.4.2 Workpiece coordinate system shift value write WOSET G040#7 f – signal X XAE X004#0 f f Y YAE X
- Page 1063B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC A.2.3 List of Signals f : Available – : Unavailable (In Order of Addresses) T M Referen Address Signal name Symbol series series ce Item X004#0 XAE f f X004#1 YAE – f Measuring position reached signal 14.2 X004#1 ZAE f – X004#2 ZAE – f X004#2,#4 Manual
- Page 1064A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item G007#4 Stroke check 3 release signal RLSOT3 f f 2.3.3 G007#5 Follow-up signal *FLWU f f 1.2.6 G007#6 Stored stroke limit select signal EXLM f f 2.3.2 G007#7 Stroke limit release signal RLSOT
- Page 1065B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Address Signal name Symbol series series ce Item G029#4 Spindle speed arrival signal SAR f f G029#5 Spindle orientation signal SOR f f 9.3 G029#6 Spindle stop signal *SSTP f f G030 Spindle speed override signal SOV0 to SOV7 f f G032#0 to G0
- Page 1066A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item G047#0 to #6 TL01 to TL64 f – Tool group number select signal G047#0 to G048#0 TL01 to TL256 – f G048#5 Tool skip signal TLSKP f f 10.3 G048#6 Individual tool change reset signal TLRSTI – f G
- Page 1067B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Address Signal name Symbol series series ce Item G072#0 Orientation stop position change signal (serial spindle) INDXA f f Rotation direction command while changing the G072#1 ROTAA f f orientation stop position signal (serial spindle) Shor
- Page 1068A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item Main spindle MCC status signal while changing spindles G076#6 MFNHGB f f signal (serial spindle) High–output MCC status signal while a magnetic sensor G076#7 RCHHGB f f (serial spindle) Comma
- Page 1069B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Address Signal name Symbol series series ce Item G142#0 Auxiliary function completion signal (PMC axis control) EFINA f f G142#1 Accumulated zero check signal ELCKZA f f G142#2 Buffering disable signal (PMC axis control) EMBUFA f f G142#3 B
- Page 1070A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item G167#7 Block stop disable signal (PMC axis control) EMSBKC f f G168,G169 Axis control feedrate signal (PMC axis control) EIF0C to EIF15C f f G170 to G173 Axis control data signal (PMC axis co
- Page 1071B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Address Signal name Symbol series series ce Item F003#0 Incremental feed select check signal MINC f f F003#1 Manual handle feed select check signal MH f f 2.6 F003#2 Jog feed select check signal MJ f f F003#3 Manual data input select check
- Page 1072A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item F038#2 ENB2 f f Spindle enable signals 9.9 F038#3 ENB3 f f F040,F041 Actual spindle speed signal AR0 to AR15 f – 9.6 F044#1 Cs contour control switch completion signal FSCSL f f 9.8 F044#2 Sp
- Page 1073B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Address Signal name Symbol series series ce Item F050#2 Output switch signal (serial spindle) RCHPB f f 9.2 F050#3 Output switch completion signal (serial spindle) RCFNB f f F050#4 Slave operation status signal (serial spindle) SLVSB f f Si
- Page 1074A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item F072 Software operator's panelgeneral-purpose switch signal OUT0 to OUT7 f f F073#0 Software operator's panel signal (MD1) MD1O f f F073#1 Software operator's panel signal (MD2) MD2O f f F073
- Page 1075B–63833EN–1/02 A. INTERFACE BETWEEN CNC AND PMC T M Referen Address Signal name Symbol series series ce Item F122#0 High-speed skip status signal HDO0 f f 14.3.2 F124 Stroke limit reached signals +OT1 to +OT4 – f 2.3.2 F126 Stroke limit reached signals –OT1 to –OT4 – f F129#5 Override 0% signal (PMC
- Page 1076A. INTERFACE BETWEEN CNC AND PMC B–63833EN–1/02 T M Referen Address Signal name Symbol series series ce Item F138,F148 Auxiliary function code signal (PMC axis control) EM11C to EM48C f f F139#0 In-position signal (PMC axis control) EINPD f f F139#1 Following zero checking signal (PMC axis control)
- Page 1077B–63833EN–1/02 Index Note Volume 1 : Up to Page 602 / Volume 2 : Page 603 and later ƠNumbersơ Connection among spindle, spindle motor, and position coder, 527 2nd reference position return/3rd, 4th reference position return, Constant surface speed control, 462 200 Controlled axes, 2 Conversational p
- Page 1078INDEX B–63833EN–1/02 Note Volume 1 : Up to Page 602 / Volume 2 : Page 603 and later Expanded external workpiece number search, 940 Input of measured workpiece origin offsets, 871 External data input, 925 Input of offset value measured A (T series), 850 External deceleration, 328 Input of tool offset
- Page 1079B–63833EN–1/02 INDEX Note Volume 1 : Up to Page 602 / Volume 2 : Page 603 and later No. of registered programs, 770 Rapid traverse rate, 305 Normal direction control (M series), 296 Reader/puncher interface, 778 Notes on interface with the PMC, 547 Reference position establishment, 175 Reference pos
- Page 1080INDEX B–63833EN–1/02 Note Volume 1 : Up to Page 602 / Volume 2 : Page 603 and later Spindle serial output/spindle analog output, 425 Tool function, 604 Spindle setting and tuning screen, 717 Tool functions, 603 Spindle speed control, 433 Tool length measurement (M series), 828 Spindle speed fluctuat
- Page 1081Revision Record FANUCĄSeriesĄ0i–MODEL B/0i Mate–MODEL B CONNECTION MANUAL (FUNCTION) (B–63833EN–1) D Deletion Series 0i Mate–MODEL A 02 Aug., 2002 D Addition Series 0i Mate–MODEL B 01 Aug., 2002 Edition Date Contents Edition Date Contents
- Page 1082
- Page 1083TECHNICAL REPORT (MANUAL) No. TMN 03/049E Date : Jun. 13, 2003 General Manager of Software Development Center FANUC Series 0i/0iMate-B I/O LINK MPG allocation function 1. Communicate this report to: Your information only ○ GE Fanuc-A, GE Fanuc-E FANUC Robotics America MILACRON ○ Machine tool builder
- Page 1084FANUC Series 0i/0i Mate - B I/O LINK MPG allocation function Specifications 1.OUTLINE .................................................................................................................. 2 2.DETAILS........................................................................................
- Page 10851. Outline MPG (Manual Pulse Generator) is connected with the control unit in Series 0i -B usually. On the other hand, MPG is connected with the operator’s panel (I/O module for operator’s panel is included) with MPG interface connected with I/O LINK in Series 0i Mate -B. When the operator’s panel (
- Page 10864. Parameter No. #7 #6 #5 #4 #3 #2 #1 #0 7105 HDX Data form: Bit type HDX 0: MPG is automatically allocated in order connected with I/O LINK. 1: MPG in X address set to parameter No.12305-12307 is used. 12305 X signal address for the first MPG 12306 X signal address for the second MPG 12307 X signal
- Page 1087TECHNICAL REPORT NO.TMN 03/ 071E Date : August.19.’03 General Manager of Software Development Center FANUC Series 0i / 0i Mate - B Additional manual for Controlled Axes Detach function 1. Communicate this report to : Your information only ○ GE Fanuc-A, GE Fanuc-E FANUC Robotics CINCINATI MILACRON ○
- Page 10881 Controlled Axes Detach General These signals release the specified control axes from control by the CNC. When attachments are used (such as a detachable rotary table), these signals are selected according to whether the attachments are mounted. The signals can also be used for switching the C axis
- Page 1089Controlled axis detach status signals MDTCH1 – MDTCH4
[Classification] Output signal [Function] These signals notify the PMC that the corresponding axes have been released from control. These signals are provided for each control axis; the affixed number of the signal name shows the control a - Page 1090MCCx When an axis is released from control, control for the MCC signal for the corresponding servo amplifier is 0 : Disabled 1 : Enabled NOTE If the servo motor for an axis is connected to a 2-axis or other multiaxis amplifier, releasing the axis from control causes servo alarm 401 (V ready off) to
- Page 1442. PREPARATIONS FOR OPERATION B–63833EN–1/02 All axes Interlock signal *IT